Silicate powder conveying systems are essential components in industrial processes, particularly for handling and transporting silicate materials such as silica, kaolin, and other mineral powders. These systems are designed to efficiently move bulk powders from one location to another while maintaining product integrity and minimizing material loss. The core of these systems lies in their ability to handle the unique properties of silicate powders, which often include high moisture content, abrasive characteristics, and varying particle sizes. A well-designed silicate powder conveying system not only enhances operational efficiency but also ensures compliance with safety and environmental standards.
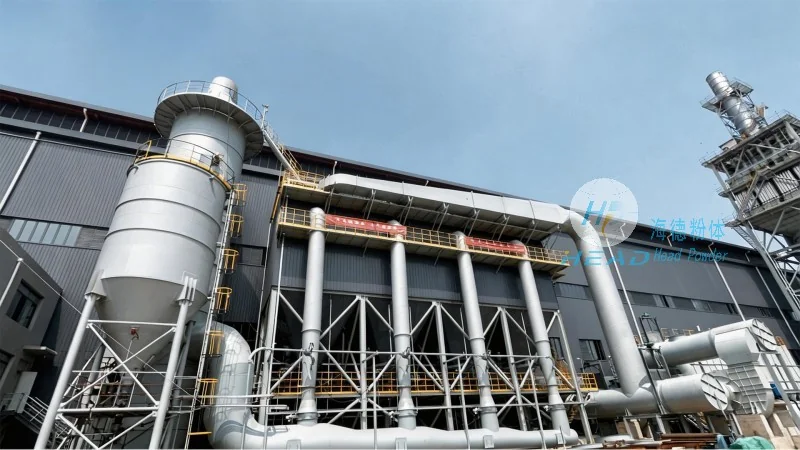
About HeadPowder: A Leading Provider of Conveying Solutions
HeadPowder, operating as Shandong HeadPowder Engineering Co., Ltd., is a reputable company based in China, specializing in the design, manufacturing, and integration of advanced powder handling equipment. With a strong focus on innovation and customer-centric solutions, HeadPowder has established itself as a trusted partner for industries requiring reliable silicate powder conveying systems. The company’s expertise lies in understanding the specific challenges of handling silicate powders, such as dust control, material flow optimization, and system durability. By leveraging years of experience and cutting-edge technology, HeadPowder delivers customized solutions that meet the unique needs of each client, ensuring optimal performance and long-term reliability.
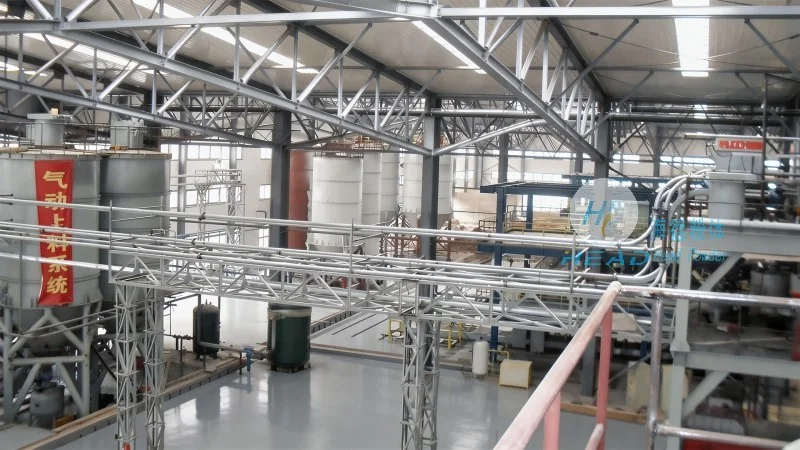
The Design Principles of Silicate Powder Conveying Systems
The design of a silicate powder conveying system is a complex process that involves several key principles to ensure effective and safe operation. One of the primary considerations is the selection of appropriate equipment components, such as screw conveyors, pneumatic conveyors, or bucket elevators, based on the material characteristics and process requirements. For silicate powders, which may be abrasive and prone to caking, materials like stainless steel or specialized alloys are often used for the conveyor components to prevent wear and maintain hygiene. The system design also incorporates features like aeration and vibration to prevent material bridging and ensure smooth flow. Additionally, the integration of dust collection and filtration systems is crucial to maintain air quality and comply with environmental regulations. The control systems, including variable speed drives and sensors, allow for real-time monitoring and adjustment of the conveying process, optimizing performance and reducing energy consumption.
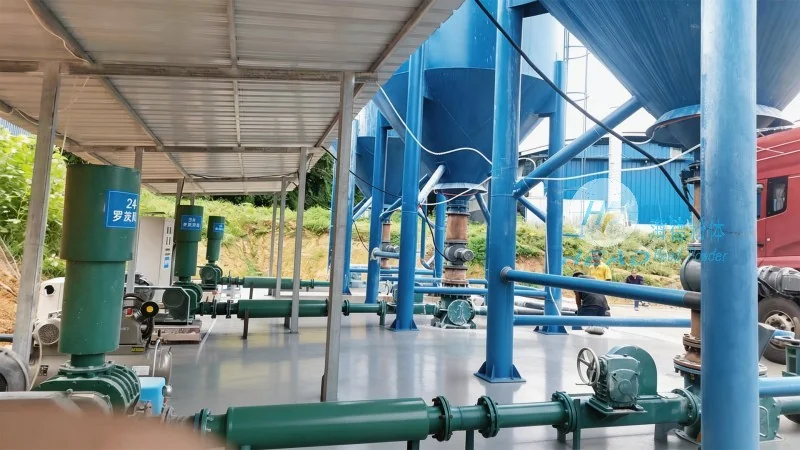
Key Features and Benefits of HeadPowder's Silicate Powder Conveying Systems
HeadPowder’s silicate powder conveying systems are engineered with a range of features that address the specific challenges of handling silicate materials. These systems are designed to handle a wide range of particle sizes and moisture contents, ensuring consistent performance across different applications. The use of high-quality materials and precision manufacturing ensures durability and long service life, reducing maintenance costs and downtime. The systems are also equipped with advanced control technologies that enable automated operation and integration with existing production lines. This automation not only improves efficiency but also enhances safety by minimizing human intervention in potentially hazardous environments. Furthermore, the modular design of the systems allows for easy installation and customization, making them suitable for various industrial settings, from small-scale operations to large-scale manufacturing facilities.
Applications and Industries Served
Silicate powder conveying systems are widely used in industries such as ceramics, glass, pharmaceuticals, and food processing. In the ceramics industry, these systems are essential for transporting raw materials like kaolin and silica to production lines, where they are used to manufacture tiles, pottery, and other ceramic products. In the glass industry, silicate powders are used as raw materials for glass production, and efficient conveying systems ensure a steady supply of high-quality materials. The pharmaceutical and food industries also rely on these systems for handling powders that require strict contamination control and hygiene standards. HeadPowder’s systems are tailored to meet the specific requirements of these industries, providing reliable and efficient solutions that enhance productivity and product quality.
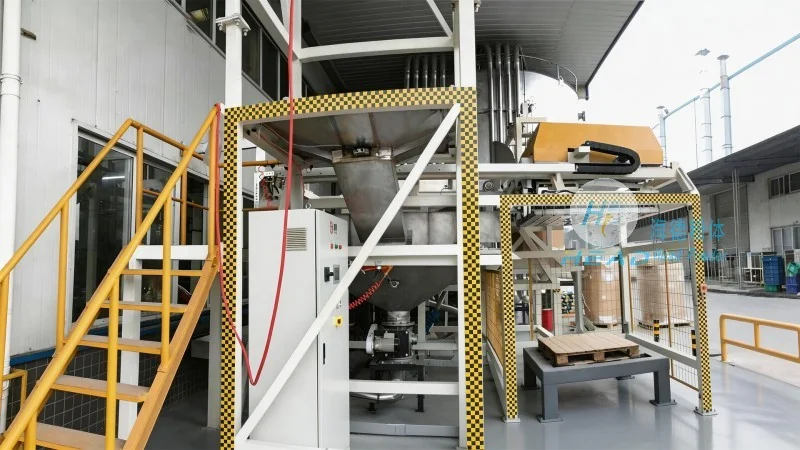
Conclusion and Company Information
HeadPowder, with its headquarters in Shandong, China, continues to be a leader in the development and supply of silicate powder conveying systems. By combining advanced design principles with practical application knowledge, the company delivers solutions that meet the evolving needs of modern industries. The focus on durability, efficiency, and safety makes HeadPowder’s systems a preferred choice for businesses seeking to optimize their powder handling processes. With a commitment to quality and customer satisfaction, HeadPowder remains dedicated to providing innovative and reliable conveying solutions for the global market.




