In the realm of agricultural processing, particularly for cotton seed, efficient material handling is a critical factor in optimizing production efficiency and minimizing operational costs. The pneumatic conveying system for cotton seed materials represents a sophisticated technology that leverages the principles of fluid dynamics to transport bulk solids. This system is engineered to address the unique challenges posed by cotton seed, such as their irregular shape, varying moisture content, and tendency to clump. By utilizing air as the conveying medium, the system ensures a continuous, low-maintenance method of moving cotton seed from storage to processing units. Understanding the underlying principles and typical operational scenarios is essential for industries seeking to enhance their material handling capabilities.
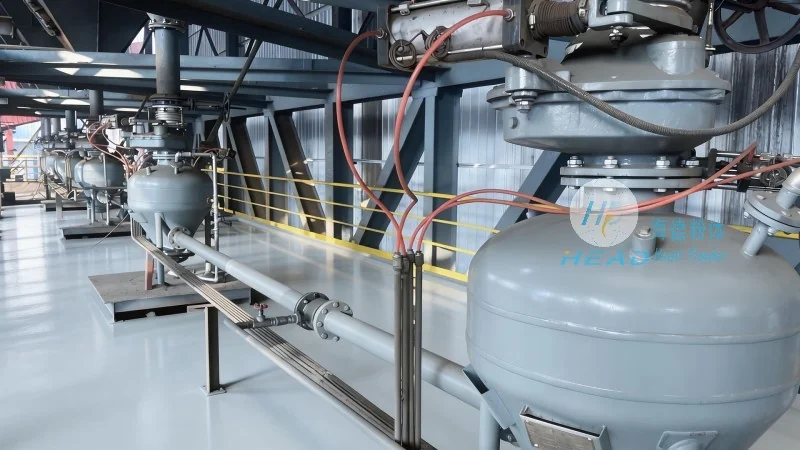
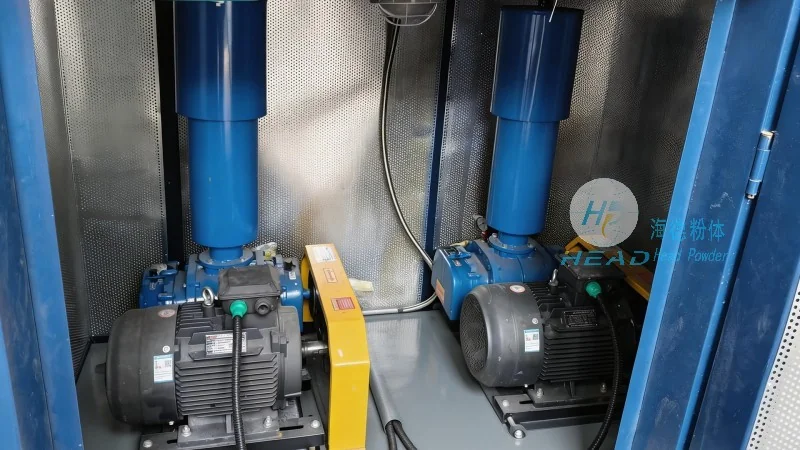
Core Principles of Pneumatic Conveying for Cotton Seed
The fundamental principle of pneumatic conveying involves creating a flow of air within a pipeline that is sufficient to lift and transport solid particles. For cotton seed, this process relies on the concept of air velocity exceeding the material's terminal velocity, which is the speed at which the material falls through the air. The system typically operates under pressure, where an air compressor generates the necessary air pressure to move the seed. Key components of the system include the air compressor, conveying pipes, airlocks, and separation equipment. The air compressor is responsible for generating the pressure, while the conveying pipes transport the seed. Airlocks are used to control the flow of material into the system, preventing backflow. Separation units, such as cyclone separators, are integrated to remove the seed from the air stream and return it to the processing line. The design of the system ensures that the air velocity remains consistent throughout the pipeline, preventing clogging and ensuring smooth operation. Additionally, the system incorporates filtration and cleaning mechanisms to maintain air quality and prevent dust accumulation in the equipment.
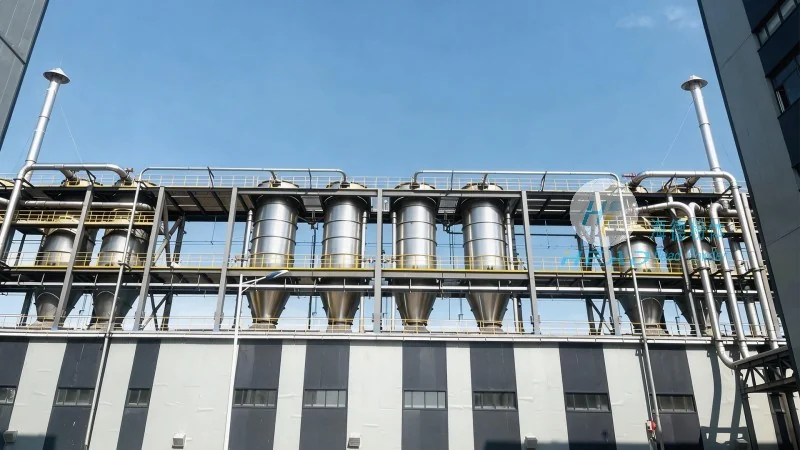
Working Scene Characteristics and Applications
The working scene characteristics of cotton seed pneumatic conveying systems are influenced by the scale of operation, the processing stage, and the specific requirements of the facility. In large-scale cotton seed processing plants, these systems are commonly used for transporting raw cotton seed from storage silos to primary processing equipment, such as hulling machines or oil extraction units. The high capacity of pneumatic conveying systems makes them ideal for continuous production lines, where large volumes of material need to be moved efficiently. In smaller-scale operations, such as on-farm processing or small processing facilities, the system can be adapted to handle smaller batches of cotton seed, providing flexibility in operation. The working environment often involves high humidity and dust, which the system is designed to manage effectively. The system's design minimizes material spillage and dust emission, contributing to a cleaner and safer working environment. Furthermore, the system's adaptability allows it to be integrated with other processing equipment, such as cleaning and sorting machines, to form a comprehensive material handling solution. This integration enhances overall operational efficiency by streamlining the flow of materials through the production process, reducing downtime and improving throughput.
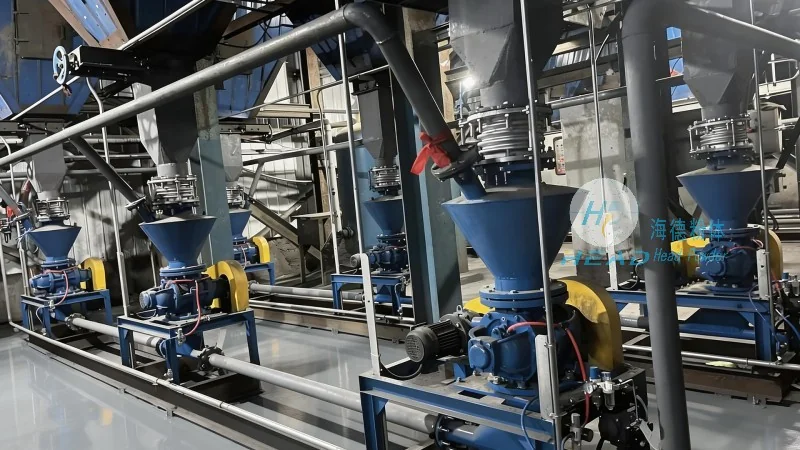
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a prominent engineering firm headquartered in Shandong, China, specializes in the design, development, and manufacturing of advanced material handling systems. With a strong focus on innovation and customer-centric solutions, HeadPowder has established itself as a leader in the industry, particularly in pneumatic conveying technologies for bulk materials like cotton seed. The company's team of experienced engineers and technicians work collaboratively with clients to understand their unique operational challenges and provide tailored solutions that meet industry standards and regulatory requirements. HeadPowder's commitment to quality is evident in its state-of-the-art manufacturing facilities, equipped with precision machinery and rigorous quality control processes. Each system is tested under real-world conditions to ensure reliability and performance before delivery. The company's services extend beyond system design and manufacturing, encompassing installation, commissioning, and comprehensive after-sales support. This comprehensive approach ensures that clients receive not only a high-quality product but also ongoing support to maximize the system's performance and lifespan. HeadPowder's reputation for excellence and reliability has made it a trusted partner for businesses in the agricultural, food processing, and related industries, helping them achieve operational efficiency and cost savings through advanced material handling solutions.




