Multi-point feeding powder conveyors are advanced industrial equipment designed to efficiently transport bulk powders from multiple feeding points to a central collection or processing unit. These systems are widely used in various industries, including pharmaceuticals, chemicals, food processing, and mining, where precise and reliable powder handling is critical. The core functionality of a multi-point feeding powder conveyor lies in its ability to integrate multiple input sources and manage the flow of materials seamlessly, ensuring consistent performance under diverse operational conditions.
Principle of Operation
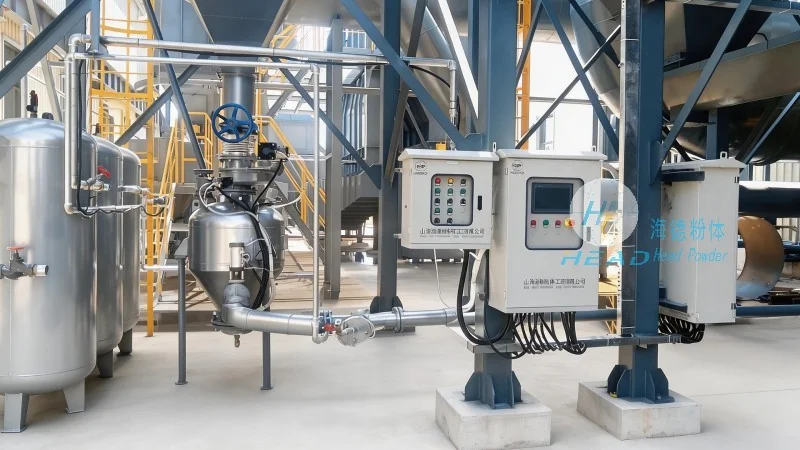
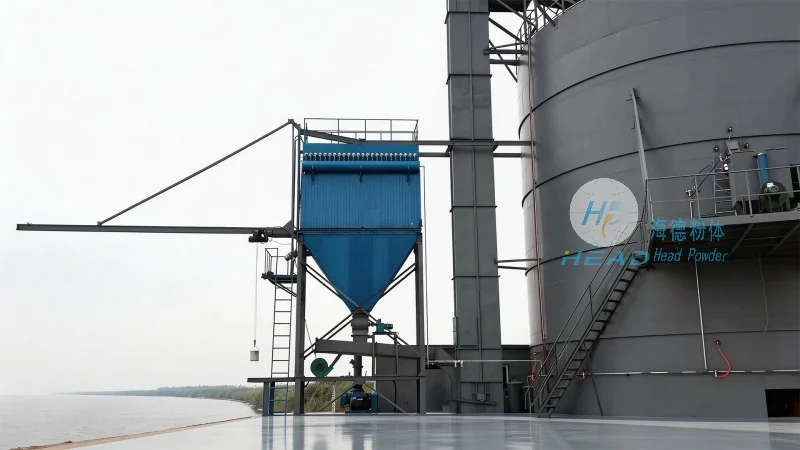
The operation of a multi-point feeding powder conveyor is based on a combination of mechanical and pneumatic principles. Typically, the system consists of a main conveyor line with multiple inlet hoppers, each connected to a separate feeding source. As powders are introduced into the inlet hoppers, they are drawn into the conveyor via a vacuum or pressure differential. The conveyor then transports the material through a pipeline to a central outlet or processing station. Key components include feed hoppers, control valves, and a main conveying duct, all working in tandem to regulate the flow rate and direction of the powder. The system often incorporates sensors and control panels to monitor and adjust the feeding process in real-time, ensuring optimal performance and preventing material blockages or overloading. Advanced models may also feature variable speed drives and automated batching systems, allowing for precise control over the amount of material conveyed per batch. This level of control is crucial in industries where consistency is paramount, such as in the production of pharmaceuticals or food products.
Working Scene Characteristics
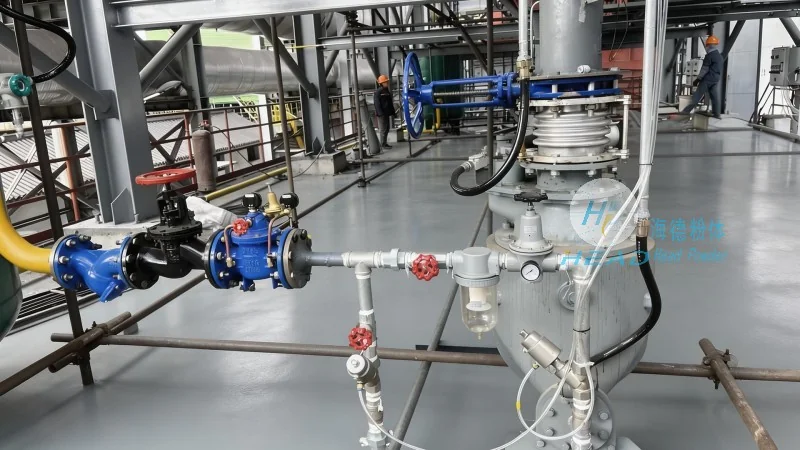
Multi-point feeding powder conveyors are particularly suited for applications where powders need to be collected from multiple locations or processing stages. For instance, in a pharmaceutical manufacturing plant, powders from different raw material batches may be fed into a central mixing unit through separate feeding points. The conveyor ensures that each batch is delivered at the correct rate and in the right sequence, maintaining product quality and batch traceability. In chemical processing facilities, these systems are used to transport reactive powders from storage silos to reactors, where precise dosing is essential for reaction control. The working scene characteristics also include adaptability to different powder types, such as fine powders, granules, or bulk materials, and the ability to handle varying flow rates based on production demands. Additionally, the design allows for easy integration with existing production lines, minimizing downtime during installation and operation. In mining operations, multi-point feeding conveyors are used to transport ore from multiple extraction points to a central processing plant, optimizing the extraction and processing workflow. The versatility of these systems makes them indispensable in industries where efficient material handling directly impacts production efficiency and cost-effectiveness.
Manufacturer Information
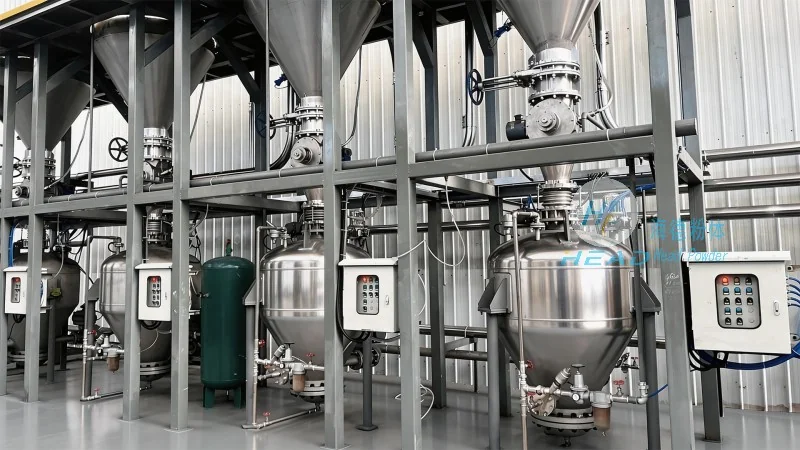
HeadPowder, a leading manufacturer of powder handling equipment, specializes in the design and production of multi-point feeding powder conveyors. With a strong presence in Shandong, China, HeadPowder Engineering Co., Ltd. leverages advanced engineering and manufacturing capabilities to deliver high-quality, reliable equipment tailored to the needs of various industries. The company's commitment to innovation and customer satisfaction is reflected in its comprehensive product line, which includes customized solutions for specific application requirements. HeadPowder's multi-point feeding powder conveyors are engineered to meet international standards for safety, efficiency, and durability, ensuring long-term performance and minimal maintenance costs for users. The company's R&D team continuously works on improving the technology, incorporating features like energy-efficient designs and smart control systems to enhance operational efficiency. HeadPowder also provides comprehensive after-sales support, including installation guidance, maintenance services, and technical assistance, ensuring that clients can maximize the lifespan and performance of their equipment.




