HeadPowder, a prominent entity in the field of powder handling technology, specializes in the design, manufacturing, and implementation of advanced large-scale powder conveying systems. With a strong presence in China, particularly in Shandong, the company has established itself as a reliable partner for industries requiring efficient and reliable powder transport solutions.
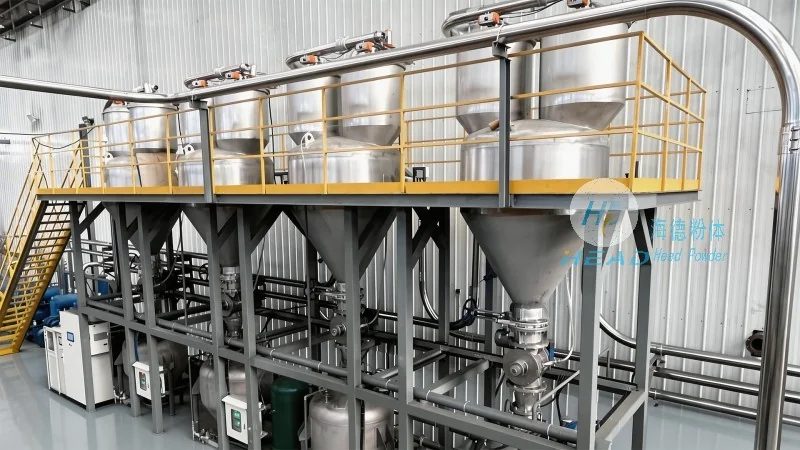
About HeadPowder: A Leading Manufacturer of Powder Conveying Solutions
HeadPowder, operating under the full name Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company has built a reputation for delivering high-quality, customized powder conveying equipment tailored to the diverse needs of various industrial sectors. By combining technical expertise with practical application experience, HeadPowder ensures that its products meet stringent industry standards and provide long-term operational efficiency.
Principles of Large-Scale Powder Conveying Systems
Large-scale powder conveying machines operate on fundamental principles that ensure the efficient transport of bulk powders over significant distances. These systems typically utilize mechanisms such as pneumatic or mechanical conveying, where powders are moved through pipelines using air pressure or mechanical force. The core components include feeders, conveyors, and control systems that work in tandem to maintain consistent flow rates and prevent material degradation. Advanced systems may incorporate features like variable speed drives, pressure regulation, and material monitoring to optimize performance and minimize downtime. The design of these machines is tailored to handle a wide range of powder characteristics, including particle size, density, and moisture content, ensuring compatibility with diverse materials like cement, chemicals, food products, and pharmaceuticals.
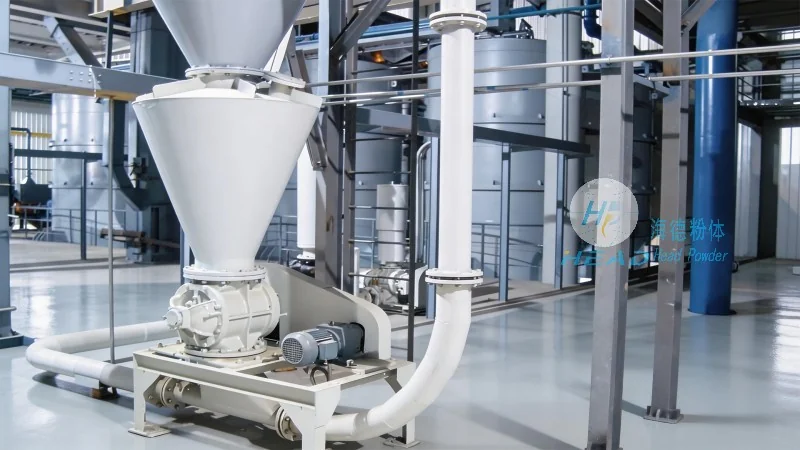
Working Scene Characteristics of Large-Scale Powder Conveying Machines
The working scene characteristics of large-scale powder conveying machines are shaped by the specific operational environments and application requirements. In industrial settings, these systems are often integrated into production lines where continuous material flow is critical for maintaining productivity. The machines are designed to operate in both indoor and outdoor environments, with robust construction to withstand harsh conditions such as temperature fluctuations, dust, and moisture. Key characteristics include high throughput capacity, which allows for the rapid transport of large volumes of powder, and flexibility in conveying routes, enabling adaptation to complex layouts. Additionally, these systems are engineered for low maintenance and high reliability, reducing operational costs and ensuring consistent performance over extended periods. The working scene also emphasizes safety features, such as enclosed systems to prevent dust emissions and automated controls to minimize human intervention, aligning with modern industrial safety standards.
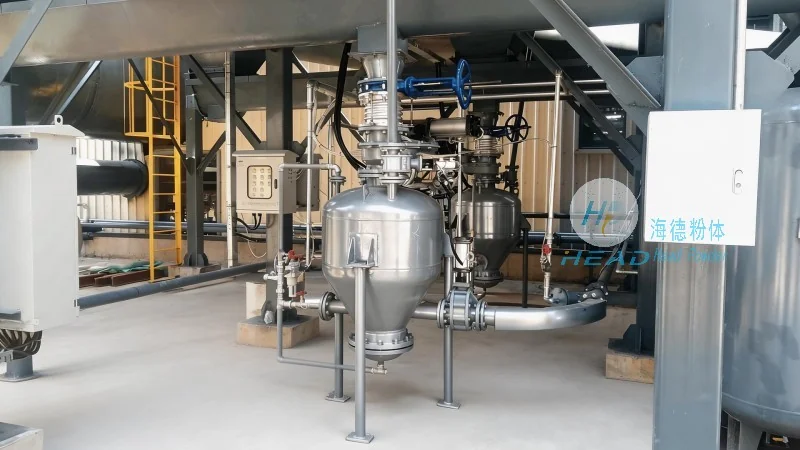
Application Scenarios and Industry Integration
Large-scale powder conveying machines find extensive application across multiple industries, each with unique operational demands. In the construction sector, these systems are crucial for transporting cement, fly ash, and other bulk materials to construction sites, ensuring smooth supply chains and reducing material handling time. The chemical industry utilizes them for the transport of raw materials and finished products, such as powders used in pharmaceuticals or industrial chemicals, where precision and contamination control are paramount. The food and beverage industry relies on these machines for handling ingredients like flour, sugar, and spices, maintaining hygiene standards and preventing cross-contamination. Similarly, the pharmaceutical sector benefits from the precise and controlled transport of powders, ensuring compliance with regulatory requirements and product quality. Each application scenario leverages the efficiency and reliability of large-scale powder conveying systems to enhance operational efficiency and meet industry-specific challenges.
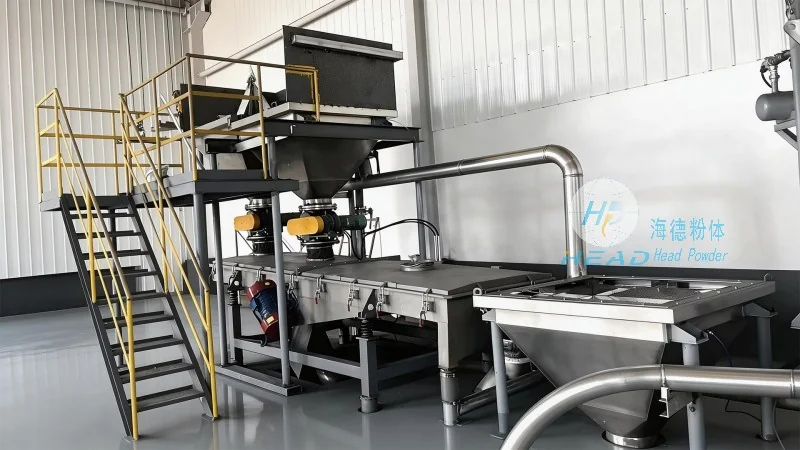
Advantages and Technical Innovations
The adoption of large-scale powder conveying machines offers several advantages that contribute to improved operational performance and cost-effectiveness. These systems provide significant energy savings compared to traditional manual or small-scale conveying methods, as they can transport large volumes of material with minimal power consumption. The automated nature of these machines reduces labor costs and minimizes human error, leading to higher productivity and consistent quality. Furthermore, the modular design of many large-scale systems allows for easy expansion or reconfiguration, adapting to changing production needs without major overhauls. Technical innovations, such as advanced control systems and predictive maintenance tools, enhance system reliability and reduce maintenance intervals. These innovations also enable real-time monitoring of system performance, allowing for proactive adjustments to optimize efficiency and prevent potential issues before they impact operations.
Conclusion: The Role of Large-Scale Powder Conveying Machines in Modern Industry
Large-scale powder conveying machines, as exemplified by the solutions offered by HeadPowder, play a vital role in modern industrial operations. By integrating advanced principles and robust design, these systems address the challenges of efficient bulk material transport, ensuring reliability, efficiency, and cost-effectiveness. The working scene characteristics and application scenarios highlight the versatility and adaptability of these machines, making them indispensable in various industries. As industries continue to evolve, the demand for sophisticated powder handling solutions will remain high, and companies like HeadPowder will continue to innovate, providing tailored solutions that meet the evolving needs of the market.




