Intelligent ingredient material conveying lines represent a pivotal advancement in modern industrial processing, particularly within sectors that demand precise and efficient handling of raw materials. These systems are designed to streamline the entire process of ingredient preparation, from initial reception to final delivery to processing units. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the development and implementation of such advanced conveying solutions. This article delves into the working principle and key features of intelligent ingredient material conveying lines, highlighting how they enhance operational efficiency and product quality.
Working Principle of Intelligent Ingredient Material Conveying Lines
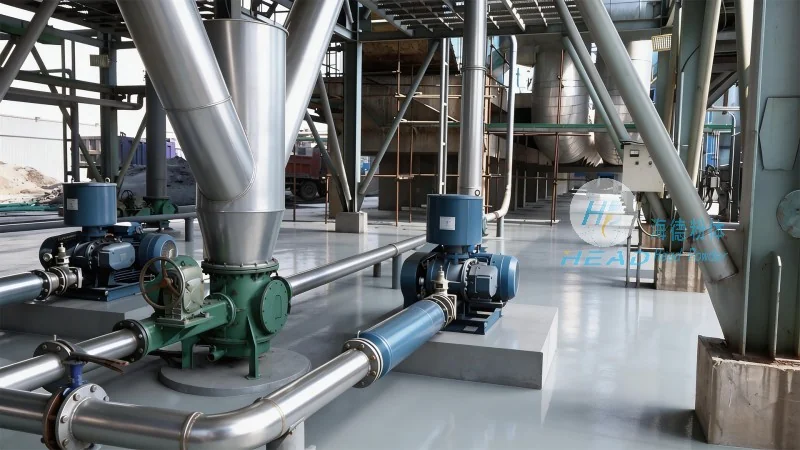
The core working principle of an intelligent ingredient material conveying line revolves around a sophisticated integration of hardware and software components. At its foundation, the system utilizes advanced sensors and identification technologies to detect and classify different ingredient types. This initial step ensures that each material is accurately recognized, which is crucial for maintaining the integrity of the final product. The process typically begins with the reception of raw ingredients, where the line’s sensors scan and record the characteristics of each batch. Subsequently, the system employs a programmable logic controller (PLC) or a more advanced industrial computer system to manage the entire workflow. These control systems coordinate the operation of various components, including conveyor belts, elevators, and storage bins, ensuring that materials are transported in the correct sequence and at the optimal speed.
Once the ingredients are identified and verified, the conveying line transitions into the active transport phase. This involves the use of automated conveying equipment such as belt conveyors, screw conveyors, or pneumatic systems, depending on the material properties and processing requirements. The intelligent system continuously monitors the flow of materials, adjusting the speed and direction of the conveyors as needed to prevent bottlenecks or overloading. For instance, if a particular ingredient is detected to be in excess, the system can automatically redirect it to an alternative storage or processing route. This dynamic adjustment capability is a hallmark of intelligent conveying systems, enabling real-time optimization of the material handling process.
Key Features of Intelligent Ingredient Material Conveying Lines
Intelligent ingredient material conveying lines are distinguished by several critical features that set them apart from traditional manual or semi-automated systems. The first and most notable feature is the high degree of automation. By eliminating the need for manual intervention in the material handling process, these systems reduce human error and labor costs while increasing operational consistency. The automation is supported by advanced control algorithms that can adapt to changing conditions, ensuring that the system remains efficient even under varying production loads.
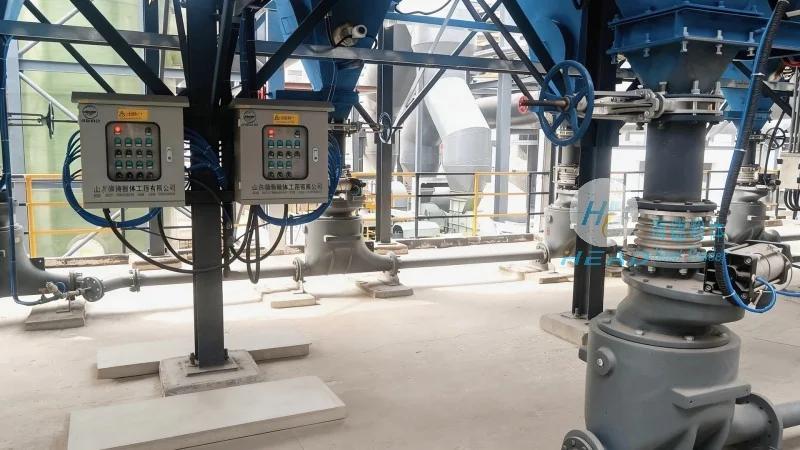
A second key feature is the precision and accuracy in ingredient measurement and distribution. Modern intelligent conveying lines are equipped with high-precision weighing and dosing mechanisms, which are essential for applications where the exact quantity of each ingredient is critical, such as in pharmaceuticals, food processing, or chemical manufacturing. These systems can achieve measurement accuracies within a fraction of a percent, ensuring that the final product meets stringent quality standards. The integration of these precision components with the overall conveying system allows for seamless and reliable ingredient delivery to the next stage of production.
A third significant feature is the enhanced safety and reliability. Intelligent conveying lines incorporate multiple safety sensors and redundancy measures to prevent accidents and system failures. For example, emergency stop buttons, overload detection systems, and collision avoidance sensors are standard features. These safety measures not only protect personnel but also minimize downtime by quickly identifying and addressing potential issues. The reliability of the system is further improved through regular maintenance alerts and predictive diagnostics, which help in proactively identifying and resolving problems before they escalate.
Benefits of Implementing Intelligent Ingredient Material Conveying Lines
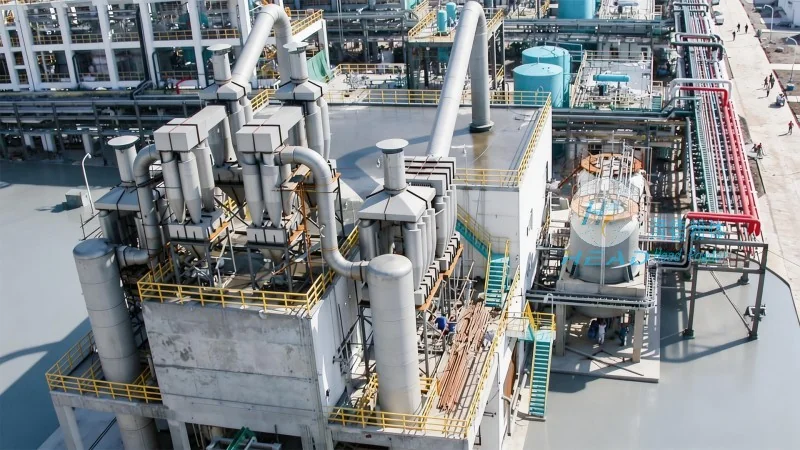
The adoption of intelligent ingredient material conveying lines brings numerous benefits to industrial operations. From a productivity standpoint, these systems significantly reduce the time required for material handling, allowing production lines to operate at higher throughput rates. The automation also frees up human resources, enabling workers to focus on more value-added tasks, such as quality control or process optimization. In terms of cost, the reduction in labor and material waste, combined with lower maintenance costs due to the system’s reliability, results in substantial savings over the long term.
From a quality perspective, the precision and consistency offered by intelligent conveying lines directly impact the quality of the final product. By ensuring that each ingredient is measured and delivered accurately, these systems help maintain product uniformity and meet regulatory requirements. This is particularly important in industries where product consistency is non-negotiable, such as in the food and pharmaceutical sectors. Additionally, the real-time monitoring capabilities of the system provide valuable data on material flow and usage, which can be used for continuous improvement and process optimization.
Conclusion
In conclusion, intelligent ingredient material conveying lines represent a cutting-edge solution for modern industrial material handling. Through their sophisticated working principles and advanced features, these systems enhance operational efficiency, improve product quality, and reduce costs. As a company dedicated to innovation and excellence, Shandong HeadPowder Engineering Co., Ltd. continues to lead in the development of such advanced technologies, providing tailored solutions that meet the specific needs of its clients. By investing in intelligent conveying systems, industries can achieve a competitive edge in today’s fast-paced and demanding market.




