

What is a Chocolate Powder Pneumatic Conveying System? And What Are Its Design Principles?
Chocolate powder pneumatic conveying systems are specialized equipment designed to transport chocolate powders and related bulk materials efficiently and safely. These systems are crucial in the food processing industry, particularly for handling delicate and high-value products like chocolate powders, which require careful handling to maintain quality and prevent contamination. The design of such systems must account for the unique properties of chocolate powders, including their hygroscopic nature, particle size distribution, and flow characteristics.
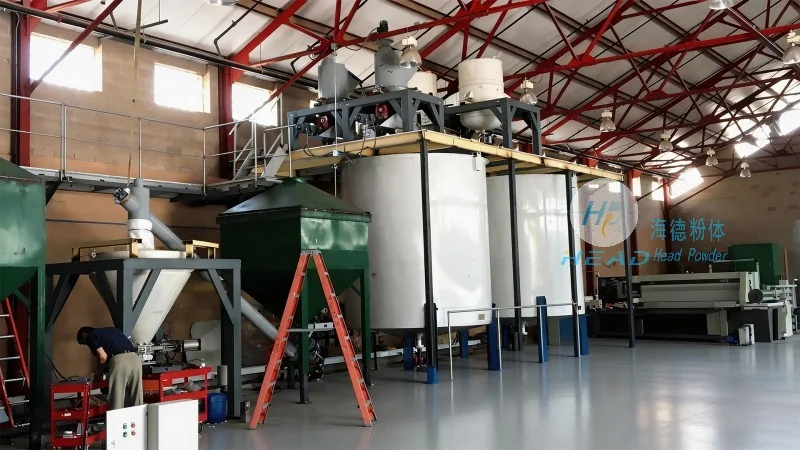
Introduction to Chocolate Powder Pneumatic Conveying Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in developing advanced pneumatic conveying solutions tailored for the chocolate industry. The company's expertise lies in understanding the specific challenges associated with chocolate powders, such as their tendency to clump, stick to surfaces, and absorb moisture from the environment. By addressing these challenges through innovative design, HeadPowder ensures that their systems provide reliable and efficient material transport while maintaining product integrity.
Design Principles of Pneumatic Conveying Systems for Chocolate Powders
The core design principle of a chocolate powder pneumatic conveying system is to use compressed air to move the powder from a source to a destination. This method, known as pneumatic conveying, offers several advantages over traditional mechanical conveying, including reduced product degradation, lower risk of contamination, and improved process control. The system typically consists of several key components, including a hopper for material storage, a feeder to control the flow rate, a conveying line (often with bends and elbows), and a receiver for the discharged material. Each component is carefully engineered to handle the specific characteristics of chocolate powders.
For chocolate powders, the design must consider the material's hygroscopicity, which means it can absorb moisture from the air. This property requires the system to be equipped with drying or moisture control mechanisms to prevent caking and ensure consistent flow. Additionally, the particle size and density of chocolate powders influence the air velocity and pressure needed for effective conveying. HeadPowder's systems are designed with adjustable air flow rates and pressure control to accommodate different powder types and processing requirements.
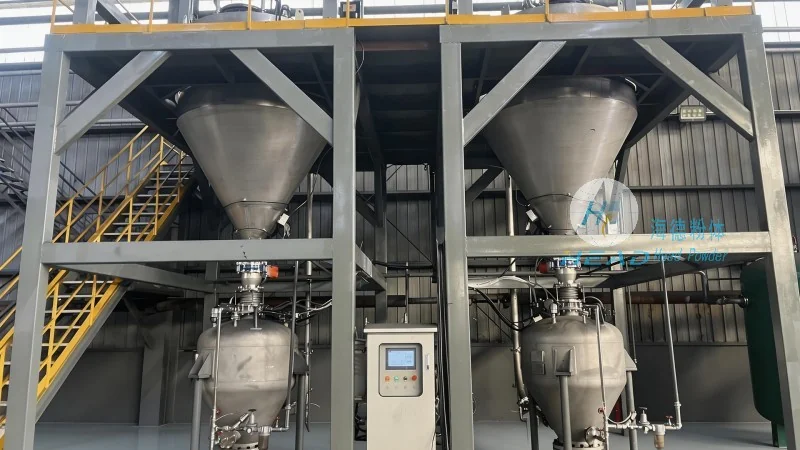
Key Design Considerations for Chocolate Powder Handling
When designing a pneumatic conveying system for chocolate powders, several factors must be taken into account to ensure optimal performance. First, the system must maintain a consistent air flow to prevent material buildup or blockages in the conveying line. This is achieved through the use of positive displacement blowers or rotary lobe pumps, which provide a steady pressure and flow rate. Second, the system should incorporate features to prevent product degradation, such as gentle material handling and minimal exposure to air, which can cause oxidation or flavor loss.
Third, the design must address the potential for product contamination, which is a critical concern in the food industry. HeadPowder's systems are constructed with food-grade materials, such as stainless steel, and include sanitary design features to minimize the risk of cross-contamination. The system also includes cleaning mechanisms, such as CIP (Clean-In-Place) systems, to ensure thorough sanitation between batches.
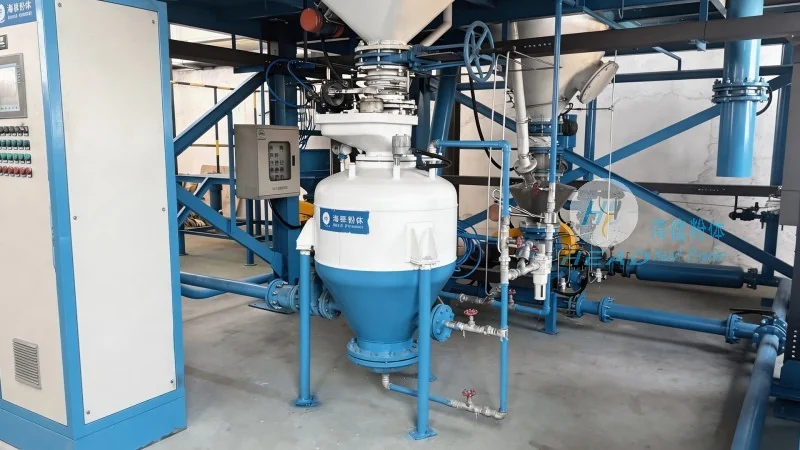
Advantages of Using Pneumatic Conveying for Chocolate Powders
Implementing a pneumatic conveying system for chocolate powders offers numerous benefits for food processing facilities. One of the primary advantages is the ability to transport materials in a closed system, which prevents exposure to dust, moisture, and contaminants. This closed-loop design also reduces the risk of product loss and improves overall process efficiency. Additionally, pneumatic conveying allows for flexible system integration, as the equipment can be easily connected to existing processing lines or expanded to accommodate increased production volumes.
Another key advantage is the reduced labor and maintenance requirements compared to traditional mechanical conveying. Pneumatic systems require less manual handling of materials and have fewer moving parts, resulting in lower operational costs and increased reliability. Furthermore, the gentle handling of chocolate powders by pneumatic systems helps maintain product quality, ensuring that the final product meets the highest standards of taste and texture.
Conclusion
Chocolate powder pneumatic conveying systems, as designed by companies like Shandong HeadPowder Engineering Co., Ltd., represent a sophisticated solution for the efficient and safe transport of delicate bulk materials. By integrating advanced design principles, such as moisture control, gentle handling, and sanitary construction, these systems address the unique challenges of chocolate powder processing. The result is a reliable, efficient, and cost-effective method for moving chocolate powders through the production process, ensuring product quality and meeting the demands of modern food processing operations.