HeadPowder, a leading provider in the field, specializes in the design, manufacturing, and implementation of pneumatic conveying systems tailored for the mining industry. These systems are essential for efficiently transporting bulk materials such as ores, coal, and other minerals from extraction sites to processing facilities. The technology behind pneumatic conveying leverages the principles of air flow to move particles through pipelines, offering a flexible and efficient alternative to traditional mechanical conveyors.
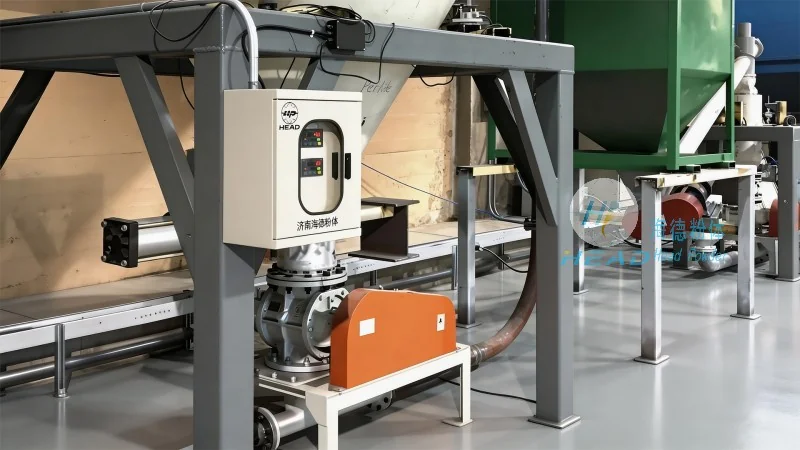
Working Principle of Pneumatic Conveying
The core mechanism of pneumatic conveying involves the use of compressed air or gas to create a flow that transports solid materials. In a typical system, material is fed into a hopper or feeder, where it is then introduced into a pipeline. The air, often under pressure, moves through the pipeline, carrying the material particles along. The system can operate in either positive pressure or negative pressure modes. Positive pressure systems force air and material through the pipeline, while negative pressure systems draw material into the pipeline using a vacuum. This dual approach allows for the handling of a wide range of materials, from fine powders to larger lumps, with varying moisture content and particle sizes.
Key Components and Their Roles
Several critical components make up a pneumatic conveying system. The feeder or hopper is responsible for controlling the flow rate of the material into the system. The pipeline itself is designed to withstand the pressure and abrasion from the material and air. The air compressor or vacuum pump provides the necessary pressure or suction to drive the material through the system. Additionally, filters and cyclones are used to separate the material from the air at the end of the pipeline, ensuring that the material is delivered to the destination without contamination. The control system manages the entire process, adjusting air pressure, flow rates, and material feed to maintain optimal performance.
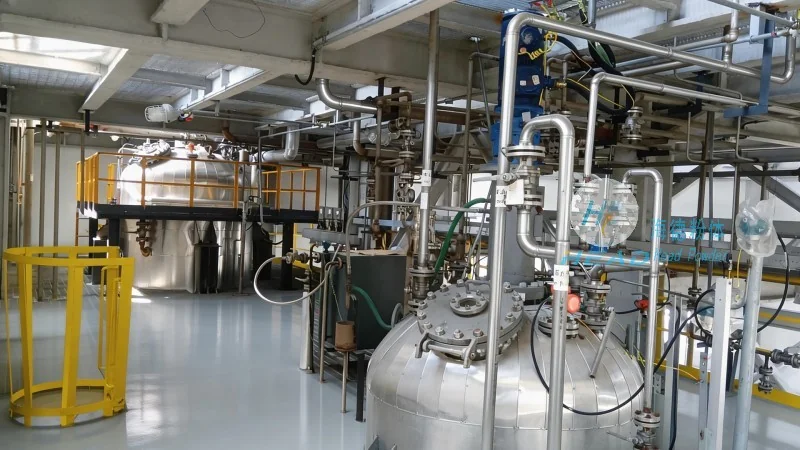
Operation Process of Mine Material Pneumatic Conveying
The operation process begins with the loading of material into the hopper. The feeder then regulates the material flow, ensuring a consistent rate of input. The air compressor generates the required pressure, which is then introduced into the pipeline. As the air flows through the pipeline, it picks up the material particles and transports them to the receiving hopper or storage area. At the end of the pipeline, a separator, such as a cyclone or filter, separates the material from the air. The material is collected in the receiving hopper, while the air is either vented or recirculated back into the system. This continuous cycle allows for the efficient and reliable transport of mine materials, minimizing downtime and maximizing throughput.
Advantages of Pneumatic Conveying in Mining
Pneumatic conveying systems offer several advantages over traditional mechanical conveyors. They are highly flexible, allowing for changes in material flow direction and pipeline layout without major modifications. The systems are also capable of handling materials with high moisture content or abrasive properties, which can damage mechanical components. Additionally, pneumatic conveying reduces the risk of material contamination and can be integrated with other processing equipment, such as crushers or screens, to form a complete material handling solution. The technology also minimizes the need for manual labor, improving safety and operational efficiency in mining operations.
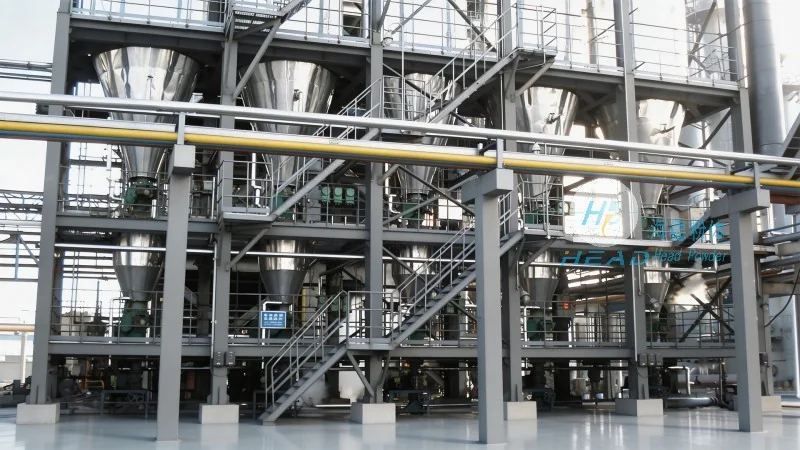
Applications in the Mining Industry
HeadPowder's pneumatic conveying systems are widely used in various mining applications. In coal mines, the systems transport coal from the extraction site to processing plants, where it is prepared for combustion or further processing. In metal mines, the systems handle ores and concentrates, moving them from the mine to smelters or refineries. The technology is also applied in the handling of non-metallic minerals, such as limestone and sand, for use in construction and industrial applications. The versatility of the systems makes them suitable for both underground and surface mining operations, adapting to the specific requirements of each project.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted partner for mining companies seeking reliable and efficient material handling solutions. With years of experience in the industry, the company provides customized pneumatic conveying systems that meet the unique needs of each client. By leveraging advanced technology and expert engineering, HeadPowder ensures that its systems operate at peak performance, delivering high throughput and low maintenance costs. The company's commitment to quality and customer satisfaction has made it a leader in the mining material handling sector, helping mining operations improve productivity and reduce operational costs.




