High-pressure bin pumps are critical equipment in modern material handling systems, designed to transport bulk materials with high efficiency and reliability. This article explores the concept of high-pressure bin pump material handling and delves into its fundamental design principles, providing a comprehensive understanding of this essential technology.
Understanding High-Pressure Bin Pump Material Handling
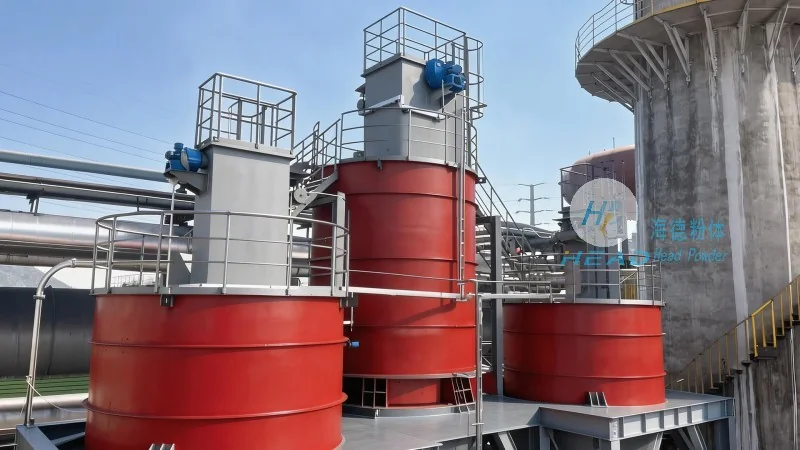
High-pressure bin pump material handling refers to the process of transporting bulk solid materials from storage bins or silos to processing units, such as reactors, mixers, or conveyors, using high-pressure pneumatic or hydraulic systems. Unlike traditional gravity-fed or low-pressure pneumatic systems, high-pressure bin pumps operate under elevated pressure, enabling them to handle materials with higher density, larger particle sizes, or those that are difficult to move through conventional methods. The system typically consists of a storage bin, a high-pressure pump, a control valve, and a discharge line, working together to create a pressurized environment that forces material flow.
Design Principles of High-Pressure Bin Pumps
The design of high-pressure bin pumps is based on several key principles to ensure optimal performance and safety. First, the pump must be capable of generating sufficient pressure to overcome the resistance of the material and the system's friction losses. This is achieved through the use of powerful compressors or hydraulic motors that can maintain consistent pressure levels, even under varying load conditions. Second, the pump's internal components, such as the cylinder, piston, and valve, are engineered to withstand high pressures and abrasive materials, ensuring long service life and minimal maintenance. The material selection for these components is crucial, as they must resist corrosion, wear, and thermal stress. Third, the system incorporates advanced control mechanisms, including pressure sensors, flow meters, and programmable logic controllers (PLCs), to monitor and regulate the pump's operation. These controls help maintain stable pressure, prevent over-pressurization, and adjust flow rates based on the material's characteristics and the system's requirements.
Key Components and Their Functions
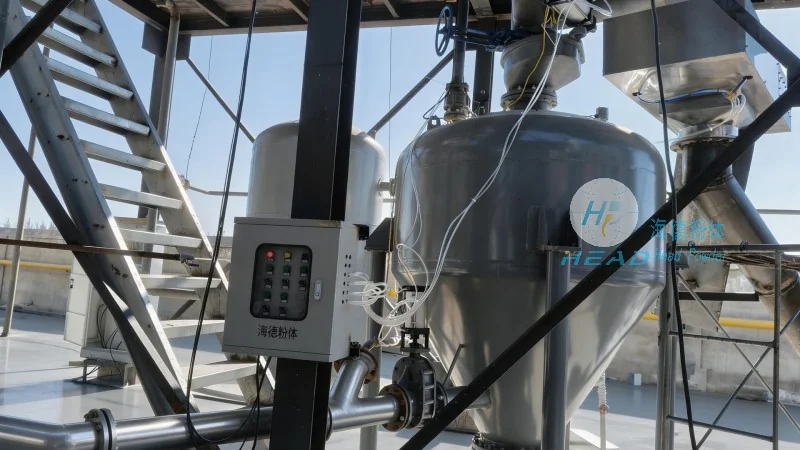
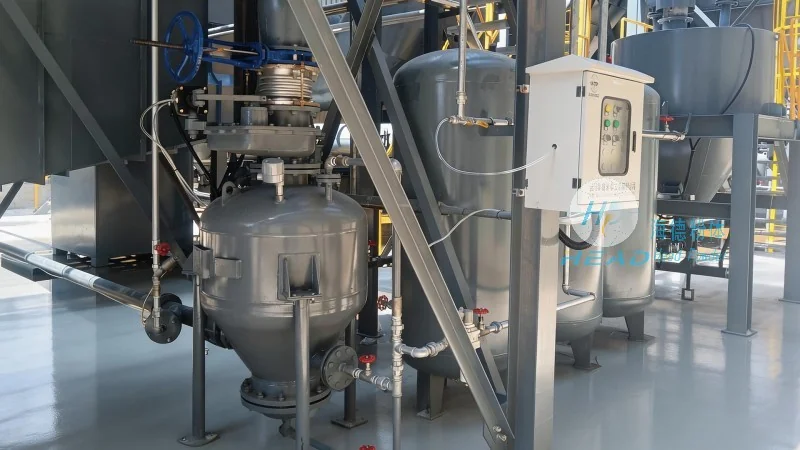
Several critical components make up a high-pressure bin pump system, each playing a vital role in the overall operation. The storage bin, often made of steel or other durable materials, serves as the material reservoir, holding the bulk material until it is needed. The bin is equipped with a hopper or inlet that connects to the pump's suction line, allowing material to be drawn into the system. The high-pressure pump, typically a reciprocating or rotary type, is the heart of the system. It creates the pressure differential that drives material flow. The pump's cylinder and piston work in a reciprocating motion, compressing air or hydraulic fluid to generate the necessary pressure. The control valve, usually a pressure relief or check valve, regulates the pressure within the system, preventing backflow and protecting the pump from damage. The discharge line, often made of reinforced plastic or metal, carries the pressurized material from the pump to the processing unit. Finally, the system may include a filter or separator to remove moisture or debris from the material, ensuring that only clean material is transported.
Applications and Benefits of High-Pressure Bin Pump Material Handling
High-pressure bin pumps are widely used in various industries, including chemical, pharmaceutical, food processing, and mining. They are particularly suitable for handling materials that are difficult to transport, such as powders, granules, or slurries with high moisture content. The benefits of using high-pressure bin pumps include increased material throughput, reduced downtime, and improved safety. By eliminating the need for manual handling or low-pressure systems, these pumps minimize the risk of material spillage, dust emissions, and worker exposure to hazardous materials. Additionally, the consistent pressure and flow control provided by the system ensure that processing units receive a steady supply of material, improving overall production efficiency.
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of high-quality material handling equipment, including high-pressure bin pumps. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry. Headpowder's products are designed to meet the specific needs of various applications, offering reliable performance and durability. The company's headquarters is located in Shandong, China, where it has a state-of-the-art manufacturing facility and a team of experienced engineers and technicians. Headpowder is committed to providing customized solutions for its clients, ensuring that each system is tailored to the unique requirements of the application. The company's dedication to quality and service has earned it a reputation for excellence in the market.




