Barley pneumatic conveying machines are specialized equipment designed for the efficient transport of barley grains in agricultural and industrial settings. These systems utilize air pressure or vacuum to move barley from one location to another, offering a clean and low-maintenance alternative to traditional mechanical conveyors. The technology is widely adopted in the grain processing industry due to its ability to handle delicate barley kernels without causing damage, which is crucial for maintaining grain quality during handling and processing.
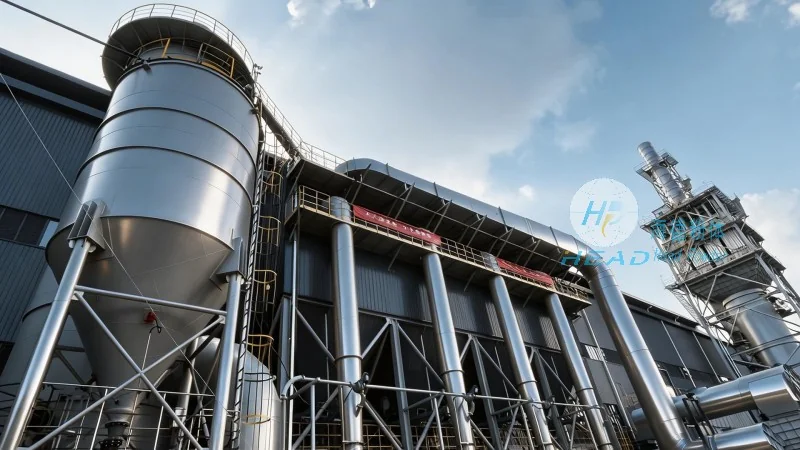
Key Design Principles of Barley Pneumatic Conveying Systems
The design of a barley pneumatic conveying machine is centered on several critical principles that ensure optimal performance and reliability. First, the system must be capable of generating sufficient air pressure or vacuum to overcome the resistance of the barley particles as they move through the pipeline. This is typically achieved through the use of blowers or vacuum pumps, which are selected based on the specific characteristics of the barley, such as particle size, moisture content, and bulk density. Second, the pipeline design is crucial; it must be constructed from materials that are resistant to corrosion and abrasion, as barley grains can be abrasive over time. Common materials include stainless steel, polyethylene, or specialized alloys that can withstand the continuous flow of grain and air. Third, the system incorporates components like inlets, outlets, and filters to manage the flow of barley and air effectively. Inlets are designed to introduce barley into the system in a controlled manner, often using hoppers or feeders that minimize spillage and ensure a consistent flow. Outlets are positioned to deliver the barley to the desired destination, such as storage silos or processing equipment. Filters are essential to prevent the accumulation of dust and debris in the system, which can reduce efficiency and cause equipment damage over time. Additionally, the system may include pressure relief valves and check valves to maintain safe operating conditions and prevent backflow.
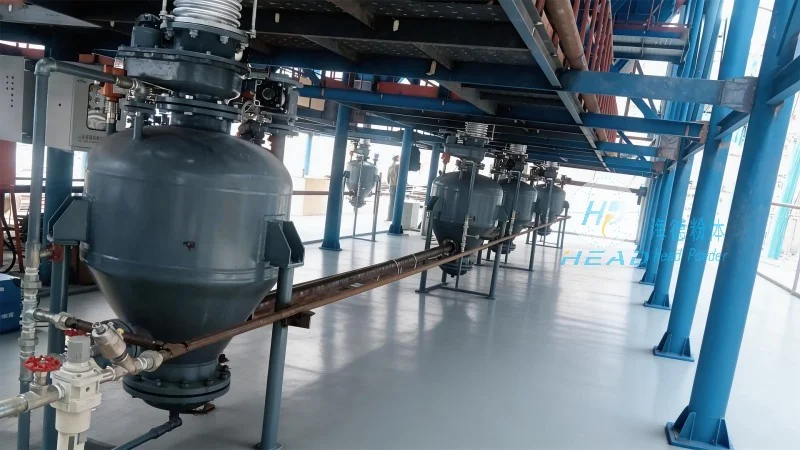
How Barley Pneumatic Conveying Machines Work
The operation of a barley pneumatic conveying machine involves a series of steps that work together to transport barley efficiently. The process begins with the loading of barley into a hopper or feeder, which is typically located at the start of the system. The feeder then controls the flow of barley into the pipeline, ensuring a steady supply of material. Simultaneously, a blower or vacuum pump generates the necessary air pressure or vacuum. In a pressure system, the blower pushes air into the pipeline, creating a positive pressure that propels the barley forward. The barley particles are suspended in the air stream and travel through the pipeline to the outlet. In a vacuum system, the pump creates a negative pressure that draws the barley into the pipeline. The air flow is designed to maintain the particles in a suspended state, preventing them from settling and clogging the system. The speed of the air flow is critical; it must be sufficient to keep the barley particles airborne but not so high as to cause excessive wear on the pipeline or components. The system also includes sensors and controls that monitor the flow rate and pressure, allowing for adjustments to be made in real-time to maintain optimal performance. This automation ensures that the system operates efficiently and safely, minimizing downtime and maximizing throughput.
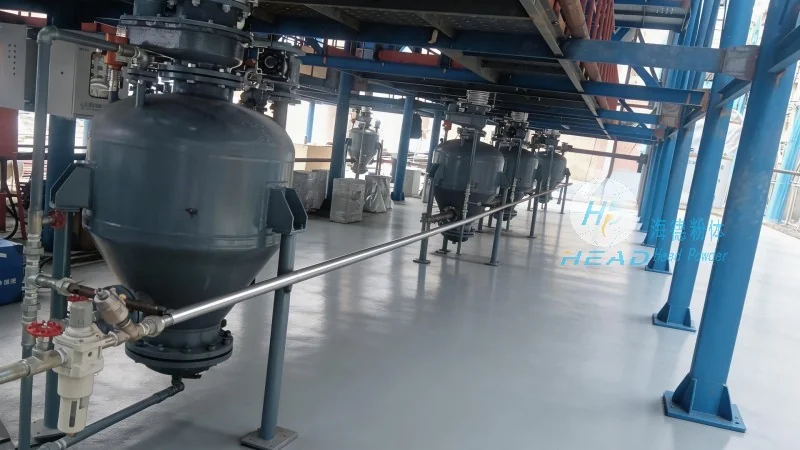
Applications and Benefits of Barley Pneumatic Conveying Machines
Barley pneumatic conveying machines are used in a variety of applications within the grain processing industry. They are commonly employed in malting facilities, where barley is transported from storage to the malting process. The machines are also used in breweries and distilleries to move barley from storage to milling and brewing equipment. In addition, they are used in feed mills and animal feed production facilities to transport barley as part of the feed mix. The benefits of using pneumatic conveying systems for barley are numerous. First, they offer a clean and hygienic method of transport, as the system is enclosed and prevents contamination from external sources. This is particularly important in food processing applications where maintaining grain quality and safety is paramount. Second, pneumatic conveying systems are low-maintenance compared to traditional mechanical conveyors. They have fewer moving parts, which reduces the risk of breakdowns and the need for frequent repairs. Third, the systems are flexible and can be easily modified to accommodate changes in production volume or process requirements. This adaptability makes them a cost-effective solution for businesses that need to scale their operations. Fourth, the systems are energy-efficient, as they use less power than mechanical conveyors to achieve the same level of throughput. The use of air as the primary transport medium reduces energy consumption and lowers operating costs. Finally, pneumatic conveying systems are environmentally friendly, as they do not generate dust or noise pollution, which is a significant advantage in industrial settings.
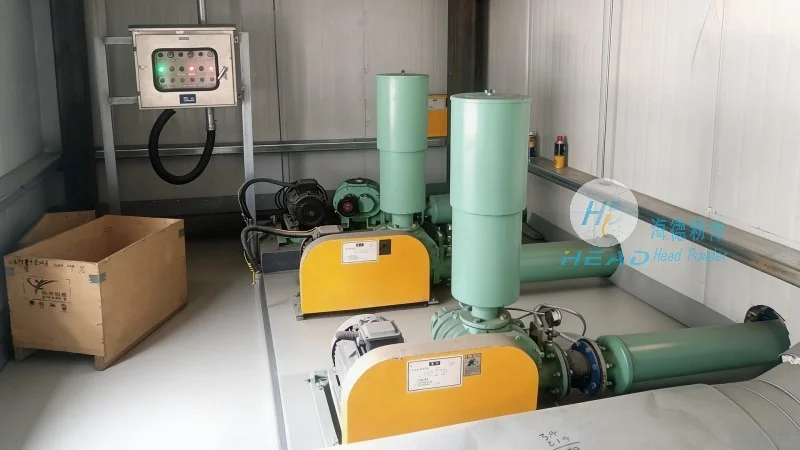
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of barley pneumatic conveying machines and related equipment. The company is based in Shandong, China, and has been in operation for over 20 years, providing high-quality, reliable equipment to customers worldwide. HeadPowder specializes in designing and manufacturing custom pneumatic conveying systems tailored to the specific needs of their clients. The company's team of engineers and technicians has extensive experience in the grain processing industry, ensuring that their products meet the highest standards of performance and durability. HeadPowder's commitment to quality is reflected in their use of advanced manufacturing techniques and rigorous quality control processes. All products are tested and inspected before delivery to ensure that they meet the customer's specifications and industry standards. The company also provides after-sales support, including maintenance, repair, and technical assistance, to ensure that their customers' equipment operates at peak performance. HeadPowder's goal is to provide the best possible service and support to their customers, helping them to achieve their production goals efficiently and effectively.




