Welcome to the official website of Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in high-quality powder conveying systems. In this article, we will explore the positive pressure dilute phase powder conveying system, its core components, and the underlying design principles that make it an efficient solution for transporting bulk powders.
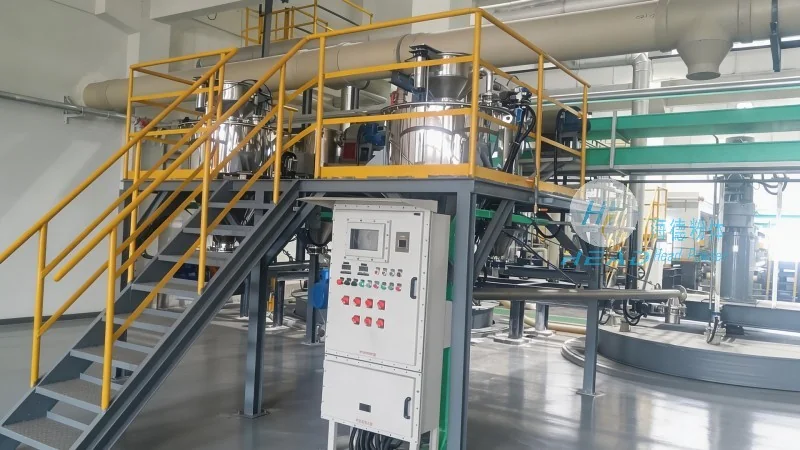
Understanding the Positive Pressure Dilute Phase Powder Conveying System
A positive pressure dilute phase powder conveying system is a specialized equipment designed to transport dry powders and particulate materials through a pipeline under positive pressure. Unlike dense phase conveying, which uses high pressure to push material through a pipeline, the dilute phase system operates by creating a low-pressure zone in the receiving end and maintaining a positive pressure in the conveying line. This method ensures that the material is suspended in a carrier gas, typically air, and moves efficiently through the system. The system is widely used in various industries, including chemical, pharmaceutical, food, and mining, due to its ability to handle a wide range of powder types and its flexibility in conveying distances and elevations.
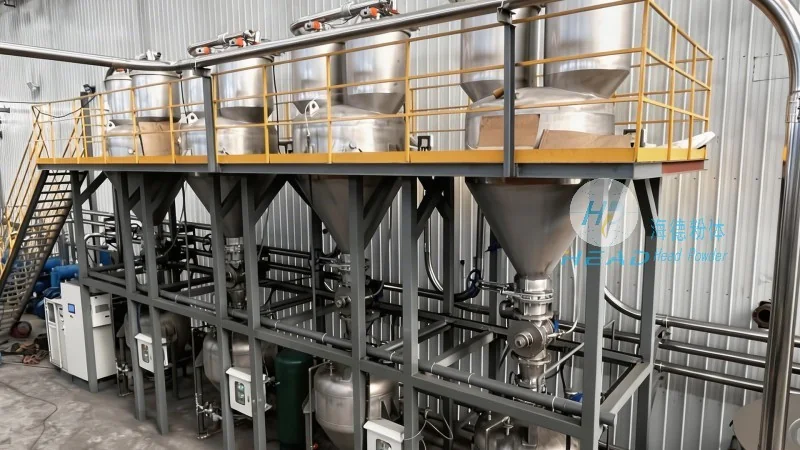
Key Components of the Positive Pressure Dilute Phase Powder Conveying System
The positive pressure dilute phase powder conveying system consists of several critical components that work in tandem to ensure smooth and efficient operation. The main components include a material feeder, a positive pressure blower or compressor, a pipeline system, a dust filter, and a receiving hopper. The material feeder is responsible for feeding the powder into the system, ensuring a consistent flow rate. The positive pressure blower or compressor provides the necessary air pressure to move the powder through the pipeline. The pipeline system is typically made of stainless steel or other corrosion-resistant materials to handle various powder types and prevent material buildup. The dust filter is crucial for capturing any airborne particles and ensuring compliance with environmental regulations. Finally, the receiving hopper collects the conveyed material and can be connected to downstream processes.
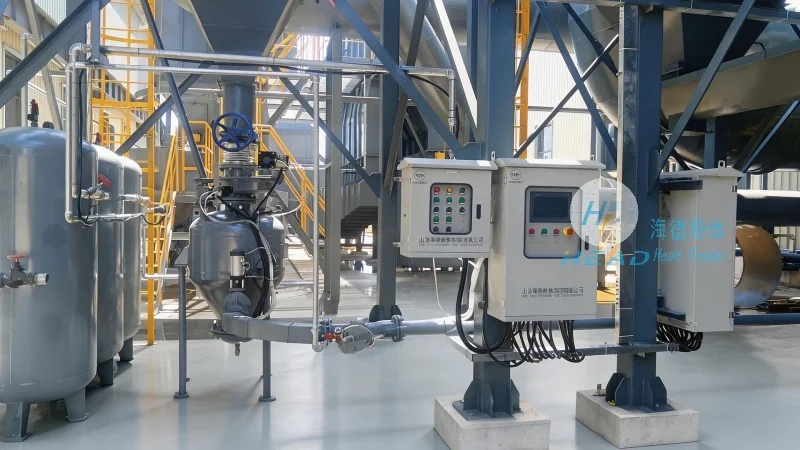
Design Principles Behind the Positive Pressure Dilute Phase Powder Conveying System
The design of a positive pressure dilute phase powder conveying system is based on several key principles that optimize performance and efficiency. The first principle is the use of a positive pressure environment, which prevents the material from settling in the pipeline and ensures continuous flow. The second principle is the dilute phase operation, where the powder is suspended in a carrier gas, reducing the risk of blockages and ensuring uniform flow. The third principle is the selection of appropriate equipment components, such as the blower or compressor, which must be capable of providing sufficient pressure and airflow to handle the specific powder characteristics. Additionally, the system design considers factors like pipeline length, elevation changes, and material properties to ensure optimal performance. Engineers at Shandong HeadPowder Engineering Co., Ltd. employ advanced engineering techniques and extensive experience to design systems that meet the unique requirements of each application, ensuring reliable and efficient powder transport.
Applications and Benefits of the Positive Pressure Dilute Phase Powder Conveying System
The positive pressure dilute phase powder conveying system offers numerous benefits and is suitable for a wide range of applications. One of the primary benefits is its ability to handle a variety of powder types, including fine powders, coarse powders, and mixtures of different materials. This versatility makes it ideal for industries that require the transport of diverse bulk materials. Another benefit is its efficiency in terms of energy consumption and operational costs. By using a positive pressure system, the equipment can operate with lower energy requirements compared to other conveying methods, resulting in cost savings for the end-user. Additionally, the system is relatively simple to install and maintain, reducing downtime and maintenance costs. The positive pressure dilute phase powder conveying system is also known for its ability to handle long conveying distances and high elevations, making it suitable for applications where other conveying methods may not be feasible. Overall, this system provides a reliable and efficient solution for bulk powder transport, enhancing productivity and reducing operational challenges in various industrial settings.
Conclusion and Company Information
Shandong HeadPowder Engineering Co., Ltd. is committed to providing high-quality positive pressure dilute phase powder conveying systems that meet the needs of our clients. Our team of experienced engineers and technicians uses advanced design principles and manufacturing techniques to ensure that our equipment is reliable, efficient, and durable. We understand that each application has unique requirements, and we work closely with our clients to develop customized solutions that optimize performance and minimize costs. With our headquarters in Shandong, China, we serve clients worldwide, providing comprehensive support and after-sales service to ensure long-term satisfaction. If you are in need of a reliable powder conveying system, contact us today to learn more about our products and services.




