At Shandong HeadPowder Engineering Co., Ltd., we specialize in providing efficient and reliable air-powered conveying solutions for various industrial applications. Pneumatic conveying systems utilize compressed air to transport bulk materials, offering advantages such as non-contact material handling, reduced contamination, and the ability to handle a wide range of materials from powders to granules. Our solutions are tailored to meet the specific needs of clients, ensuring optimal performance and cost-effectiveness.
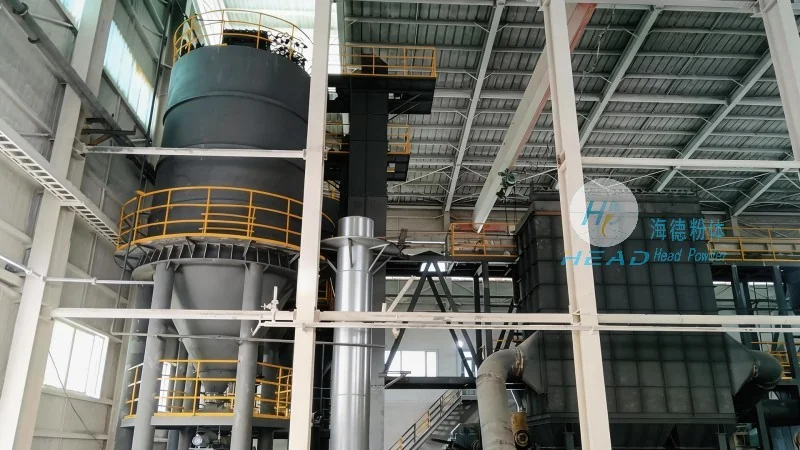
Company Overview: HeadPowder
HeadPowder, a leading manufacturer in the field of pneumatic conveying technology, is committed to delivering high-quality equipment and services. With a strong presence in China, our company, Shandong HeadPowder Engineering Co., Ltd., has established itself as a trusted partner for industries requiring robust material transport solutions. Our headquarters are located in Shandong, China, where we leverage local expertise and resources to develop innovative systems that address the evolving demands of modern manufacturing.
Key Features of Air-Powered Conveying
Our air-powered conveying systems are designed with several key features that enhance their performance and usability. These include adjustable air pressure controls, which allow for precise material flow regulation; durable construction materials, such as stainless steel and corrosion-resistant alloys, to ensure longevity and resistance to harsh environments; and integrated filtration systems to maintain material purity and comply with industry standards. Additionally, our systems are equipped with safety features, including pressure relief valves and emergency shut-off mechanisms, to prevent accidents and ensure operational safety.
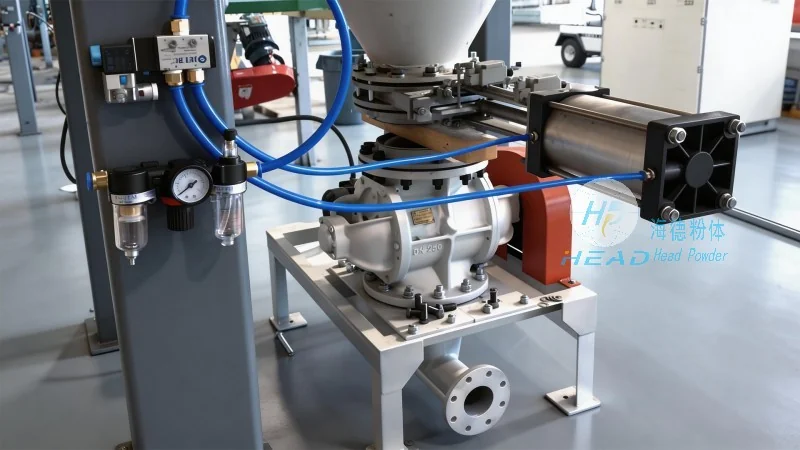
Option 1: Dilute Phase Pneumatic Conveying
Dilute phase pneumatic conveying is a common method for transporting materials over moderate distances. This system operates by introducing a high volume of air at low pressure, creating a dilute mixture of material and air. The material is then carried through the pipeline by the air flow. This method is particularly suitable for fine powders and granules, as it minimizes material degradation and ensures efficient transport. Our dilute phase systems are optimized for low pressure operation, reducing energy consumption while maintaining high material throughput. The design incorporates efficient air-liquid separation and material recovery mechanisms, ensuring minimal waste and maximum material recovery.
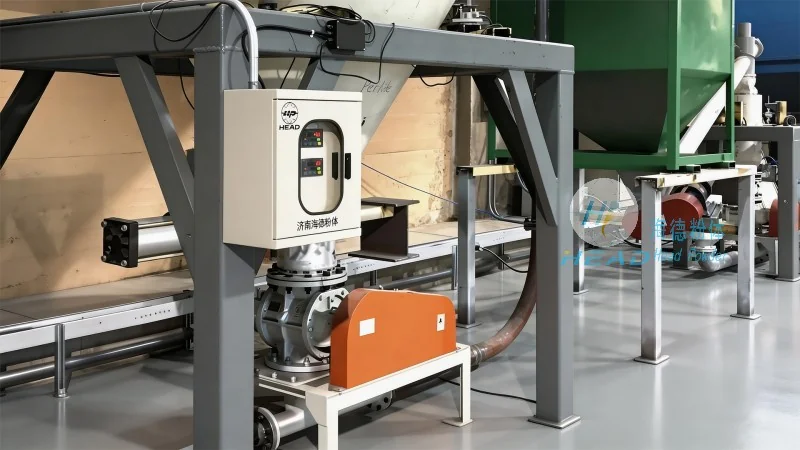
Option 2: Dense Phase Pneumatic Conveying
Dense phase pneumatic conveying is ideal for transporting materials that are sensitive to high air velocities or for longer distances. In this method, the material is conveyed in a dense phase, where the air flow is controlled to maintain a higher material concentration. This approach reduces material attrition and prevents product degradation, making it suitable for delicate or valuable materials. Our dense phase systems utilize controlled air pressure and flow rates to achieve stable material transport. The design includes features such as pulse-jet operation and pressure surge control, which enhance the system's efficiency and reliability. This option is particularly beneficial for applications requiring gentle handling of materials, such as pharmaceuticals or food products.
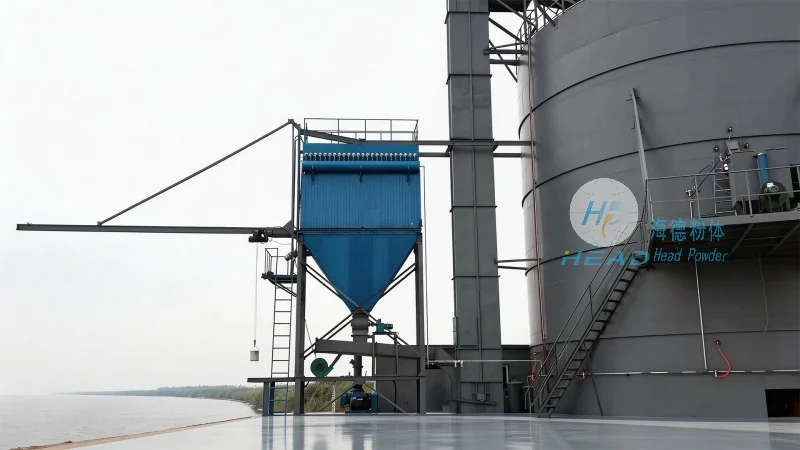
Option 3: Hybrid Pneumatic Conveying Systems
Hybrid pneumatic conveying systems combine the advantages of both dilute and dense phase methods, offering flexibility and adaptability for diverse material handling needs. These systems can switch between dilute and dense phase operation based on the material characteristics and transport requirements. For instance, they may use dilute phase for short distances and dense phase for longer segments, optimizing energy use and material transport efficiency. Our hybrid systems are equipped with advanced control algorithms that monitor material flow and adjust air pressure in real-time, ensuring consistent performance. This approach allows for cost-effective solutions that can handle a wide range of materials, from low to high bulk density, making them suitable for various industrial applications.
Application Examples and Benefits
Our air-powered conveying solutions are widely used in industries such as pharmaceuticals, food processing, chemical manufacturing, and mining. In pharmaceutical applications, the systems ensure sterile and contamination-free transport of raw materials and finished products. In food processing, the gentle handling and hygienic design prevent product spoilage and maintain quality standards. In chemical manufacturing, the robust construction and corrosion resistance of our systems handle aggressive materials without degradation. The benefits of our air-powered conveying systems include reduced labor costs due to automated material transport, lower maintenance requirements compared to mechanical systems, and improved safety through non-contact handling. Additionally, the systems contribute to environmental sustainability by minimizing material waste and reducing the need for manual handling, which can lead to occupational hazards.




