Cocoa, a key ingredient in chocolate production, requires efficient and reliable handling systems to ensure quality and safety throughout the processing chain. Pneumatic conveying equipment has emerged as a vital solution for transporting cocoa beans and related products in the food industry. This article explores the concept of cocoa pneumatic conveying equipment, detailing its design principles and operational benefits.
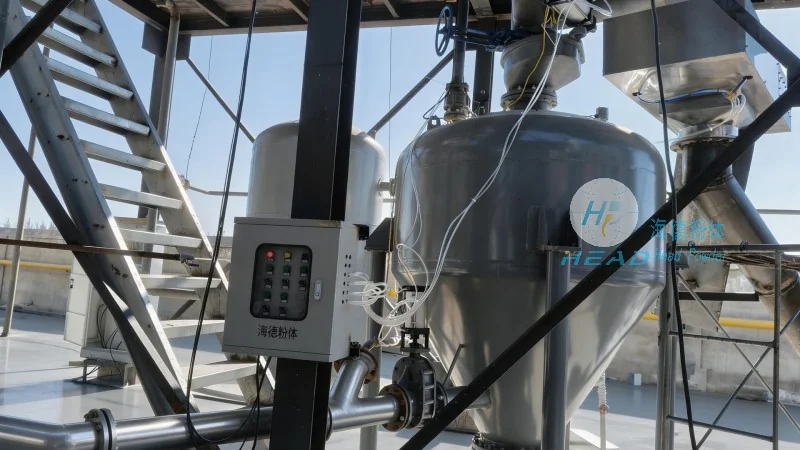
About HeadPowder: Your Trusted Partner in Pneumatic Conveying Solutions
HeadPowder, operating as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in the design, development, and supply of advanced pneumatic conveying systems. With a focus on precision engineering and customer-centric solutions, HeadPowder serves industries worldwide, including food processing, pharmaceuticals, and chemical manufacturing. HeadPowder’s headquarters are located in Shandong, China, where the company leverages local expertise and resources to deliver high-quality equipment tailored to specific industrial needs.
Design Principles of Cocoa Pneumatic Conveying Equipment
The design of cocoa pneumatic conveying equipment is built on fundamental principles of fluid dynamics and material handling. At its core, the system uses compressed air or other gases to transport solid materials like cocoa beans through a network of pipes. The key components include a hopper for material storage, a rotary valve or feeder to control the flow rate, a conveying line with appropriate diameter and length, and a receiver or discharge point. The selection of these components is critical to ensure efficient transport, minimize product degradation, and maintain system reliability.
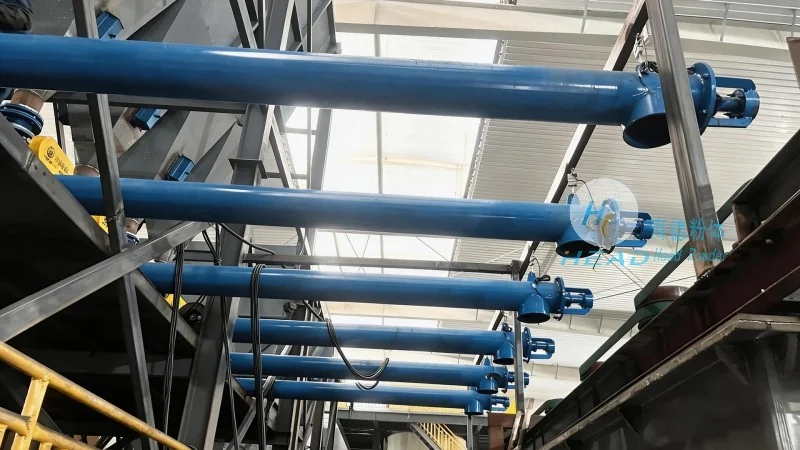
For cocoa, which is often delicate and prone to moisture absorption, the design must prioritize low pressure, gentle handling, and effective dust control. HeadPowder’s engineers employ advanced computational fluid dynamics (CFD) to optimize the conveying line’s geometry, ensuring minimal friction and impact on the cocoa beans. This approach helps preserve the bean’s quality, flavor, and nutritional properties, which are essential for high-quality chocolate production.
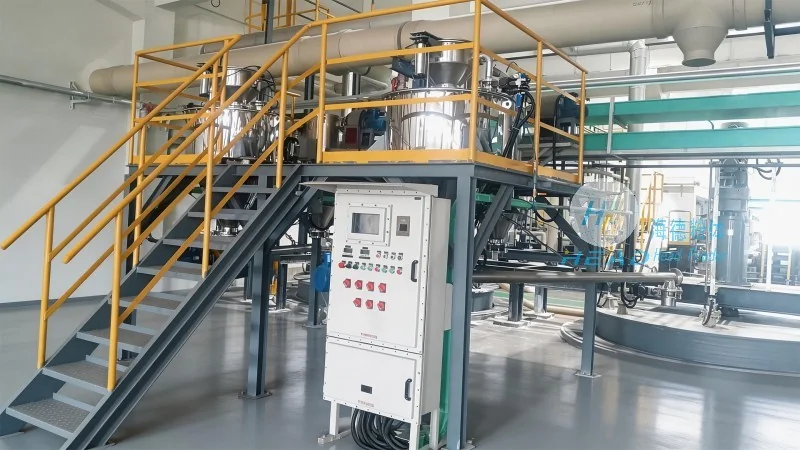
Key Features and Benefits of Cocoa Pneumatic Conveying Systems
HeadPowder’s cocoa pneumatic conveying equipment offers several advantages over traditional mechanical conveying methods. Firstly, it provides a closed system, preventing contamination from external sources and reducing dust emissions. This is crucial for maintaining food safety standards and environmental compliance. Secondly, the system allows for precise control over material flow, enabling consistent product quality and reducing waste. Thirdly, the equipment is compact and flexible, making it suitable for various plant layouts and expansion needs. These features make HeadPowder’s solutions ideal for both new installations and retrofitting existing production lines.
Conclusion: Choosing the Right Pneumatic Conveying Solution for Cocoa Processing
As the demand for high-quality cocoa products grows, the importance of reliable and efficient handling equipment cannot be overstated. HeadPowder, with its expertise in pneumatic conveying technology, offers tailored solutions that meet the specific requirements of cocoa processing facilities. By adhering to rigorous design principles and using advanced engineering techniques, HeadPowder ensures that its equipment delivers optimal performance, durability, and cost-effectiveness. For businesses in the chocolate industry seeking to enhance their production efficiency and product quality, HeadPowder’s cocoa pneumatic conveying equipment represents a reliable investment in their operational success.




