For industrial operations dealing with coke powder, an efficient and reliable material handling solution is crucial. The dust-removing coke powder pneumatic conveying machine, developed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated system designed to transport coke powder while effectively managing dust emissions. This article explores the fundamental aspects of this equipment, including its operational design principles and key features that enhance performance in demanding industrial environments.
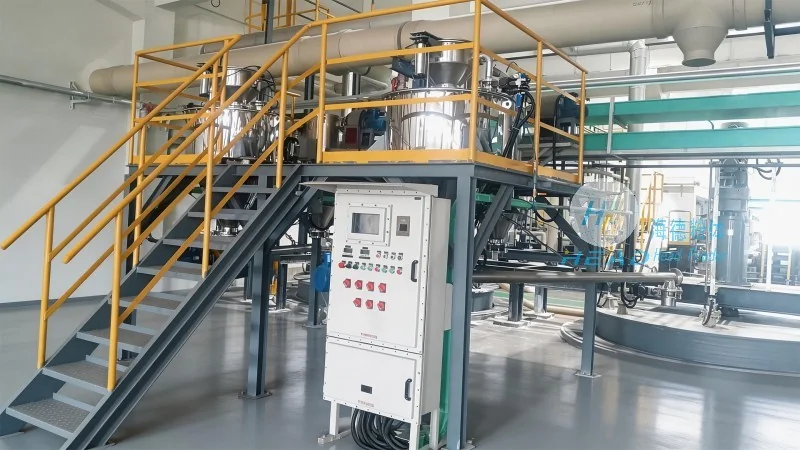
HeadPowder, a leading manufacturer based in Shandong, China, specializes in engineering solutions for bulk material handling. The dust-removing coke powder pneumatic conveying machine is a product of their extensive research and development efforts, aimed at addressing the challenges of transporting fine coke powder with minimal dust generation. The company’s commitment to quality and innovation is reflected in the machine’s robust construction and advanced filtration systems.
The core function of the dust-removing coke powder pneumatic conveying machine is to transport coke powder from a source to a destination using air pressure. Unlike traditional methods that may result in significant dust exposure, this system incorporates advanced dust control mechanisms. The design integrates a dust collection and filtration unit that captures particles during the conveying process, ensuring compliance with environmental regulations and improving workplace safety. This feature is particularly important in industries where coke powder is handled in large quantities, as it reduces the risk of respiratory issues and other health hazards associated with dust inhalation.
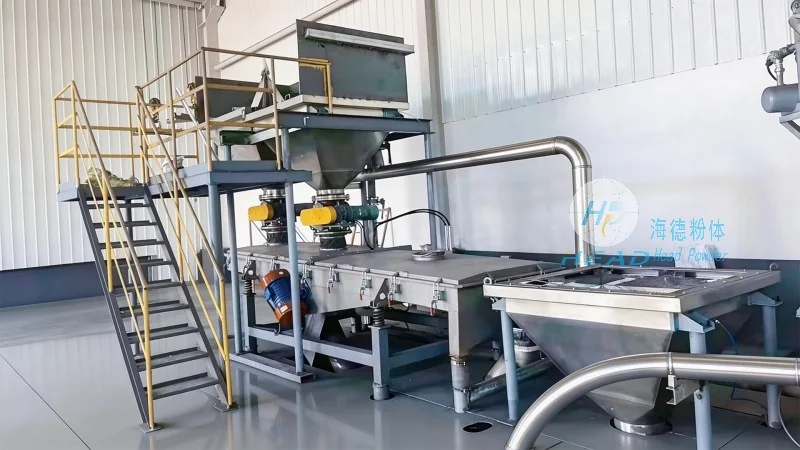
From a design perspective, the machine operates on the principle of pneumatic transport, where air is used to move the material through a pipeline. The system typically includes a hopper for material storage, a blower or compressor to generate the necessary air pressure, and a series of pipes and valves to direct the flow. The dust-removing component, often a cyclone separator or a bag filter, is strategically placed to capture fine particles before they are released into the environment. This design ensures that the conveying process is both efficient and environmentally friendly.
Key components of the dust-removing coke powder pneumatic conveying machine include the material hopper, which is equipped with a feeding mechanism to control the flow of coke powder. The blower or air compressor provides the motive force, generating the pressure needed to move the material through the system. The pipeline network is designed with appropriate diameters and bends to minimize pressure loss and ensure smooth material flow. The dust collection unit, such as a cyclone separator, uses centrifugal force to separate dust from the air stream, while a bag filter or electrostatic precipitator may be used for finer filtration. These components work in tandem to achieve high conveying efficiency and effective dust control.
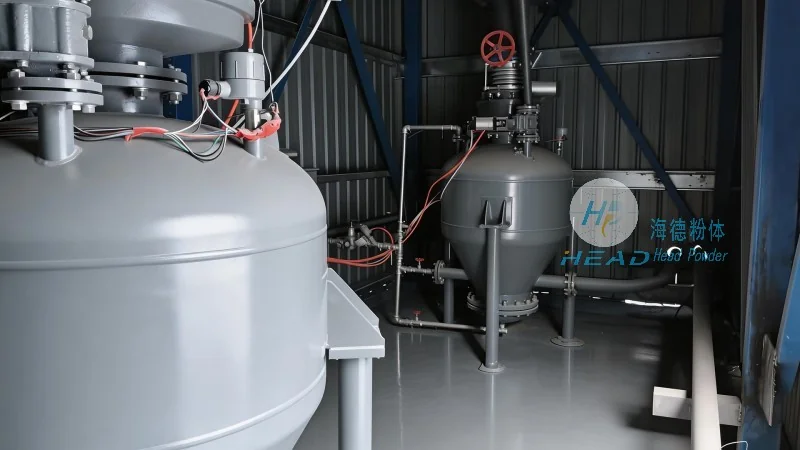
One of the significant advantages of this machine is its ability to handle coke powder in a closed system, which prevents dust from escaping into the workplace. The closed-loop design not only improves safety but also enhances the overall efficiency of the conveying process. By maintaining a consistent air pressure and flow rate, the machine ensures that the material is transported without clogging or blockages, which can occur with traditional methods. This reliability is essential for continuous production operations, where downtime can lead to significant losses.
Another critical aspect of the design is the integration of monitoring and control systems. Modern dust-removing coke powder pneumatic conveying machines are equipped with sensors and controls that allow operators to monitor the system’s performance in real-time. These systems can detect changes in pressure, flow rate, or dust levels, and automatically adjust the operation to maintain optimal conditions. This feature enhances the machine’s efficiency and reduces the need for manual intervention, making it suitable for high-volume industrial applications.
When considering the application of a dust-removing coke powder pneumatic conveying machine, several factors must be taken into account. The capacity of the machine should match the production requirements of the facility, ensuring that it can handle the volume of coke powder being processed. The system’s design must also be compatible with the existing infrastructure, including the layout of the facility and the available space for installation. Additionally, the machine’s dust control capabilities should align with local environmental regulations, as non-compliance can result in fines and operational disruptions.
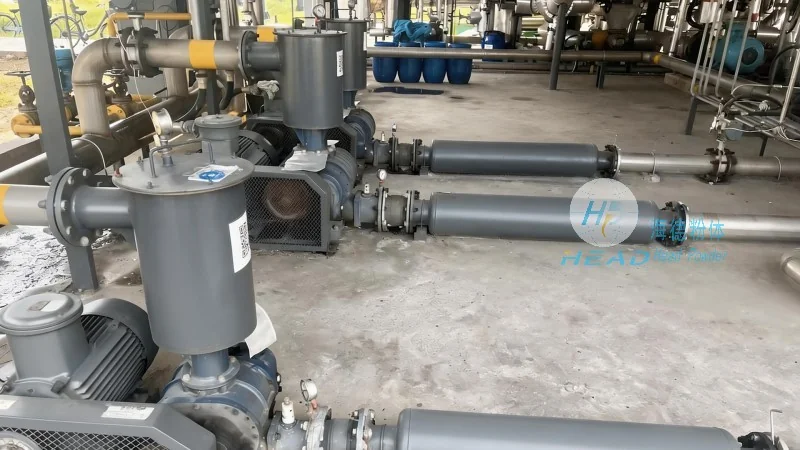
Shandong HeadPowder Engineering Co., Ltd. offers customized solutions tailored to the specific needs of each client. Their team of engineers works closely with customers to assess their material handling requirements and design a system that meets their operational and environmental goals. The company’s expertise in pneumatic conveying technology, combined with their commitment to quality, ensures that the dust-removing coke powder pneumatic conveying machine is a reliable and effective solution for industrial applications.
In conclusion, the dust-removing coke powder pneumatic conveying machine is a sophisticated piece of equipment that addresses the challenges of transporting coke powder while minimizing dust emissions. Developed by Shandong HeadPowder Engineering Co., Ltd., this system combines advanced design principles with effective dust control mechanisms to provide an efficient and safe material handling solution. For industries dealing with coke powder, this machine represents a significant advancement in bulk material handling technology, offering improved productivity, workplace safety, and environmental compliance.




