For industrial operations in the fertilizer sector, efficient material handling is crucial to maintaining productivity and ensuring consistent quality. Among the various methods available, pneumatic conveying stands out as a versatile and effective solution for transporting granular fertilizers. This article delves into the concept of fertilizer granule pneumatic conveying, exploring the fundamental principles behind this powder handling system and how it enhances operational efficiency.
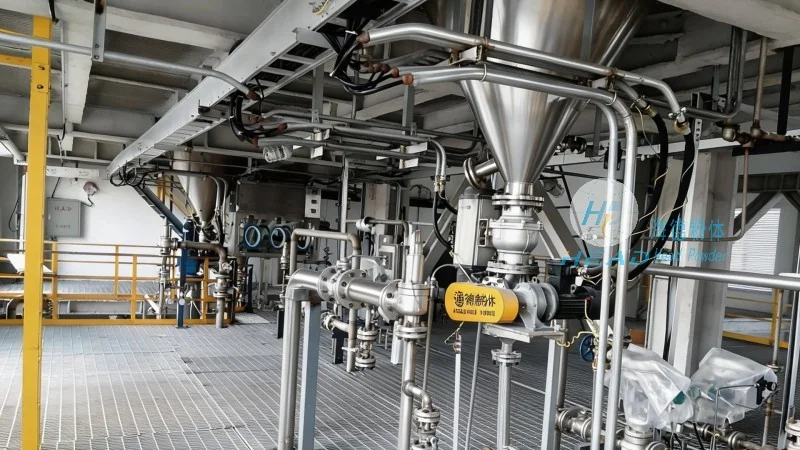
Understanding Pneumatic Conveying Systems
Pneumatic conveying, also known as powder handling systems, utilizes air or gas to transport bulk materials like fertilizer granules through a pipeline network. The system operates by creating a pressure differential, either through suction (negative pressure) or pressure (positive pressure), to move the material from the source to the destination. This method eliminates the need for mechanical components such as belts, buckets, or screw conveyors, reducing maintenance costs and minimizing the risk of material contamination.
The Working Principle of Fertilizer Granule Pneumatic Conveying
The core of the fertilizer granule pneumatic conveying system involves several key components and processes. At the source, the fertilizer granules are introduced into a hopper or feeder, where they are then fed into the conveying line. A fan or blower generates the necessary airflow, which is directed through the pipeline. As the air flows, it entrains the granules, creating a slurry-like mixture that travels through the system. The velocity of the air is carefully controlled to ensure the granules are carried without excessive wear or degradation. The system may include features such as cyclones or filters to separate the air from the material at the destination, allowing for clean material discharge and air recycling.
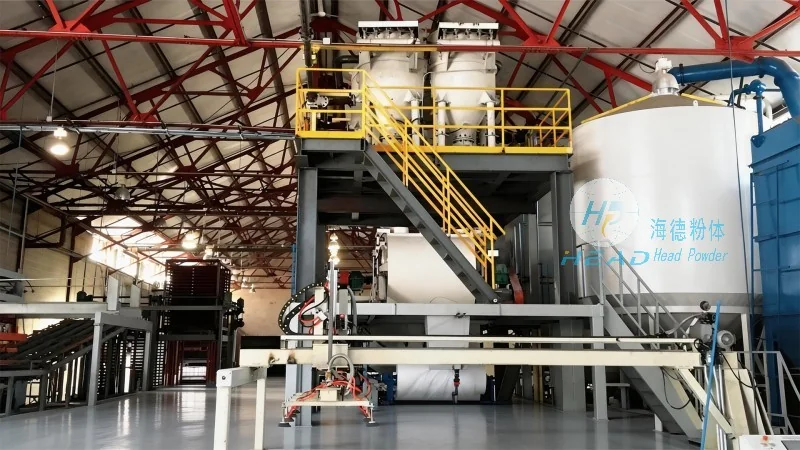
Key Advantages of Pneumatic Conveying for Fertilizer Transport
Implementing a pneumatic conveying system for fertilizer granules offers numerous benefits. Firstly, it provides a dust-free and hygienic environment, which is essential for maintaining product quality and adhering to regulatory standards. Secondly, the system is highly flexible, capable of transporting materials over long distances and through complex layouts without the need for multiple transfer points. Additionally, it reduces labor costs by automating the material handling process and minimizes the risk of product breakage or segregation. The efficiency of the system also contributes to lower energy consumption compared to traditional methods, making it a cost-effective solution for large-scale fertilizer operations.
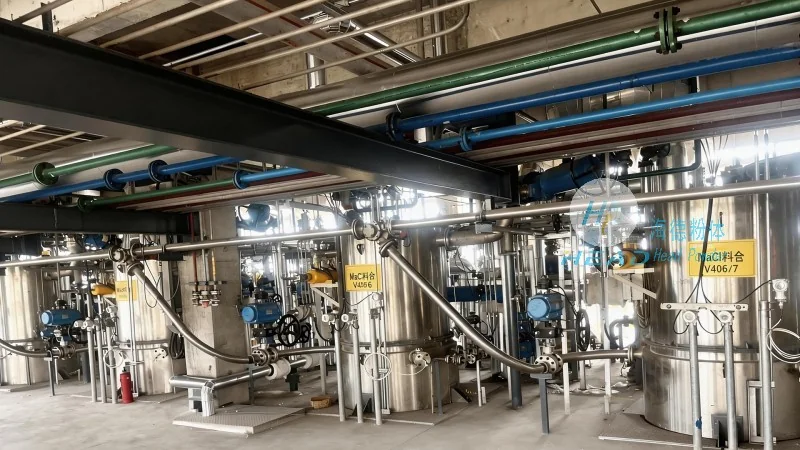
HeadPowder Engineering Co., Ltd. - Experts in Powder Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of customized powder handling systems tailored to the fertilizer industry. With a focus on innovation and precision engineering, HeadPowder designs and manufactures pneumatic conveying solutions that meet the unique demands of fertilizer manufacturers. The company’s expertise lies in optimizing material flow, ensuring consistent product quality, and enhancing overall operational efficiency. HeadPowder’s systems are built to withstand the harsh conditions of fertilizer processing, including high temperatures, moisture, and abrasive materials, while maintaining durability and reliability. By partnering with HeadPowder, fertilizer producers can achieve seamless material transport, reduce downtime, and improve their bottom line.
Conclusion
Fertilizer granule pneumatic conveying represents a sophisticated and efficient approach to powder handling in the agricultural sector. By leveraging the principles of pneumatic transport, this system enables smooth, dust-free, and reliable movement of granular fertilizers, supporting the productivity and sustainability of modern farming operations. As the demand for efficient fertilizer production and distribution grows, companies like HeadPowder continue to play a vital role in delivering advanced powder handling solutions that meet the evolving needs of the industry.




