For industries dealing with silicate materials, efficient and reliable material handling is crucial. Silicate pneumatic conveying equipment plays a vital role in transporting these materials from one location to another with precision and minimal loss. This equipment is designed to handle the unique properties of silicate materials, ensuring smooth operation and optimal performance in various industrial applications.
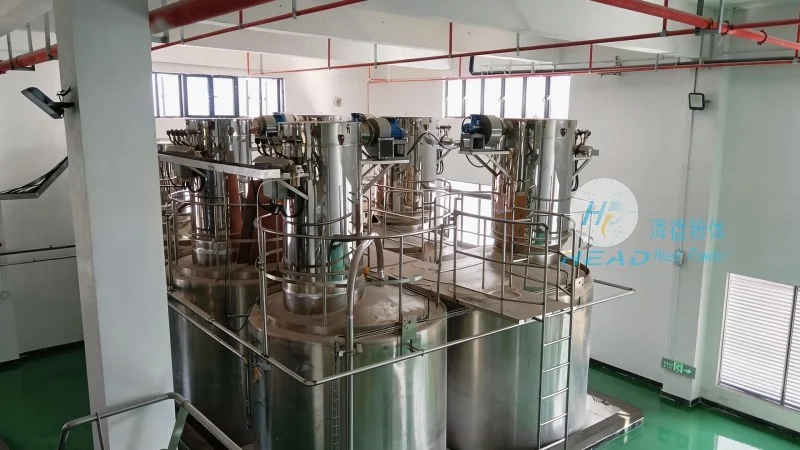
Key Components and Structure of Silicate Pneumatic Conveying Equipment
The core structure of silicate pneumatic conveying equipment consists of several essential components that work in harmony to achieve effective material transport. The primary components include the hopper, which serves as the material storage and feeding unit; the conveying pipeline, which is responsible for transporting the material through the system; the air supply system, which provides the necessary airflow to move the material; and the control system, which regulates the operation of the entire conveying process. Each component is carefully engineered to handle the specific characteristics of silicate materials, such as their particle size, density, and flowability.
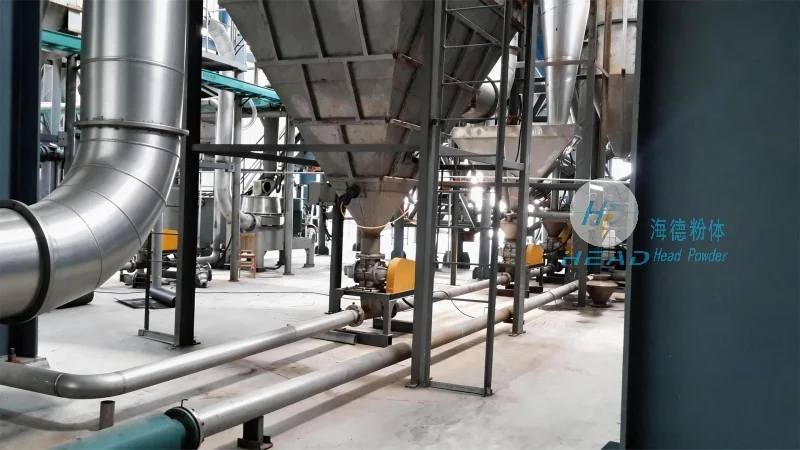
Working Principle of Silicate Pneumatic Conveying Equipment
The operation of silicate pneumatic conveying equipment is based on the principle of pneumatic transport, where material is conveyed through a pipeline using compressed air. The process typically begins with the material being fed into the hopper. From there, the material is drawn into the conveying pipeline by the airflow generated by the air supply system. The air flow, often referred to as the conveying air, creates a low-pressure zone in the pipeline, which pulls the material along with it. The control system ensures that the airflow and material feed are synchronized to maintain a consistent conveying rate. This method allows for the efficient transport of silicate materials over long distances without the need for mechanical components like belts or chains, reducing maintenance and operational costs.
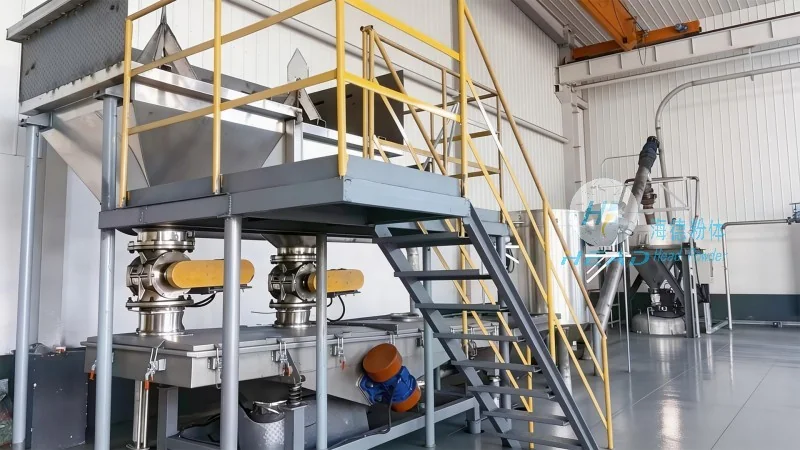
Advantages of Using Silicate Pneumatic Conveying Equipment
Implementing silicate pneumatic conveying equipment offers numerous advantages for industrial operations. One of the key benefits is the ability to handle a wide range of silicate materials, including powders, granules, and fine particles. The equipment is designed to minimize material degradation and loss during transport, which is critical for maintaining product quality. Additionally, the system is highly flexible, allowing for easy integration into existing production lines and the ability to transport materials to multiple destinations from a single source. The absence of moving parts in the conveying pipeline reduces the risk of mechanical failure and lowers maintenance requirements, leading to increased operational reliability and cost savings over time.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of advanced material handling solutions. With a focus on innovation and quality, the company specializes in developing and supplying silicate pneumatic conveying equipment tailored to the needs of various industries. Headpowder's commitment to excellence is reflected in their rigorous design and manufacturing processes, ensuring that each piece of equipment meets the highest standards of performance and durability. The company's headquarters is located in Shandong, China, where they leverage local expertise and resources to deliver cutting-edge solutions to clients worldwide.
Conclusion
Silicate pneumatic conveying equipment is an indispensable tool for industries that rely on the efficient transport of silicate materials. By understanding its structure, working principles, and advantages, businesses can make informed decisions about implementing this technology to enhance their operational efficiency and product quality. With the support of companies like Shandong HeadPowder Engineering Co., Ltd., industries can access reliable and effective solutions that meet their specific material handling requirements.




