HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced capsule pneumatic conveying systems. This equipment is engineered to efficiently transport bulk materials through a pressurized air system, offering a reliable solution for various industrial applications. The capsule pneumatic conveying system is particularly suitable for handling powders, granules, and other particulate materials, ensuring minimal product degradation and consistent flow rates.
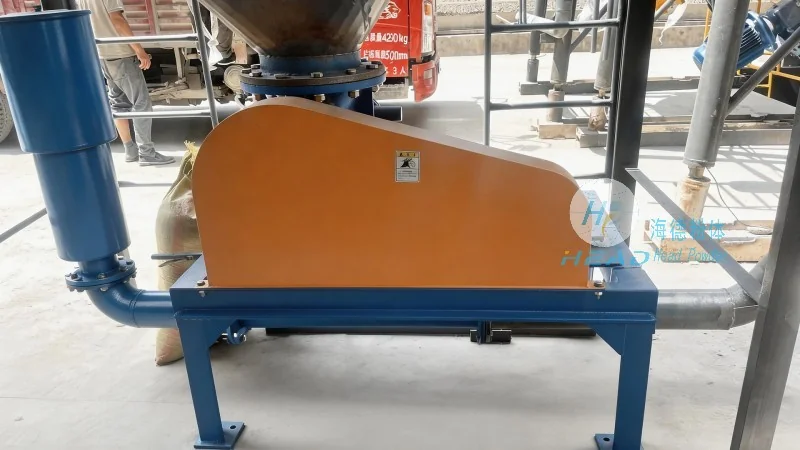
Overview of Capsule Pneumatic Conveying System Equipment
The capsule pneumatic conveying system, also known as a pneumatic conveyor, utilizes a series of capsules or flexible tubes to move materials from a source to a destination. This technology is widely adopted in industries such as food processing, pharmaceuticals, chemicals, and manufacturing due to its ability to handle sensitive materials without contamination. The equipment is designed to maintain product integrity, reduce dust generation, and improve operational efficiency compared to traditional mechanical conveying methods.
Structural Principles of the Capsule Pneumatic Conveying System
The core components of the capsule pneumatic conveying system include the material hopper, air compressor, conveying line, and discharge hopper. The material is fed into the hopper, where it is then drawn into the conveying line by the pressurized air generated by the compressor. The capsules, which are flexible and expandable, ensure a smooth and consistent flow of material through the system. The system operates on the principle of differential pressure, where the air pressure is maintained above atmospheric pressure to create a positive pressure environment for material transport.
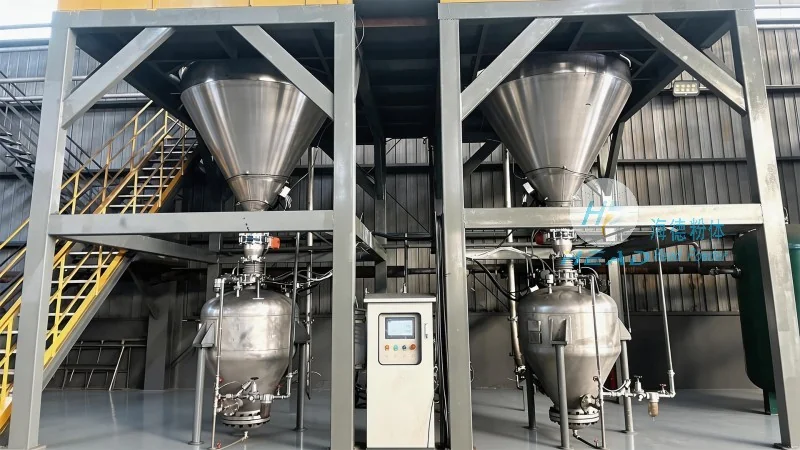
Key Features and Advantages
HeadPowder's capsule pneumatic conveying systems are equipped with several key features that enhance performance and reliability. These include adjustable air pressure controls, which allow for precise control over material flow rates, and flexible conveying lines that can be customized to fit specific plant layouts. The system also offers low maintenance requirements, as the capsules are durable and resistant to wear and tear. Additionally, the equipment is designed to minimize product contamination, making it ideal for applications where hygiene and product purity are critical.
Applications in Industrial Settings
The capsule pneumatic conveying system is versatile and can be applied in a wide range of industrial processes. In the food industry, it is used to transport ingredients like flour, sugar, and spices without cross-contamination. In the pharmaceutical sector, it is employed to handle active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring compliance with regulatory standards. The system is also utilized in chemical manufacturing to transport powders and granules, reducing the risk of dust explosions and improving workplace safety.
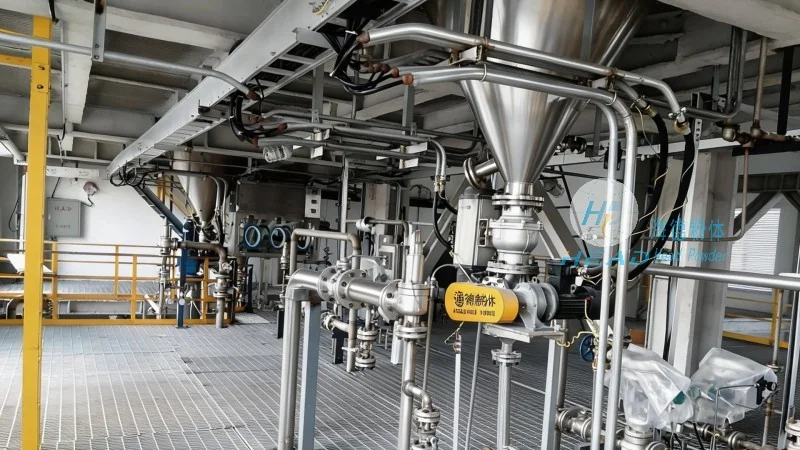
Installation and Maintenance Considerations
Proper installation and regular maintenance are essential for the optimal performance of the capsule pneumatic conveying system. HeadPowder provides comprehensive installation services, ensuring that the equipment is set up according to industry best practices. Regular maintenance includes checking air compressor performance, inspecting conveying lines for any signs of wear, and cleaning the material hopper and discharge hopper to prevent material buildup. By adhering to a regular maintenance schedule, users can extend the lifespan of the equipment and minimize downtime.
Conclusion
HeadPowder's capsule pneumatic conveying system equipment offers a superior solution for bulk material handling in various industrial applications. With its advanced structural design and reliable performance, the system ensures efficient, safe, and hygienic material transport. As a trusted manufacturer based in Shandong, China, HeadPowder continues to innovate and provide high-quality equipment that meets the evolving needs of the industry. The capsule pneumatic conveying system is an investment in operational efficiency and product quality, making it a valuable asset for any industrial facility.




