Coal powder pneumatic conveying systems are essential in industrial applications for transporting coal powder efficiently. These systems utilize air as the medium to move coal powder from one location to another, offering advantages such as low maintenance, flexible layout, and the ability to handle fine powders. The classification and application of these systems are critical for optimizing industrial processes and ensuring reliable material transport.
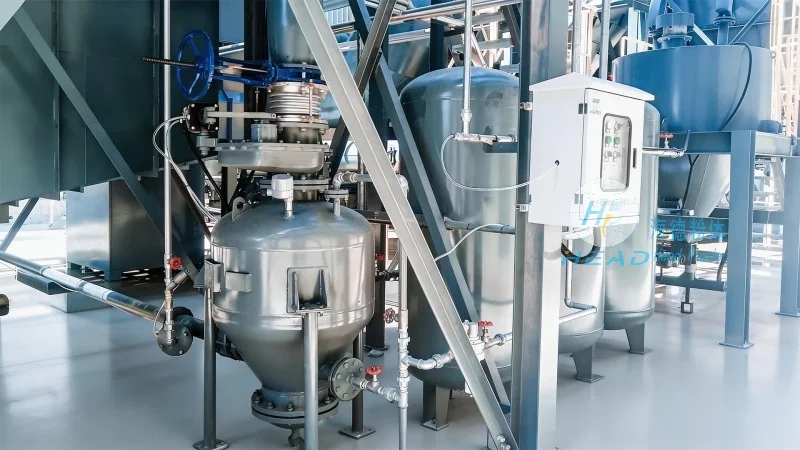
Classification of Coal Powder Pneumatic Conveying Systems
Coal powder pneumatic conveying systems can be broadly classified into two main categories: dilute-phase and dense-phase systems. Dilute-phase systems, also known as pneumatic conveying, operate by suspending coal powder particles in a high-velocity air stream. This method is suitable for long-distance transport and handling large volumes of material. Dense-phase systems, on the other hand, use lower air velocities and higher pressure to transport coal powder in a more concentrated form, reducing the risk of particle degradation and ensuring better control over material flow.
Key Components of Coal Powder Pneumatic Conveying Systems
The core components of a coal powder pneumatic conveying system include the material feed hopper, the conveying line (usually a pipeline), the air supply system (including a blower or compressor), and the control valves. The feed hopper ensures a consistent supply of coal powder, while the conveying line transports the material. The air supply system generates the necessary airflow to move the coal powder, and control valves regulate the pressure and flow within the system. Additionally, dust collection and filtration systems are often included to maintain air quality and comply with environmental regulations.
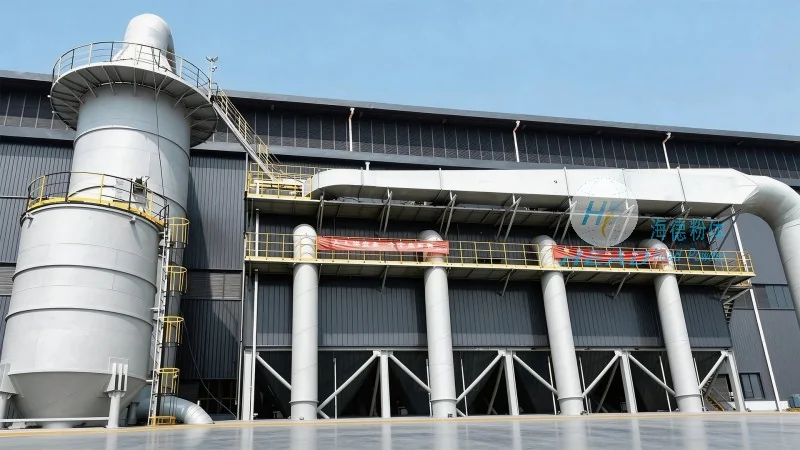
Applications of Coal Powder Pneumatic Conveying Systems
Coal powder pneumatic conveying systems are widely used in various industries, including power generation, cement production, and chemical processing. In power plants, these systems are crucial for transporting coal from storage silos to boilers, ensuring a continuous and efficient fuel supply. In cement plants, they help transport raw materials and finished products, improving production line efficiency. The systems are also employed in chemical industries for handling coal-based raw materials, contributing to streamlined manufacturing processes.
Advantages and Considerations in Coal Powder Pneumatic Conveying
One of the primary advantages of coal powder pneumatic conveying systems is their ability to handle fine and abrasive materials without causing significant wear and tear on equipment. This makes them ideal for applications involving coal powder, which can be abrasive and prone to caking. However, the systems require careful design and maintenance to prevent blockages and ensure consistent performance. Factors such as particle size, moisture content, and the distance of transport must be considered when selecting the appropriate system type and components.
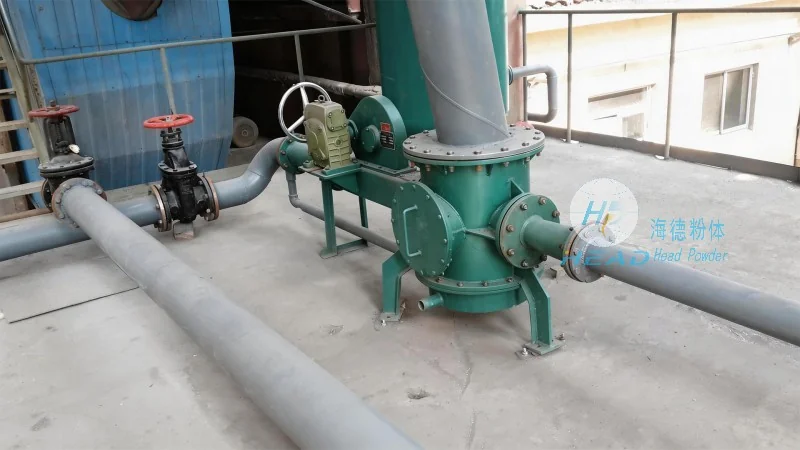
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of coal powder pneumatic conveying systems. With a focus on providing reliable and efficient solutions, the company serves a wide range of industrial sectors. HeadPowder's expertise lies in customizing systems to meet specific client requirements, ensuring optimal performance and durability. The company is committed to delivering high-quality equipment and services, supporting industrial operations with advanced material handling technologies.
Conclusion
Coal powder pneumatic conveying systems play a vital role in modern industrial operations, offering efficient and flexible solutions for transporting coal powder. By understanding the classification and application of these systems, industries can optimize their processes and enhance productivity. Shandong HeadPowder Engineering Co., Ltd. continues to be a key player in providing advanced pneumatic conveying solutions, supporting clients in achieving their operational goals with reliable and innovative equipment.




