Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for the efficient transport of coke particles over long distances. With a focus on reliability and performance, our systems are engineered to meet the demanding requirements of modern industrial applications, ensuring minimal product degradation and optimal operational efficiency.
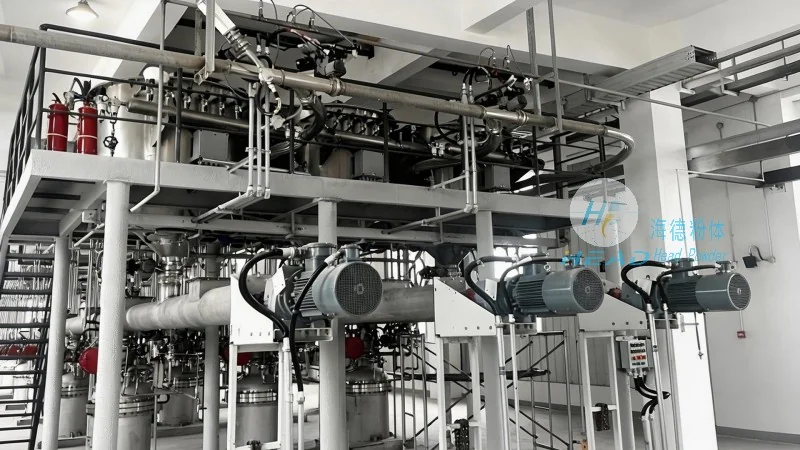
System Overview and Core Components
Our long - distance pneumatic conveying system for coke particles is a sophisticated solution that integrates multiple key components to achieve seamless material transport. The system typically comprises a feed hopper, a rotary airlock valve, a positive displacement blower or a high - pressure air compressor, a pipeline network, and a receiver or discharge unit. Each component is carefully selected and configured to handle the unique characteristics of coke particles, such as their size, density, and abrasiveness, ensuring a stable and consistent conveying process.
Advantages of the Pneumatic Conveying System
Implementing a long - distance pneumatic conveying system for coke particles offers several significant advantages over traditional methods like belt conveyors or bucket elevators. Firstly, it eliminates the need for multiple transfer points and intermediate storage, reducing the risk of material contamination and loss. Secondly, the system provides a dust - free and enclosed transport environment, which is crucial for maintaining product quality and ensuring workplace safety. Additionally, the flexibility of pneumatic conveying allows for easy integration with existing production lines and the ability to adjust conveying rates according to operational needs.
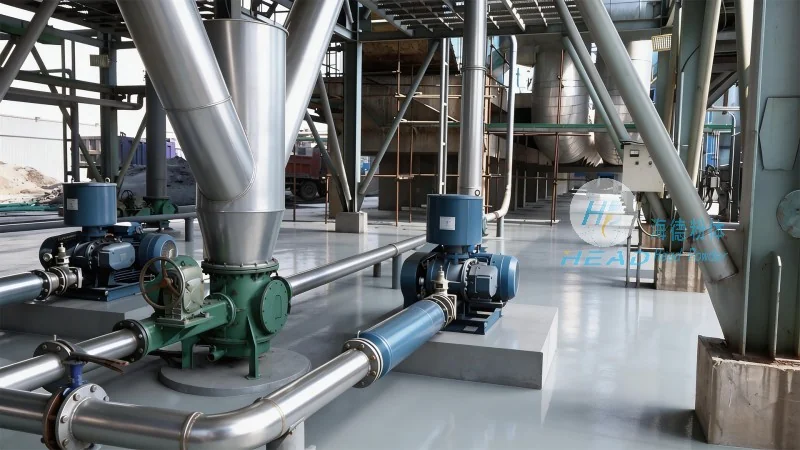
Technical Specifications and Performance Metrics
The performance of our long - distance pneumatic conveying system for coke particles is defined by several critical technical specifications. The system is capable of conveying coke particles over distances ranging from several hundred meters to several kilometers, depending on the specific design and application requirements. The conveying capacity can be adjusted to handle varying particle loads, with typical capacities ranging from a few tons per hour to over 100 tons per hour. The system operates under positive pressure, which helps prevent air leakage and maintains a consistent flow of material through the pipeline. The use of high - quality materials, such as stainless steel for the pipeline and wear - resistant components for the airlock and blower, ensures long service life and minimal maintenance.
Application Scenarios and Industry Integration
Our long - distance pneumatic conveying system for coke particles is widely used in various industrial sectors, including steel production, cement manufacturing, and chemical processing. In steel plants, the system is used to transport coke from storage silos to blast furnaces, ensuring a continuous and reliable supply of raw materials. In cement plants, it facilitates the transport of coke from the coke oven to the clinker production line, optimizing the overall production process. The system's adaptability makes it suitable for both new plant installations and retrofits of existing facilities, providing a cost - effective solution for improving material handling efficiency.
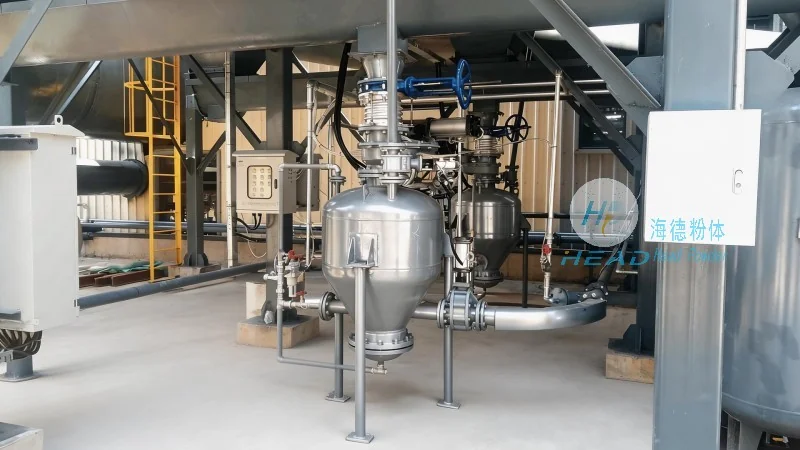
Installation and Maintenance Considerations
The successful implementation of the long - distance pneumatic conveying system for coke particles requires careful planning and professional installation. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive installation services, including site assessment, system design, and on - site commissioning. Regular maintenance is essential to ensure the system's long - term performance and reliability. This includes routine checks of the blower or compressor, inspection of the pipeline for wear or damage, and replacement of wear - resistant parts as needed. Our team of experienced technicians is available to provide maintenance support and troubleshooting services, minimizing downtime and maximizing the system's operational efficiency.
Customer Testimonials and Case Studies
Many customers have benefited from the implementation of our long - distance pneumatic conveying system for coke particles. For example, a major steel manufacturer in China reported a 20% reduction in material handling costs after upgrading to our system, along with improved product quality and reduced workplace dust levels. Another client, a cement producer, achieved a 15% increase in production throughput by integrating our system into their existing operations. These success stories highlight the effectiveness and reliability of our solutions, making us a trusted partner for industrial material handling needs.




