HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced air-pneumatic conveying systems tailored for the efficient bulk transport of aggregate materials such as sand, gravel, and crushed stone. These systems represent a critical solution in modern construction and mining operations, offering a reliable alternative to traditional mechanical conveying methods. The following overview details the key applications, technical advantages, and practical considerations associated with air-pneumatic conveying in the aggregate industry.
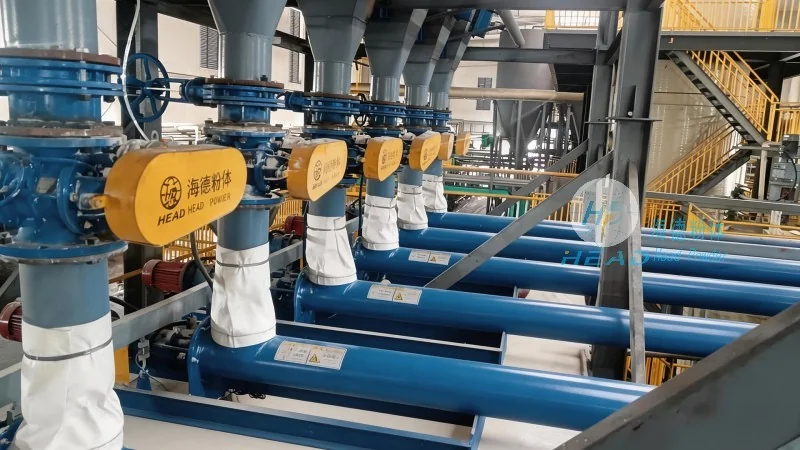
Key Advantages of Air-Pneumatic Conveying for Aggregate Materials
When compared to conventional belt or bucket elevators, air-pneumatic conveying systems provide several distinct benefits that enhance operational efficiency and material handling capabilities. Firstly, these systems eliminate the need for multiple transfer points and intermediate storage, reducing the risk of material degradation and contamination. Secondly, they offer superior flexibility in terms of layout and installation, allowing for complex routing and integration with existing processing lines. Thirdly, air-pneumatic conveyors are highly effective in handling abrasive and dusty materials like sand and gravel, minimizing wear on components and extending equipment lifespan. Additionally, these systems can operate in a closed-loop environment, significantly reducing dust emissions and improving workplace safety. For companies in the aggregate sector, these advantages translate into lower maintenance costs, higher throughput, and improved overall productivity.
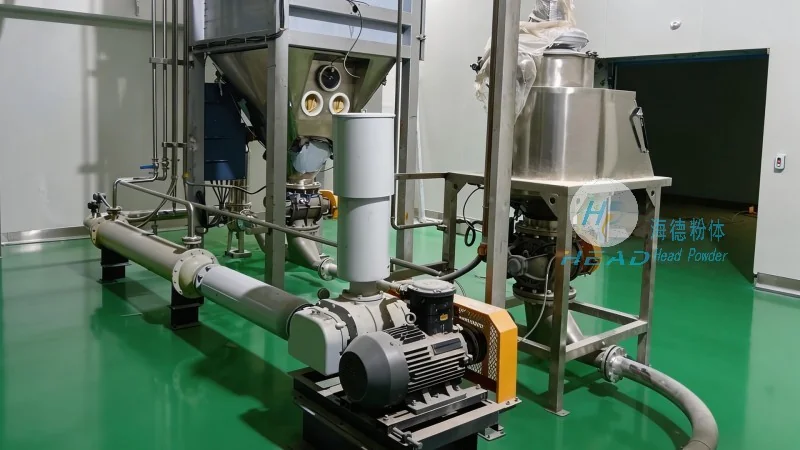
Technical Components and Operational Principles
The core components of an air-pneumatic conveying system for aggregate materials include a material feed hopper, a pneumatic conveyor line (typically made of stainless steel or high-density polyethylene to withstand abrasion), a control valve system, and a dust collection or filtration unit. The operation involves feeding the aggregate material into the hopper, where it is then drawn into the conveyor line by a vacuum or pressure source. The material is transported through the pipeline by a combination of air velocity and material density, with the system maintaining consistent flow rates through precise control of air pressure and material feed rates. HeadPowder engineers utilize advanced computational fluid dynamics (CFD) and material flow analysis to optimize system design, ensuring that the conveyor line dimensions, air flow rates, and pressure differentials are precisely matched to the specific characteristics of the aggregate being handled. This engineering approach minimizes energy consumption while maximizing material throughput, making the system both cost-effective and environmentally friendly.
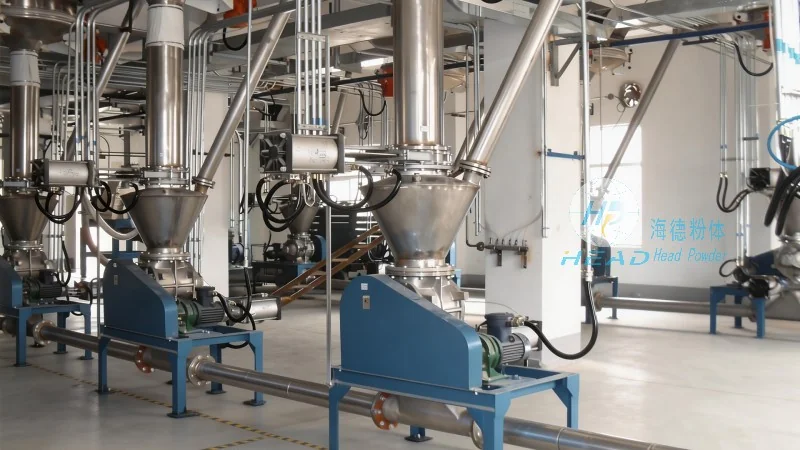
Application Scenarios and Industry Integration
Air-pneumatic conveying systems are widely applied in various stages of aggregate processing and distribution. In mining operations, these systems are used to transport raw crushed stone from the quarry to processing facilities, where the material is sorted and sized. In construction sites, they efficiently move sand and gravel to mixing plants or storage silos, ensuring a continuous supply of raw materials for concrete production. Additionally, in recycling and waste management facilities, air-pneumatic conveyors are employed to transport recycled aggregates, reducing the need for manual handling and improving material purity. HeadPowder’s solutions are designed to integrate seamlessly with existing infrastructure, whether in new construction projects or retrofits of existing plants. The company’s team of experienced engineers works closely with clients to assess their specific operational needs, from initial material analysis to final system commissioning, ensuring that the air-pneumatic conveying system meets all performance and safety standards.
Maintenance and Longevity Considerations
Proper maintenance is crucial to the long-term performance and reliability of air-pneumatic conveying systems. HeadPowder emphasizes regular inspection of conveyor line integrity, control valve functionality, and dust filtration systems. Abrasive materials like sand and gravel can cause wear on the conveyor line and internal components, so periodic replacement of wear-resistant liners and seals is recommended. The company also recommends implementing a preventive maintenance schedule that includes cleaning of the material feed hopper and conveyor line to prevent blockages and ensure consistent material flow. By adhering to these maintenance practices, aggregate processing facilities can extend the operational life of their air-pneumatic conveying systems, reducing downtime and maintenance costs over time. HeadPowder provides comprehensive after-sales support, including technical guidance and spare parts availability, to assist clients in maintaining optimal system performance.
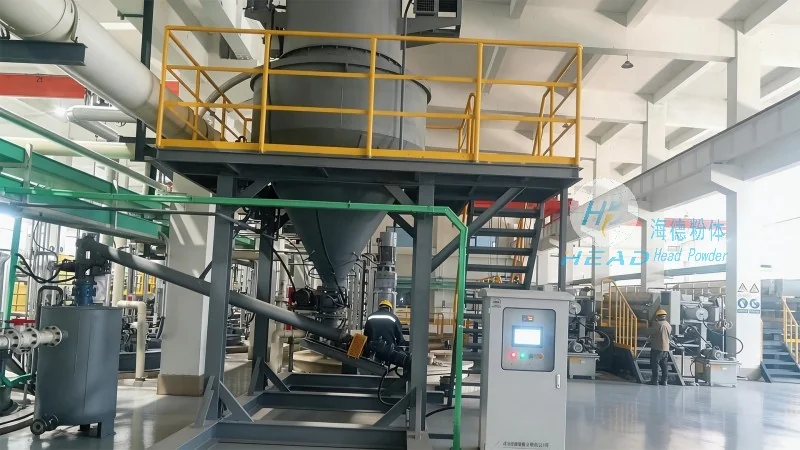
Conclusion and Future Outlook
For the aggregate industry, air-pneumatic conveying systems represent a sophisticated and efficient solution for bulk material transport. HeadPowder’s expertise in designing and implementing these systems ensures that clients receive tailored solutions that meet their specific operational requirements. By leveraging advanced engineering principles and high-quality components, HeadPowder delivers systems that enhance productivity, improve safety, and reduce operational costs. As the demand for efficient material handling in construction and mining continues to grow, air-pneumatic conveying technology will remain a critical component in the industry’s technological advancement. HeadPowder remains committed to providing innovative solutions that support the sustainable and efficient operation of aggregate processing facilities worldwide.




