Fluorspar powder, a vital industrial mineral, demands efficient handling and transportation across various processing stages. The pneumatic conveying system represents a widely adopted technology for moving fluorspar powder from source to destination. This article provides an overview of the classification and key components of fluorspar powder pneumatic conveying systems, highlighting technical specifications and practical applications.
Introduction to Fluorspar Powder Pneumatic Conveying
Fluorspar, or fluorite, primarily consists of calcium fluoride (CaF₂) and is extensively used in producing hydrofluoric acid, aluminum fluoride, and other chemical products. Due to its fine particle size and dusty nature, traditional handling methods like bucket elevators or belt conveyors may be unsuitable. Pneumatic conveying systems utilize air or gas to transport the powder through a pipeline network, ensuring safe and efficient material transfer.
Classification of Fluorspar Powder Pneumatic Conveying Systems
Fluorspar powder pneumatic conveying systems are broadly classified into two main categories based on system pressure: positive pressure systems and negative pressure (vacuum) systems. Each type has distinct characteristics suited to different operational needs.
Positive Pressure Systems
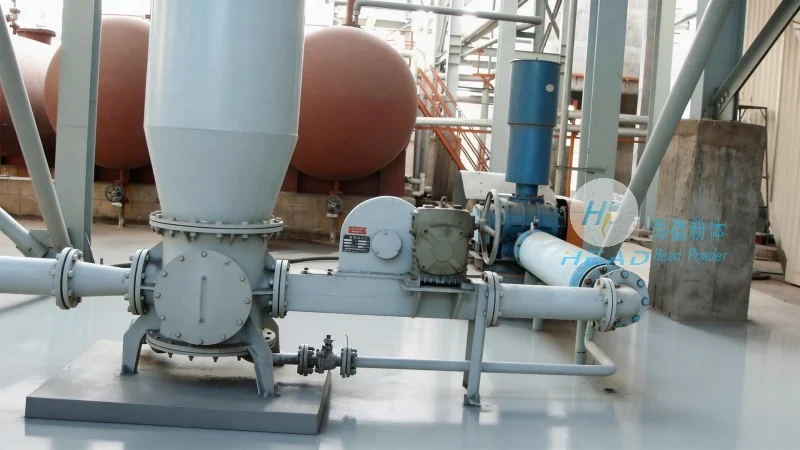
In positive pressure systems, conveying air is supplied under pressure, typically via a positive displacement blower or centrifugal fan. Air is introduced at the material loading point, maintaining pressure throughout the pipeline to propel the powder forward. This type is preferred for high-distance conveying or when delivering material to multiple destinations from a single source.
Negative Pressure (Vacuum) Systems
Negative pressure systems operate by creating a vacuum in the pipeline, drawing fluorspar powder from the source. A vacuum pump or fan generates the low-pressure environment, with suction force transporting the powder. These systems are commonly used for short to medium distances and when collecting material from multiple points to a central processing unit.
Key Components of Fluorspar Powder Pneumatic Conveying Systems
The effectiveness of a fluorspar powder pneumatic conveying system depends on the integration of critical components, each with a specific role in ensuring efficient and safe operation.
1. Material Loading Hopper and Feeder
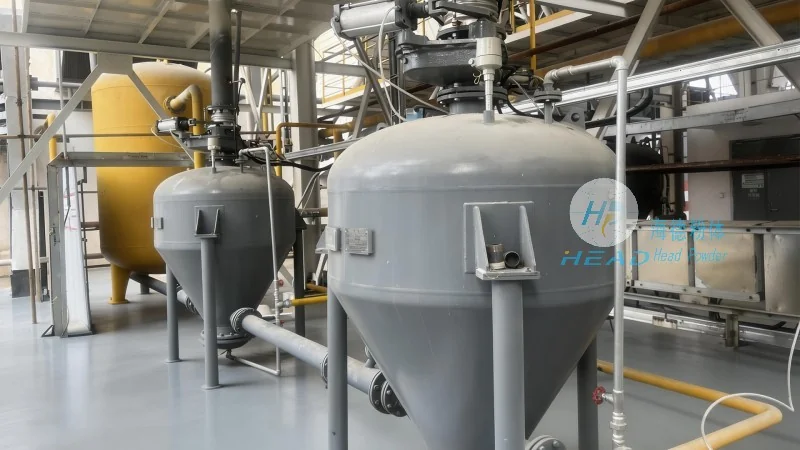
The material loading hopper serves as the initial point where fluorspar powder is introduced. It stores the powder and provides controlled feed to the conveying line. The feeder—often a rotary valve or screw feeder—regulates flow rate, preventing overloading and ensuring consistent material delivery. This component is vital for maintaining system performance and avoiding blockages.
2. Conveying Air Supply Unit
The air supply unit provides the necessary air or gas to move fluorspar powder through the pipeline. In positive pressure systems, a positive displacement blower or high-pressure centrifugal fan generates required pressure. In negative pressure systems, a vacuum pump creates suction. The unit must handle fluorspar's particle size, density, and moisture content to ensure efficient conveying.
3. Conveying Pipeline and Fittings
The pipeline is the main pathway for transporting powder and air, typically made of stainless steel, PVC, or plastic for chemical compatibility and system pressure. It includes fittings like elbows, tees, and reducers to direct flow and maintain integrity. Proper design minimizes pressure losses and prevents material deposition or blockages.
4. Air Separation and Cleaning System
At the receiving end, an air separation and cleaning system separates fluorspar powder from conveying air. This typically includes a cyclone separator and bag filter. The cyclone uses centrifugal force to separate larger particles, while the bag filter captures fine dust. The separated powder is collected in a receiving hopper, and clean air is discharged or recirculated. This component ensures product quality and environmental compliance.
5. Control and Monitoring Equipment
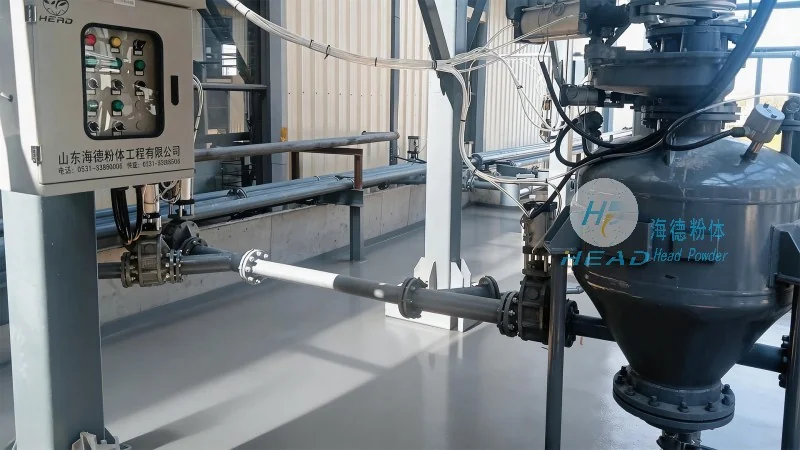
Modern systems include control and monitoring equipment for optimal operation. Pressure sensors, flow meters, and control valves regulate air supply and material feed. Integrated with PLCs or computer systems, this allows automated operation and real-time parameter monitoring. It helps maintain consistent performance, detect faults, and prevent system failures.
Applications and Benefits of Fluorspar Powder Pneumatic Conveying Systems
Fluorspar powder pneumatic conveying systems are widely used in chemical manufacturing, metallurgy, and mining. They offer benefits like improved safety (eliminating manual dusty handling), increased efficiency (reducing material loss and downtime), and flexibility in material transportation. Systems can be customized for long-distance conveying or large volume handling.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of pneumatic conveying systems, specializes in customized fluorspar powder handling solutions. With years of industry experience, the company provides high-quality systems tailored to client needs. Its systems are known for reliability, efficiency, and durability, making it a preferred choice for fluorspar powder industries.
Located in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. leverages advanced technology and engineering expertise to develop innovative pneumatic conveying solutions. The company's commitment to quality and customer satisfaction has established a strong market reputation. By offering comprehensive support—including design, installation, and maintenance—the company ensures clients operate fluorspar powder pneumatic conveying systems efficiently and effectively.




