When it comes to selecting a manufacturer for fertilizer granule pneumatic conveying systems, businesses in the agricultural and chemical sectors face a critical decision. The choice of manufacturer directly impacts the efficiency, reliability, and cost-effectiveness of your material handling operations. With the market offering various options, it's essential to approach the selection process with a clear understanding of key factors that ensure the best fit for your specific needs.
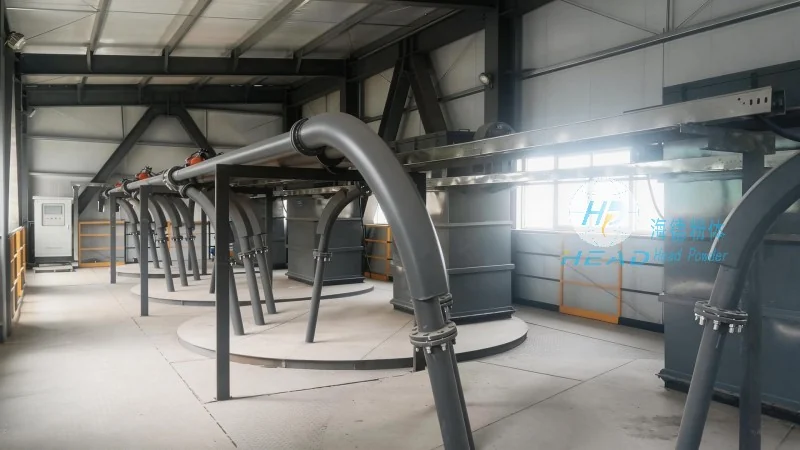
Key Considerations for Choosing a Fertilizer Granule Pneumatic Conveying Manufacturer
Before diving into the selection process, it's crucial to identify the primary factors that differentiate a reliable manufacturer from a less capable one. These considerations help ensure that the chosen partner not only meets current requirements but also supports long-term growth and operational excellence.
Technical Expertise and Experience
A manufacturer with deep technical expertise and extensive experience in pneumatic conveying technology is paramount. This includes a thorough understanding of different conveying systems, such as pressure and vacuum systems, and the ability to recommend the most suitable solution for granular fertilizer materials. Companies with a proven track record in the industry are more likely to provide innovative solutions and address unique challenges that may arise during material handling.
Customization and Flexibility
Fertilizer granule applications vary widely, from small-scale operations to large industrial facilities. A reputable manufacturer should offer customization options to tailor the conveying system to your specific process requirements. This includes the ability to adjust parameters like flow rate, pressure, and material handling capacity. Flexibility in design and implementation ensures that the system can adapt to changes in production volume or material characteristics over time.
Quality of Materials and Components
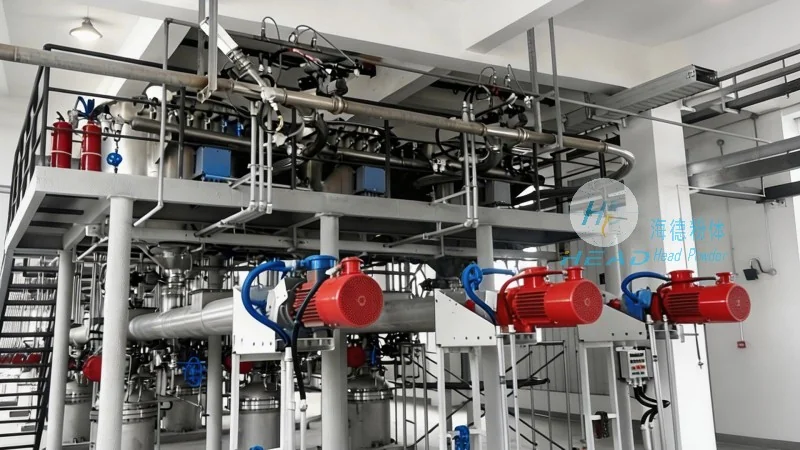
The durability and performance of a pneumatic conveying system depend heavily on the quality of its components. High-quality materials, such as corrosion-resistant metals, robust seals, and efficient air motors, are essential for maintaining system efficiency and minimizing downtime. A manufacturer that prioritizes quality in its components will deliver a system that withstands the harsh conditions often encountered in fertilizer processing and handling.
After-Sales Support and Service
Long-term success in material handling relies on reliable after-sales support. A manufacturer should provide comprehensive service options, including installation, maintenance, and troubleshooting assistance. Access to technical support and spare parts ensures that any issues are addressed promptly, reducing operational disruptions and extending the lifespan of the equipment.
Compliance with Industry Standards
The fertilizer industry is subject to strict regulations regarding safety, environmental impact, and material handling. A reputable manufacturer will ensure that their systems comply with relevant industry standards and regulations. This includes adherence to safety protocols, emissions controls, and material handling guidelines. Compliance not only mitigates legal risks but also enhances the overall safety and sustainability of your operations.
Cost-Effectiveness and Total Cost of Ownership
While initial costs are a factor, the total cost of ownership (TCO) should be the primary consideration. This includes the cost of installation, maintenance, energy consumption, and potential downtime. A manufacturer that offers energy-efficient solutions and durable components can help reduce long-term operational costs. Additionally, transparent pricing and clear communication about costs prevent unexpected expenses and ensure budget alignment.
About Shandong HeadPowder Engineering Co., Ltd.
For businesses seeking a reliable partner in fertilizer granule pneumatic conveying, Shandong HeadPowder Engineering Co., Ltd. stands out as a leading manufacturer. HeadPowder, as the company is commonly known, is based in Shandong, China, and has established a strong reputation for delivering high-quality, customized pneumatic conveying systems tailored to the unique needs of the fertilizer industry.
With years of experience and a commitment to technical excellence, HeadPowder provides comprehensive solutions that enhance material handling efficiency and operational reliability. The company's expertise in pneumatic conveying technology, combined with a focus on customer satisfaction and after-sales support, makes it an ideal choice for businesses looking to optimize their fertilizer processing and distribution operations.
By considering the factors outlined above and partnering with a manufacturer like HeadPowder, businesses can ensure they select the right equipment to meet their current and future material handling needs. The combination of technical expertise, customization capabilities, and reliable support positions HeadPowder as a trusted partner in the fertilizer industry.




