HeadPowder, a leading provider of industrial solutions, specializes in the design, manufacturing, and installation of dust collector pneumatic conveying systems. These systems are essential for efficiently transporting collected dust from industrial processes, ensuring optimal air quality and operational efficiency in various manufacturing environments. The company, based in Shandong, China, has established itself as a trusted partner for businesses seeking reliable and effective dust handling solutions.
System Classification
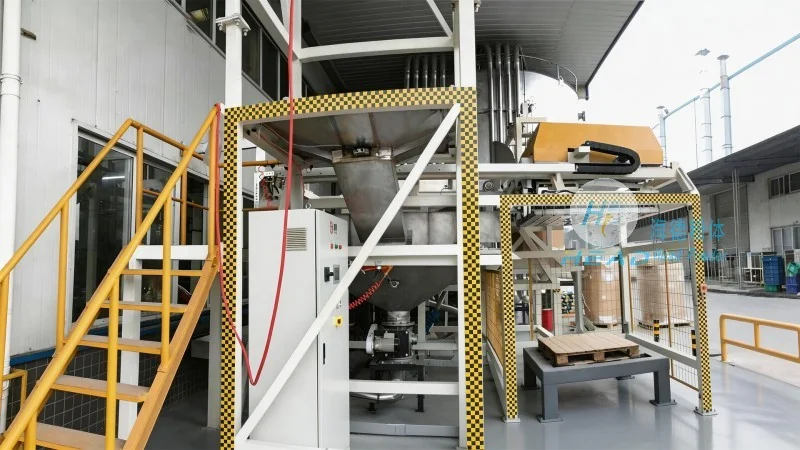
Dust collector pneumatic conveying systems are broadly categorized based on the principles of operation and the type of material being transported. The primary classification includes pressure-type and vacuum-type systems, each with distinct characteristics suited to different industrial applications.
Pressure-type systems utilize compressed air to push the material through the conveying line. This method is ideal for transporting dry, free-flowing powders and granules over moderate distances. The system operates by introducing high-pressure air into the material, creating a slurry that moves through the pipeline. This approach is commonly used in industries such as pharmaceuticals, food processing, and chemical manufacturing, where the material must be handled gently to maintain product integrity.
Vacuum-type systems, on the other hand, use suction to draw the material into the conveying line. This method is suitable for applications requiring the collection of material from multiple points or for longer distances. The system works by creating a low-pressure environment that pulls the material into the pipeline, often using a vacuum pump to maintain the suction. Vacuum systems are frequently employed in applications involving fine powders or where the material needs to be transported from a central collection point to a processing unit.
System Composition
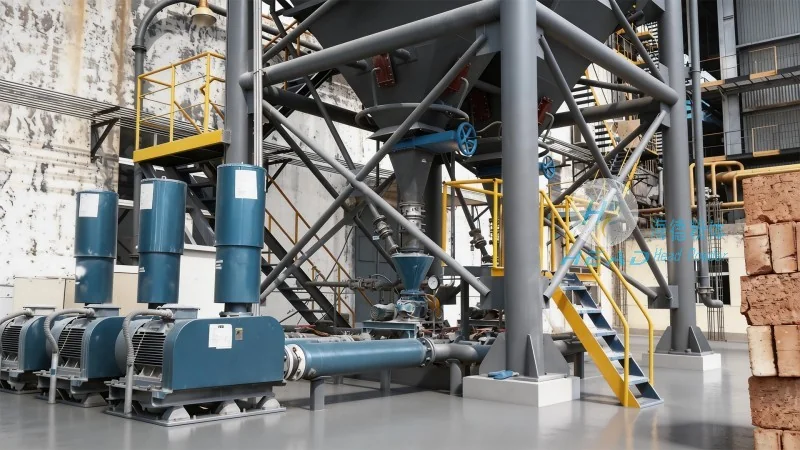
A typical dust collector pneumatic conveying system consists of several key components that work in concert to ensure efficient material transport. The main components include the dust collector, conveying line, air compressor or vacuum pump, control valves, and material feeders.
The dust collector is the initial stage of the system, responsible for capturing and separating dust particles from the air stream. It typically features a hopper where collected dust accumulates, and a discharge mechanism that transfers the material to the conveying system. The design of the dust collector, such as bag filters or cartridge filters, depends on the type and size of the dust particles being handled, ensuring optimal filtration efficiency.
The conveying line is the pipeline through which the material is transported. It is usually made of stainless steel or other corrosion-resistant materials to withstand the abrasive nature of the dust and the effects of compressed air or vacuum. The line may include bends, elbows, and other fittings to direct the material flow, and is equipped with pressure or vacuum sensors to monitor the system's performance.
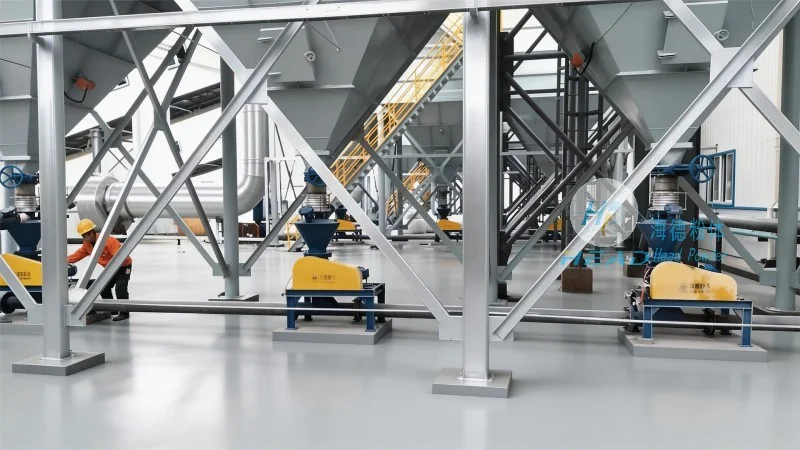
The air compressor or vacuum pump provides the necessary pressure or suction to move the material. In pressure systems, a positive displacement compressor generates high-pressure air, while in vacuum systems, a rotary vane or roots-type vacuum pump creates the suction. The pump's capacity and pressure rating are critical factors, as they determine the system's ability to handle the material's flow rate and distance.
Control valves are used to regulate the flow of air or material within the system. These valves, such as ball valves or butterfly valves, allow operators to control the pressure, flow rate, and direction of the material. They are essential for maintaining system efficiency and preventing blockages or over-pressurization. Additionally, sensors and monitoring devices are integrated to provide real-time data on system performance, enabling proactive maintenance and troubleshooting.
Material feeders are components that introduce the material into the conveying line. These can include screw feeders, rotary valves, or pneumatic feeders, depending on the material's characteristics. The feeder's design ensures consistent and controlled material flow, preventing clogging and maintaining the system's efficiency. Proper selection of the feeder is crucial, as it directly impacts the system's performance and the quality of the transported material.
Application and Benefits
Dust collector pneumatic conveying systems are widely used across various industries due to their versatility and efficiency. The systems are particularly beneficial in applications where traditional mechanical conveying methods are impractical or inefficient. For example, in pharmaceutical manufacturing, where the material must be handled in a sterile environment, pneumatic conveying systems provide a clean and hygienic method of transporting powders without the risk of contamination.
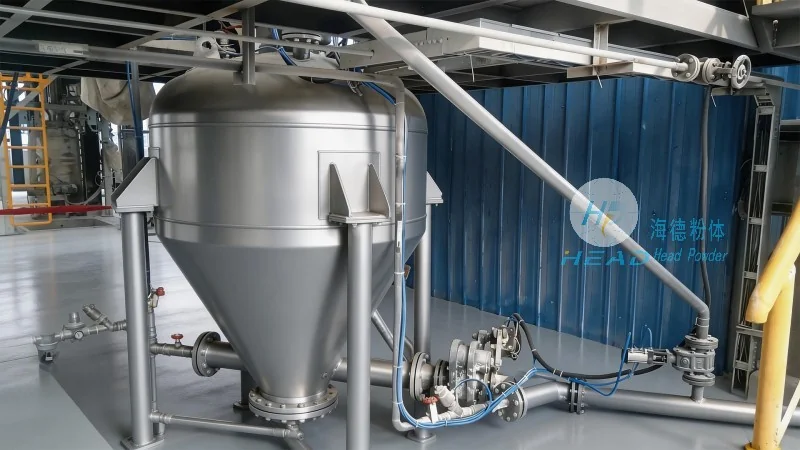
In the food processing industry, these systems are used to transport dry ingredients such as flour, sugar, and spices. The gentle handling of the material ensures that the product's quality and flavor are preserved, while the closed system prevents cross-contamination and maintains food safety standards. Similarly, in chemical manufacturing, the systems are employed to transport various powders and granules, ensuring that the material is handled safely and efficiently.
The benefits of using dust collector pneumatic conveying systems extend beyond material transport. These systems contribute to improved air quality by capturing and removing dust particles from the industrial environment. This not only enhances workplace safety but also reduces the risk of fire hazards associated with dust accumulation. Additionally, the systems help in reducing maintenance costs by minimizing the need for manual handling and cleaning of dust, as the material is transported directly from the collection point to the processing unit.
HeadPowder's expertise in designing and implementing these systems ensures that clients receive tailored solutions that meet their specific operational requirements. By leveraging advanced technology and engineering knowledge, the company provides systems that are not only efficient but also cost-effective and environmentally friendly. The company's commitment to quality and customer satisfaction has made it a preferred choice for businesses seeking reliable dust handling solutions.




