HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. This article delves into the core principles of intelligent tonne bag loading stations and their operational characteristics across various industrial applications.
Understanding the Core Principle of Pneumatic Conveying Systems
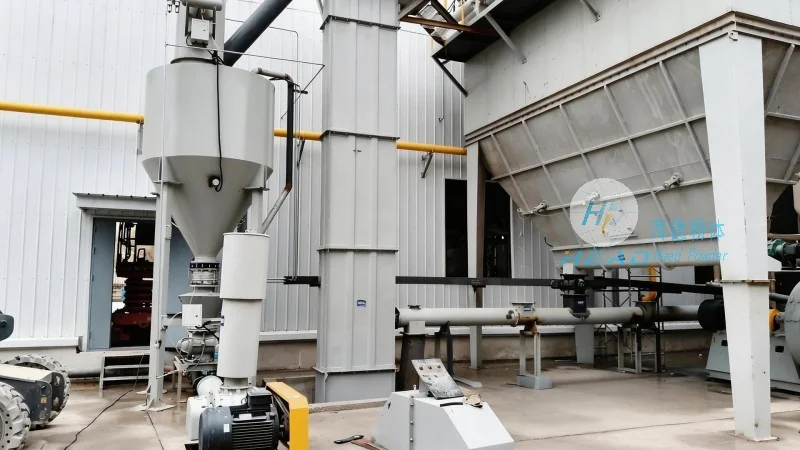
The intelligent tonne bag loading station, as part of a pneumatic conveying system, operates on the fundamental principle of transporting bulk materials through a pressurized or vacuumed air stream. Unlike traditional mechanical conveying methods, this system utilizes air as the primary medium to move powders, granules, and other bulk solids from the source to the destination. The process typically involves a hopper or silo where the material is stored, a loading station equipped with a bagging machine or a hopper discharge valve, and a conveying pipeline that connects these components. The system can function under positive pressure (where air is forced through the material) or negative pressure (where air is drawn through the material), depending on the specific requirements of the material being handled and the layout of the facility.
Key Components and Their Functional Roles
Several critical components work in tandem to ensure the efficient operation of the intelligent tonne bag loading station. The primary components include the material hopper or silo, which stores the bulk material; the loading valve or discharge mechanism, which controls the flow of material from the storage to the conveying line; the conveying pipeline, which transports the material; and the dust collector or filter system, which ensures air quality compliance and material recovery. In an intelligent system, additional components such as sensors, control panels, and automated bagging units enhance operational efficiency and safety. For instance, level sensors monitor the material level in the hopper, preventing overfilling or underfilling, while pressure sensors regulate the air pressure in the conveying line to maintain optimal flow rates. The control panel integrates all these functions, allowing operators to monitor and adjust the system parameters in real-time, ensuring consistent performance and minimizing downtime.
Working Scene Characteristics: Applications and Operational Environments
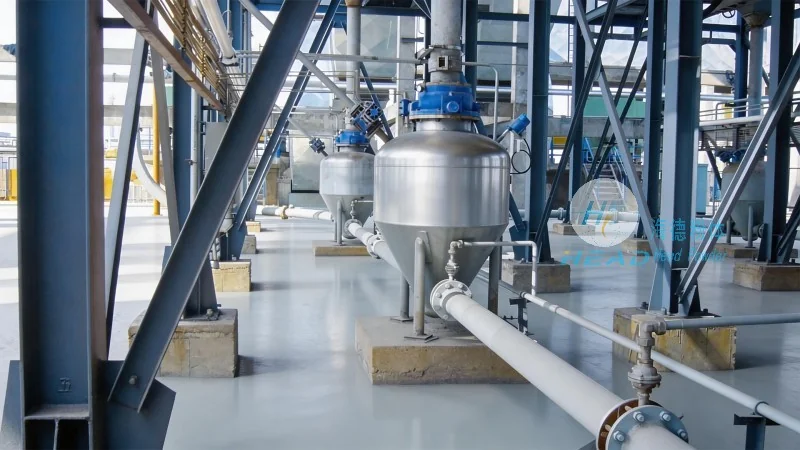
The intelligent tonne bag loading station is widely used in various industrial sectors, including chemical, pharmaceutical, food processing, and mining industries. Its adaptability to different working environments is a key characteristic. In chemical plants, for example, the system can handle corrosive or hazardous materials while maintaining strict safety standards. The sealed design of the loading station prevents dust emissions and contamination, which is crucial in pharmaceutical and food industries where product purity is paramount. In mining operations, the system efficiently transports bulk minerals from the mine to processing facilities, reducing manual labor and enhancing safety. The system's ability to operate in both indoor and outdoor settings makes it versatile, though indoor installations are more common to control environmental factors and ensure material quality. The working scene characteristics also include the system's scalability, as it can be customized to handle different material types, quantities, and conveying distances. This flexibility allows industries to adapt the system to their specific production needs, whether for small-scale batch processing or large-scale continuous operations.
Advantages and Operational Benefits
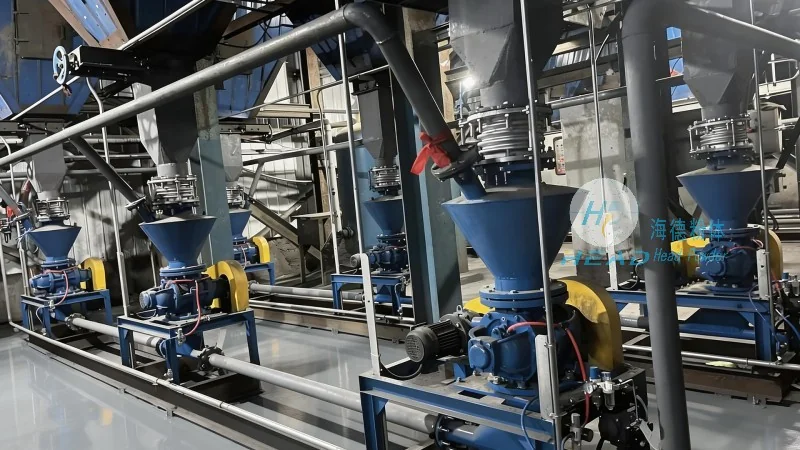
Implementing an intelligent tonne bag loading station with a pneumatic conveying system offers several advantages over traditional methods. One of the most significant benefits is the reduction in manual labor, as the system automates the loading and conveying process. This not only improves efficiency but also enhances workplace safety by minimizing the risk of accidents associated with manual handling of bulk materials. The system also ensures consistent material flow and quality, as it maintains a steady pressure and flow rate, preventing material segregation or clumping. This consistency is particularly important in industries where material uniformity is critical, such as in the production of food products or pharmaceuticals. Additionally, the sealed design of the system reduces dust emissions, improving air quality and compliance with environmental regulations. The automated control system allows for remote monitoring and operation, enabling operators to manage the system from a central location, which is especially beneficial in large facilities or those with multiple loading stations. This feature enhances operational flexibility and allows for quick adjustments to production schedules or material changes.
Conclusion: The Role of HeadPowder in Delivering Advanced Material Handling Solutions
HeadPowder Engineering Co., Ltd., based in Shandong, China, is at the forefront of developing and supplying intelligent tonne bag loading stations and pneumatic conveying systems. The company's expertise in material handling technology ensures that their products are designed to meet the specific needs of various industries, offering reliable, efficient, and safe solutions. By integrating advanced automation and control systems, HeadPowder's equipment enhances operational efficiency, reduces costs, and improves product quality. The working scene characteristics of these systems, combined with their adaptability to different industrial applications, make them a valuable asset for businesses seeking to optimize their material handling processes. As industries continue to evolve, the demand for advanced material handling solutions will only increase, and companies like HeadPowder will play a crucial role in meeting these needs with innovative and reliable products.




