Warehouse vacuum conveying systems are advanced industrial equipment designed to transport bulk materials efficiently within storage facilities. These systems utilize vacuum technology to draw materials from a source and deliver them to a designated destination, offering a flexible and reliable solution for material handling in various warehouse environments. The core components and operational principles of such systems are crucial for understanding their functionality and applicability in different working scenarios.
Core Principles of Warehouse Vacuum Conveying Systems
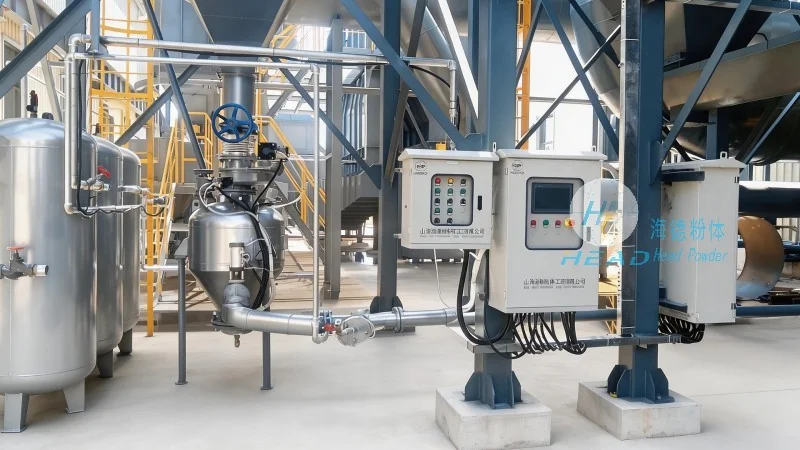
The fundamental principle of warehouse vacuum conveying systems is the creation of a pressure differential between the material source and the receiving point. By generating a vacuum in the conveying line, the system draws particles or granules from the source, such as a hopper or storage bin, and transports them through a pipeline to the target location. This process relies on the pressure difference to overcome gravitational and frictional forces, enabling the movement of materials without the need for mechanical conveyors like belts or rollers. The vacuum is typically generated by a vacuum pump, which can be either rotary vane or roots-type, depending on the system's capacity and application requirements. The system also includes filters to remove dust and particles from the air, ensuring the conveyed material remains clean and free from contamination. Additionally, control valves and sensors are integrated to regulate the flow rate and monitor system performance, enhancing operational efficiency and safety.
Working Scene Characteristics and Applications
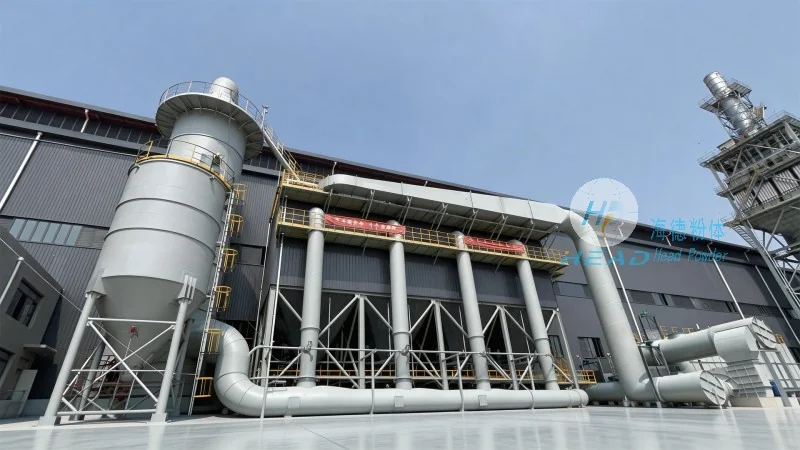
Warehouse vacuum conveying systems are particularly well-suited for applications involving fine powders, granules, or small particles that are difficult to handle with traditional mechanical conveyors. Common working scenes include pharmaceutical manufacturing, food processing, chemical production, and logistics centers where material purity and contamination control are critical. In pharmaceutical warehouses, for example, vacuum conveying systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the materials remain sterile and free from cross-contamination. The systems' ability to operate in a closed environment minimizes dust exposure and maintains a cleanroom-like atmosphere, which is essential for meeting regulatory standards. In food processing facilities, vacuum conveying is employed to handle ingredients like flour, sugar, and spices, where hygiene and product integrity are paramount. The gentle handling of materials by the vacuum system prevents degradation or damage, preserving the quality of the products. For chemical manufacturers, the systems are used to transport powders and granules that may be hazardous or reactive, with sealed pipelines and proper filtration preventing leaks and ensuring worker safety. In logistics centers, vacuum conveying systems facilitate the transfer of materials between storage bins and packaging lines, improving workflow efficiency and reducing manual handling errors. The flexibility of the system allows for easy reconfiguration of the conveying path, adapting to changes in warehouse layout or production needs.
Advantages and Technical Specifications
Warehouse vacuum conveying systems offer several advantages over traditional material handling methods. One of the key benefits is the ability to handle a wide range of materials, from fine powders to larger granules, without the need for specialized equipment for each material type. The systems are also highly flexible, as the conveying lines can be easily reconfigured or extended to accommodate changes in the warehouse layout or production requirements. This adaptability reduces downtime and increases operational efficiency. Additionally, vacuum conveying systems are energy-efficient compared to other conveying methods, as they use less power to transport materials over short to medium distances. The closed system design minimizes dust emissions and improves workplace safety, making it suitable for environments where air quality is a concern. Technical specifications of these systems vary based on the application, with factors such as conveying capacity, pipeline length, and material characteristics influencing the system's design. For instance, a system designed for pharmaceutical use may have a lower conveying capacity and more stringent filtration requirements compared to a system used in a chemical plant. The vacuum pump's power and the number of filter stages are critical parameters that determine the system's performance and suitability for specific applications.
About Shandong HeadPowder Engineering Co., Ltd.
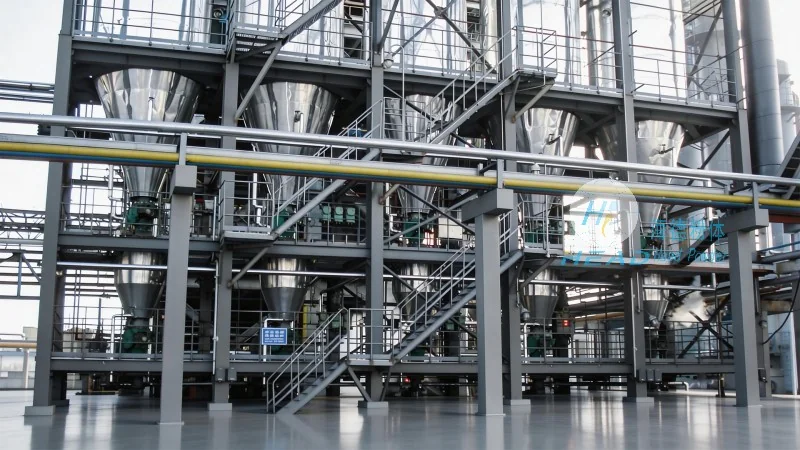
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of warehouse vacuum conveying systems and related industrial equipment. The company is headquartered in Shandong, China, and specializes in providing customized solutions for material handling challenges in various industries. With years of experience in the field, headpowder has developed advanced technologies and innovative designs that enhance the efficiency and reliability of vacuum conveying systems. The company's products are known for their high quality, durability, and compliance with international standards, making them suitable for demanding industrial environments. Headpowder's commitment to research and development ensures that their systems incorporate the latest advancements in vacuum technology, filtration, and control systems. The company also provides comprehensive after-sales support, including installation, maintenance, and technical assistance, to ensure that customers can maximize the performance and lifespan of their equipment. By combining expertise in engineering and manufacturing, headpowder delivers solutions that meet the unique needs of each client, contributing to improved productivity and operational efficiency in material handling processes.




