HeadPowder, a professional manufacturer based in Shandong, China, specializes in providing advanced pneumatic conveying solutions tailored for the efficient handling of potash fertilizer. This article delves into the core principles behind such equipment and highlights the key characteristics of its working environments, offering insights into how these systems enhance operational efficiency in fertilizer processing and distribution.
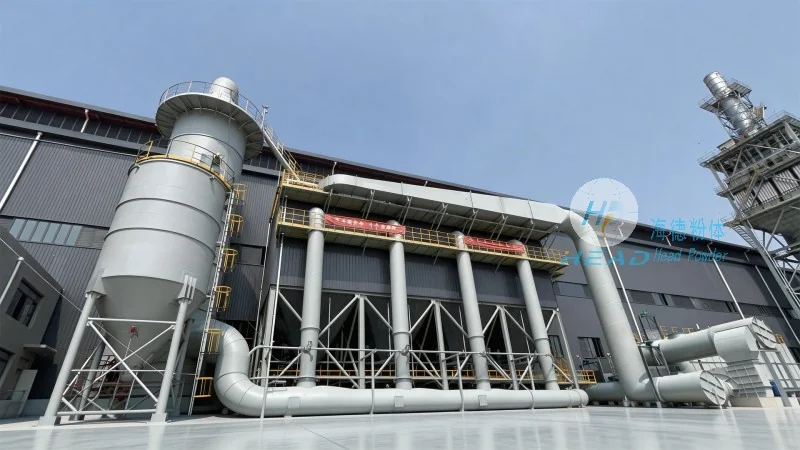
About HeadPowder: Leading Pneumatic Conveying Solutions
HeadPowder Engineering Co., Ltd. is a reputable company headquartered in Shandong, China. With years of experience in the engineering and manufacturing of pneumatic conveying systems, HeadPowder has established itself as a trusted partner for industries requiring reliable and efficient material handling solutions. The company's commitment to innovation and quality ensures that its products meet the stringent demands of modern fertilizer production and processing facilities.
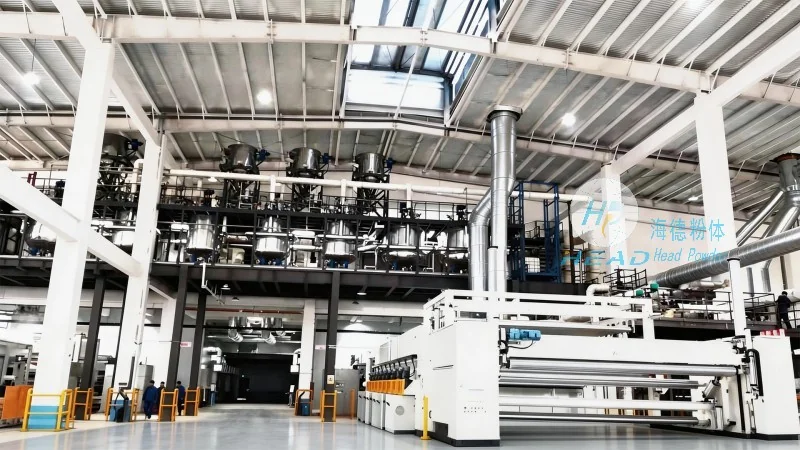
Principle of Pneumatic Conveying Systems for Potash Fertilizer
The fundamental principle of pneumatic conveying for potash fertilizer involves the use of a pressurized or vacuum system to transport bulk materials through a pipeline. In a typical setup, a fan or blower generates airflow that moves the fertilizer particles along the pipeline. This method eliminates the need for mechanical components like conveyor belts or buckets, reducing maintenance costs and increasing operational safety. The system can operate under positive pressure (where air pushes the material) or negative pressure (where air pulls the material), with the choice depending on the specific application and material characteristics. For potash fertilizer, which is often granular and abrasive, the design of the conveying line, including the type of pipeline, valves, and filters, is crucial to prevent blockages and ensure consistent flow.
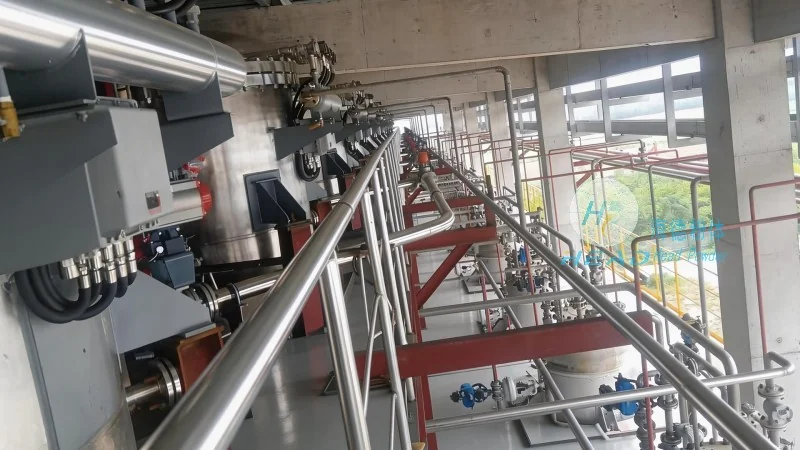
Working Scene Characteristics and Applications
The working scene characteristics of potash fertilizer pneumatic conveying equipment are tailored to the unique demands of fertilizer production and storage facilities. These systems are commonly used in scenarios such as transferring raw potash from storage silos to processing units, moving finished fertilizer products from production lines to packaging areas, and handling bulk materials in warehouse environments. The key characteristics of these working scenes include high material throughput, the need for dust control measures, and the requirement for equipment that can handle abrasive materials without degradation. For instance, in a large-scale fertilizer plant, the pneumatic conveying system may need to transport thousands of tons of potash fertilizer per day, requiring robust and reliable components that can withstand continuous operation. The working environment may also involve variable temperatures and humidity levels, necessitating equipment with appropriate sealing and corrosion-resistant materials to maintain performance over time.
Advantages of Pneumatic Conveying in Potash Fertilizer Handling
Implementing pneumatic conveying systems for potash fertilizer offers several advantages over traditional mechanical methods. Firstly, it provides a fully enclosed system, which helps in controlling dust emissions and maintaining a clean working environment, a critical factor in fertilizer processing where dust can affect both worker health and product quality. Secondly, the system is highly flexible, allowing for easy reconfiguration of the conveying line to adapt to changes in production schedules or facility layouts. Thirdly, the absence of moving parts in the conveying line reduces the risk of mechanical failure and lowers maintenance requirements, leading to lower operational costs. Additionally, pneumatic conveying can handle materials with varying particle sizes and moisture content, making it suitable for a wide range of potash fertilizer products. These advantages make pneumatic conveying an ideal solution for modern fertilizer facilities aiming to enhance efficiency, safety, and sustainability.
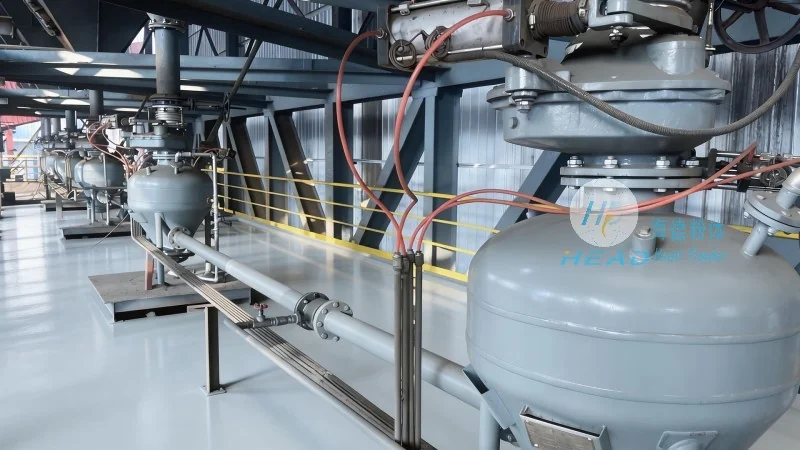
Conclusion: Enhancing Efficiency with Pneumatic Conveying
In conclusion, the pneumatic conveying equipment for potash fertilizer, as developed by HeadPowder Engineering Co., Ltd., represents a sophisticated solution for the efficient handling of bulk materials in fertilizer production. By understanding the principles of pneumatic conveying and the characteristics of working environments, industries can optimize their material handling processes, reduce costs, and improve overall operational performance. The advanced technology and expertise of HeadPowder ensure that their systems are tailored to meet the specific needs of each client, providing reliable and efficient solutions for the transportation of potash fertilizer in various industrial settings.




