For industrial applications that require efficient handling of bulk powders, the automatic powder bag opening and pneumatic conveying system represents a sophisticated solution designed to streamline material transfer processes. This technology is integral to industries such as pharmaceuticals, chemicals, food processing, and mining, where precision and reliability are paramount. The system integrates automated bag opening mechanisms with pneumatic conveying to ensure safe, dust-free, and efficient movement of powders from storage to processing equipment.
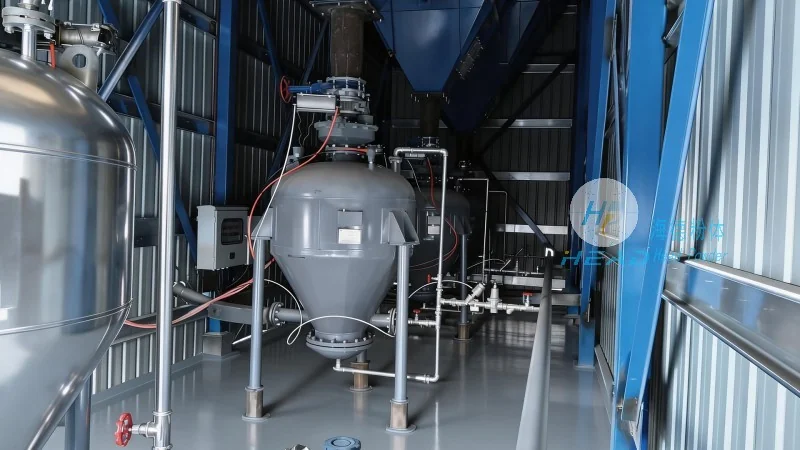
Overview of the Automatic Powder Bag Opening and Pneumatic Conveying System
The system is engineered to handle various types of bulk powders, including fine powders, granules, and bulk materials. It combines mechanical bag opening capabilities with pneumatic conveying technology to eliminate manual labor and reduce the risk of contamination. The core components include a bag opening device, a hopper for material collection, a conveying line, and a receiver for final material storage. Each component is designed to work in tandem to achieve seamless material flow from the initial bag to the processing unit.
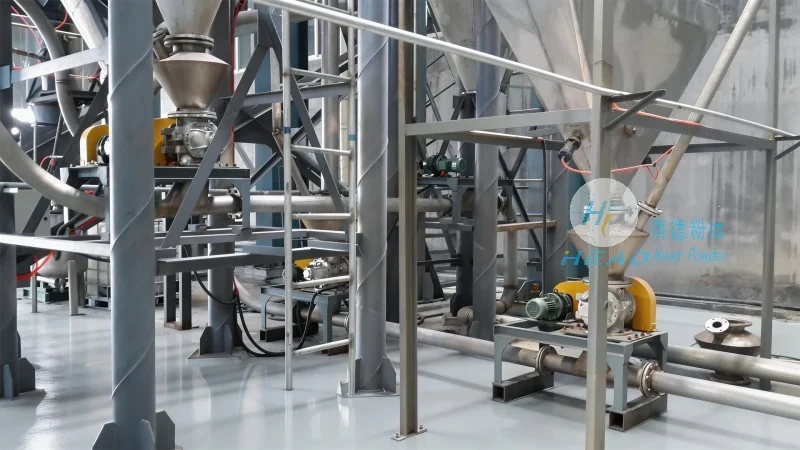
Working Principle of the System
The operation of the automatic powder bag opening and pneumatic conveying system begins with the placement of a sealed bag into the opening station. The system uses a mechanical or pneumatic actuator to open the bag, typically by cutting or tearing the top seal. Once the bag is opened, the powder is discharged into the hopper. The hopper then feeds the material into the conveying line through a rotary valve or similar device. The conveying line utilizes compressed air to create a flow of air and powder, transporting the material to the receiver. The receiver collects the material and may include a dust collection system to ensure environmental compliance and product purity. The entire process is automated, with sensors and controls monitoring the flow rate, pressure, and other parameters to maintain optimal performance.
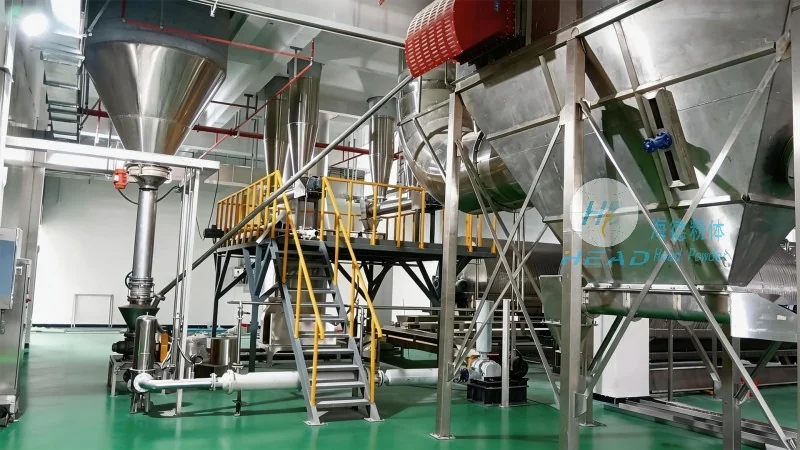
Key Features and Advantages
One of the primary advantages of this system is its ability to handle powders without manual intervention, reducing labor costs and minimizing the risk of human error or contamination. The automated bag opening mechanism ensures consistent and reliable material discharge, while the pneumatic conveying system provides a dust-free environment, which is critical for industries where product purity is essential. The system is also designed for flexibility, allowing it to handle different bag sizes and types, and can be integrated with existing processing equipment. Additionally, the system offers energy efficiency through optimized air flow and pressure control, reducing operational costs. The integration of dust collection systems further enhances safety and compliance with environmental regulations.
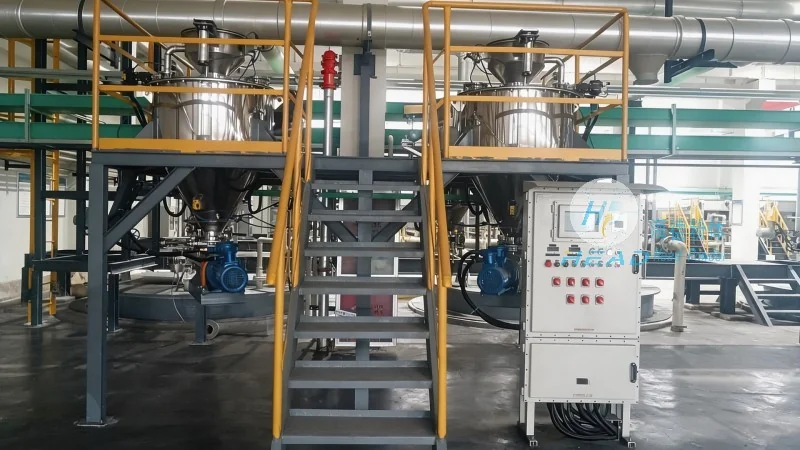
Technical Specifications and Applications
The system is manufactured by Shandong HeadPowder Engineering Co., Ltd., a company based in Shandong, China, with expertise in bulk material handling solutions. The company specializes in designing and producing customized systems tailored to the specific needs of various industries. The system is available in different configurations, including low-pressure and high-pressure pneumatic conveying, to suit various material characteristics and processing requirements. Applications include pharmaceutical manufacturing, where the system ensures sterile and contamination-free powder transfer; chemical processing, where it handles hazardous or reactive powders safely; and food processing, where it maintains hygiene standards. The system's modular design allows for easy installation and integration into existing production lines, minimizing downtime and operational disruptions.




