

What is a Chocolate Powder Pneumatic Conveying Equipment? And What Are Its Design Principles?
Chocolate powder pneumatic conveying equipment is a specialized system designed to transport chocolate powder efficiently and reliably in industrial settings. This equipment is crucial for manufacturers dealing with chocolate products, as it ensures the safe and hygienic handling of this delicate powder. The system operates by using compressed air to move the powder through a network of pipes, eliminating the need for mechanical components that might cause contamination or damage to the product.
About HeadPowder: Experts in Pneumatic Conveying Solutions
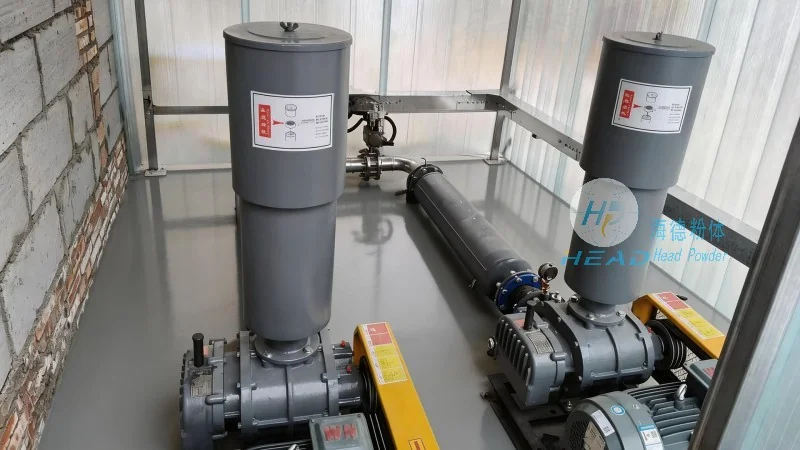
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer based in Shandong, China. With years of experience in the field, the company specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to the unique needs of the food and confectionery industry. Their expertise lies in creating equipment that meets stringent hygiene standards while ensuring optimal performance and durability.
Design Principles of Chocolate Powder Pneumatic Conveying Equipment
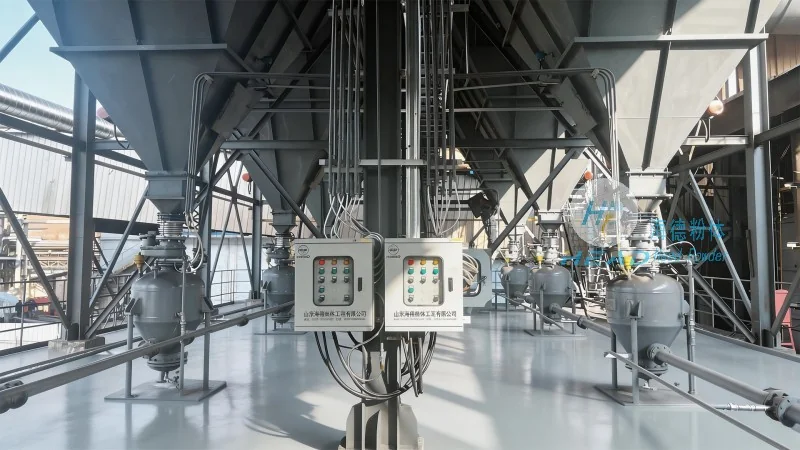
The design of chocolate powder pneumatic conveying equipment is based on several key principles to ensure efficient and safe operation. The first principle is the use of positive pressure or negative pressure systems. Positive pressure systems use compressed air to push the powder through the pipeline, while negative pressure systems use vacuum to draw the powder. For chocolate powder, positive pressure systems are often preferred as they provide better control over the flow and reduce the risk of product degradation. Another critical design principle is the selection of appropriate materials. The equipment must be made from food-grade materials, such as stainless steel, to prevent contamination and ensure compliance with food safety regulations. The design also considers the particle size and flow characteristics of the chocolate powder, as these factors affect the system's performance and efficiency.
Key Components and Their Functions
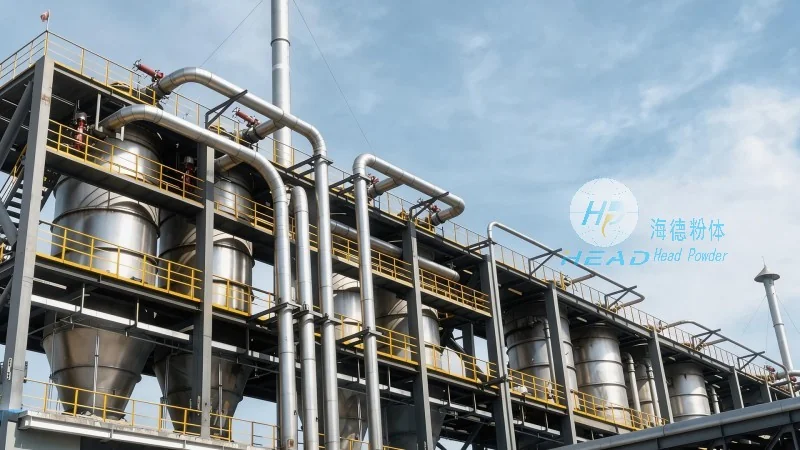
Chocolate powder pneumatic conveying equipment typically consists of several key components, each playing a vital role in the overall system. The first component is the feeder, which is responsible for feeding the chocolate powder into the conveying line. The feeder must be designed to handle the powder's flow characteristics and prevent clogging. The second component is the air compressor or vacuum pump, which provides the necessary pressure or vacuum to move the powder. The third component is the pipeline system, which transports the powder from the feeder to the destination. The pipeline is usually made of stainless steel and is designed to be smooth and free of sharp edges to prevent product damage. The fourth component is the separator, which separates the powder from the air at the end of the pipeline. The separator is crucial for maintaining the product's quality and preventing dust accumulation. Finally, the system may include a filter to remove any remaining particles from the air, ensuring a clean and safe environment.
Advantages of Using Chocolate Powder Pneumatic Conveying Equipment
There are several advantages to using chocolate powder pneumatic conveying equipment in industrial settings. The first advantage is efficiency. The system can transport large quantities of chocolate powder quickly and with minimal labor. This is particularly beneficial for manufacturers who need to process large batches of chocolate products. The second advantage is hygiene. The equipment is designed to be clean and easy to maintain, reducing the risk of contamination. This is essential for the food industry, where product safety is paramount. The third advantage is flexibility. The system can be customized to meet the specific needs of a manufacturer, including different pipe sizes, lengths, and feeding rates. This allows for a flexible and adaptable solution that can grow with the business. Finally, the equipment is cost-effective in the long run. Although the initial investment may be higher than traditional mechanical systems, the reduced labor costs and increased efficiency lead to significant savings over time.
Conclusion
Chocolate powder pneumatic conveying equipment is an essential tool for manufacturers in the chocolate industry. It provides an efficient, hygienic, and flexible solution for transporting chocolate powder. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., manufacturers can ensure that their equipment meets the highest standards of quality and performance. By understanding the design principles and key components of this equipment, manufacturers can make informed decisions and choose the best system for their needs.