Magnesium oxide powder, a widely used chemical compound in various industrial applications, often requires efficient and reliable handling methods. The magnesium oxide powder pneumatic conveying system equipment is a specialized solution designed to transport this material safely and effectively. This system utilizes air as the conveying medium to move the powder from one location to another, offering advantages such as reduced dust exposure, improved material quality, and enhanced operational flexibility.
Key Components of the Pneumatic Conveying System
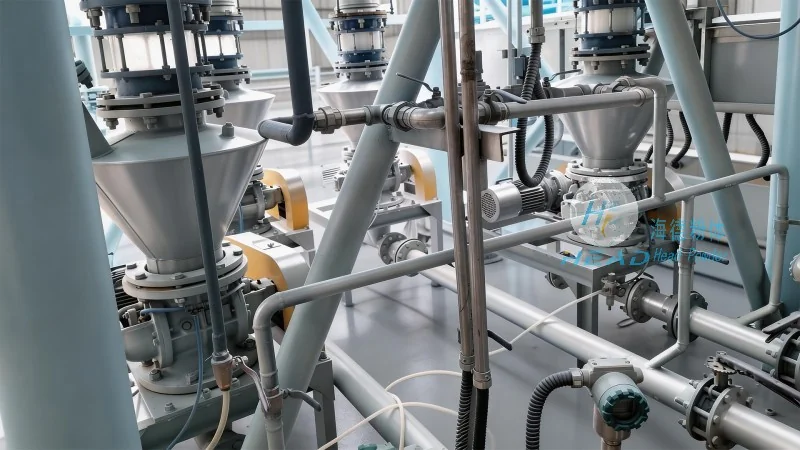
The magnesium oxide powder pneumatic conveying system typically consists of several core components that work in tandem to ensure smooth operation. These include a material hopper or feeder, a conveying line (often equipped with a venturi or rotary valve), a dust collector or filter system, and a control unit. The material hopper is responsible for storing and feeding the magnesium oxide powder into the system, while the conveying line transports the material through the air stream. The venturi or rotary valve regulates the flow rate and pressure, ensuring consistent and controlled movement of the powder. The dust collector or filter system is crucial for maintaining air quality and preventing dust emissions, which is particularly important for handling fine powders like magnesium oxide. The control unit manages the entire system, monitoring parameters such as pressure, flow rate, and material level to optimize performance and prevent operational issues.
Design Principles and Operational Mechanisms
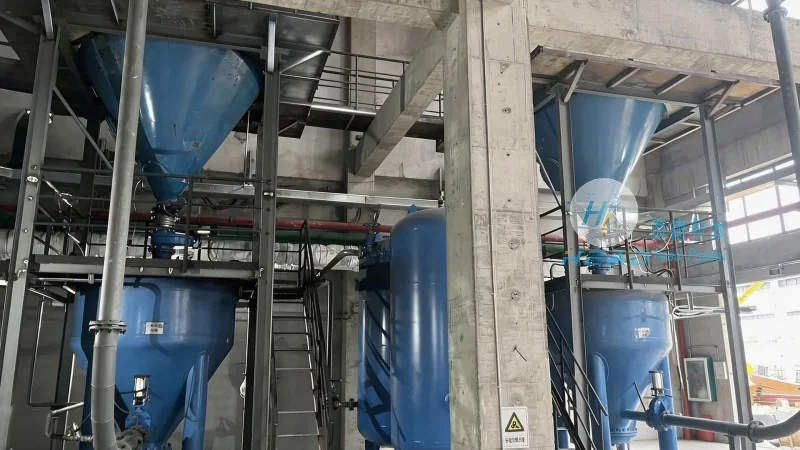
The design of the magnesium oxide powder pneumatic conveying system is based on fundamental principles of fluid dynamics and material handling. The primary design principle is to create a stable air-powder mixture that allows for efficient transport without causing particle degradation or blockages. This involves selecting appropriate air velocities and pressure differentials to ensure that the powder particles are entrained in the air stream and transported smoothly. The system must also account for the physical properties of magnesium oxide powder, such as its particle size, density, and flowability, as these factors significantly impact the conveying efficiency. For example, fine magnesium oxide particles may require higher air velocities to prevent settling or clogging in the conveying line. The design also considers the need for minimal pressure loss and energy consumption, as these are critical factors in the overall operational cost and efficiency of the system. Additionally, the system must be designed to handle variations in material feed rates and flow conditions, ensuring consistent performance under different operational scenarios.
Advantages of Using a Pneumatic Conveying System for Magnesium Oxide Powder
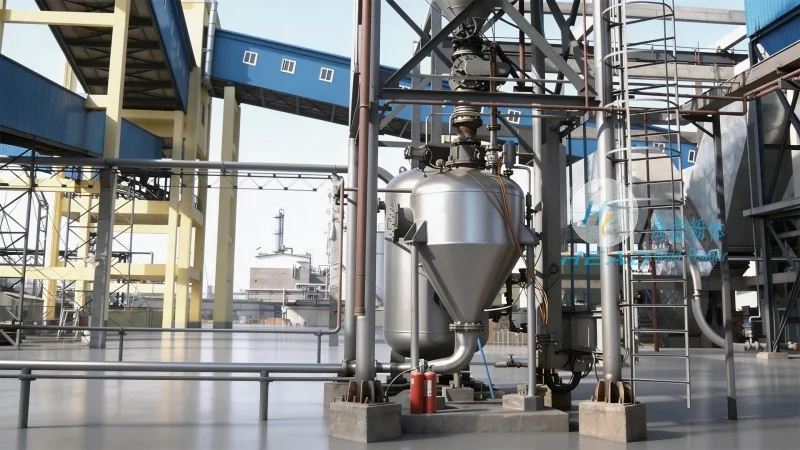
Implementing a pneumatic conveying system for magnesium oxide powder offers several key advantages over traditional methods like bulk handling or manual transport. One of the most significant benefits is the reduction in dust exposure, which enhances workplace safety and compliance with environmental regulations. The enclosed system prevents dust from being released into the air, minimizing the risk of respiratory issues or contamination of other materials. Another advantage is the improved material quality, as the system prevents contamination from external sources and reduces the risk of particle degradation due to exposure to air or moisture. This is particularly important for magnesium oxide, which is often used in applications where purity is critical, such as in pharmaceuticals or food processing. The system also offers enhanced operational flexibility, allowing for easy integration with existing production lines and the ability to transport material over long distances without the need for additional equipment like conveyor belts or trucks. Furthermore, the pneumatic conveying system can be designed to handle varying feed rates and material types, making it a versatile solution for different industrial applications.
Application Scenarios and Industry Impact
The magnesium oxide powder pneumatic conveying system is widely used in various industries that rely on the efficient handling of fine powders. In the chemical industry, it is commonly used for transporting magnesium oxide from storage facilities to processing plants, ensuring a continuous and reliable supply of raw material. In the pharmaceutical industry, the system is employed to transport magnesium oxide into production lines for the manufacturing of medications or supplements, where maintaining high purity and preventing contamination is paramount. The food industry also utilizes this system for handling magnesium oxide used as a food additive or in food processing, as it ensures the material is handled hygienically and without cross-contamination. Additionally, the system is used in the construction industry for transporting magnesium oxide used in cement production or as a filler in building materials. The widespread adoption of this system has significantly improved operational efficiency and safety in these industries, reducing downtime and operational costs associated with traditional material handling methods.
Conclusion and Company Overview
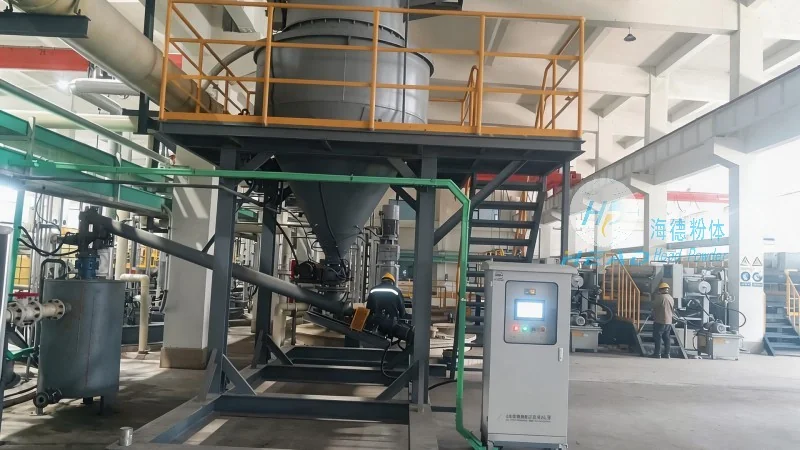
Overall, the magnesium oxide powder pneumatic conveying system equipment is a sophisticated and essential solution for the efficient and safe handling of magnesium oxide powder. Its design, based on principles of fluid dynamics and material science, ensures optimal performance and reliability. The system's components work together to create a stable air-powder mixture, transport the material efficiently, and maintain air quality. The advantages of using this system, including reduced dust exposure, improved material quality, and enhanced operational flexibility, make it a preferred choice in various industrial applications. As a leading provider of such systems, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying solutions tailored to the specific needs of clients. With a focus on quality, efficiency, and safety, the company has established itself as a trusted partner in the industry, delivering reliable equipment that meets the highest standards of performance and compliance. Based in China, Shandong HeadPowder Engineering Co., Ltd. leverages its expertise and experience to provide innovative solutions that enhance the productivity and safety of industrial operations.




