Exploring the Molybdenum Oxide Material Handling Conveyor and Its Core Design Principles
Introduction to Molybdenum Oxide Material Handling Conveyors
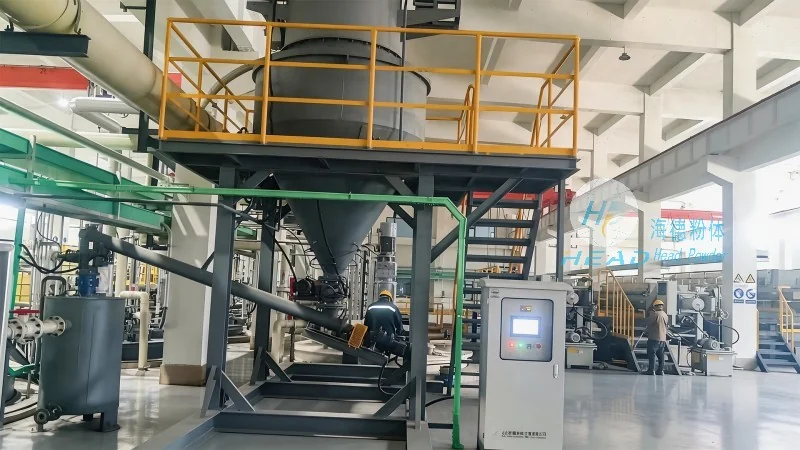
A Molybdenum Oxide Material Handling Conveyor is an industrial system engineered to transport and manage molybdenum oxide, a vital material in numerous high-tech and industrial applications. This equipment is integral to the efficient flow of material within processing facilities, particularly in sectors where molybdenum oxide serves as a raw material or intermediate product. The design of such conveyors is tailored to the unique physical and chemical properties of molybdenum oxide, ensuring reliable and safe material transport. By integrating advanced engineering techniques, these conveyors provide a solution for industries that depend on consistent and efficient handling of this material.
Key Components and Operational Mechanisms
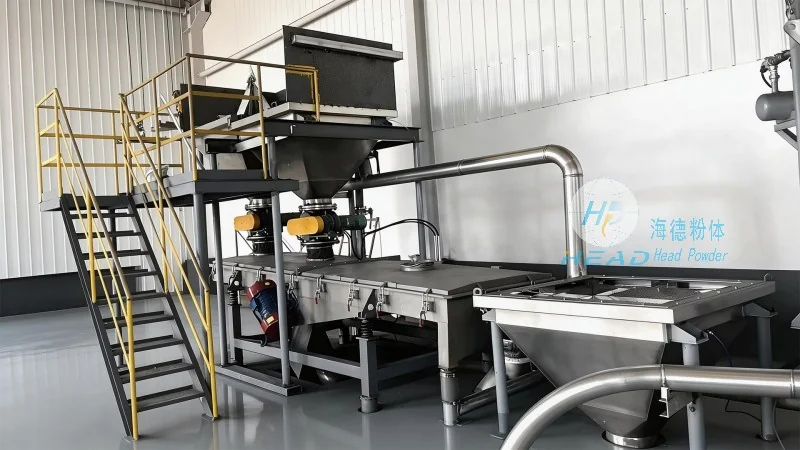
The Molybdenum Oxide Material Handling Conveyor comprises several critical components that collaborate to facilitate material transport. These components include feed hoppers, conveyor mechanisms (such as belt or roller systems), control systems, and discharge units. The feed hopper is responsible for receiving molybdenum oxide from storage or upstream processing stages, ensuring a steady flow of material into the conveyor system. The conveyor mechanism then moves the material along the designated path, with the control systems monitoring operation and adjusting parameters as needed. The discharge mechanism delivers the molybdenum oxide to the next processing or storage stage. Each component is designed to handle the specific characteristics of molybdenum oxide, including its particle size, moisture content, and potential dust generation. The system is engineered to maintain consistent flow rates, minimizing bottlenecks and ensuring smooth material movement.
Design Principles for Optimal Performance
The design principles of a Molybdenum Oxide Material Handling Conveyor are centered on maximizing efficiency, safety, and durability. Engineers at Shandong HeadPowder Engineering Co., Ltd. prioritize several key aspects during the design process. First, the conveyor is engineered to accommodate the specific physical and chemical properties of molybdenum oxide. This includes considerations for the material's density, flow characteristics, and potential reactivity under high-temperature or chemical conditions. The design ensures consistent material flow and prevents issues such as clogging or uneven distribution. Second, safety is a paramount consideration. The conveyor incorporates enclosed structures to contain dust and prevent environmental contamination, along with emergency stop mechanisms to protect operators and equipment. Third, durability is achieved through the use of high-quality, corrosion-resistant materials and wear-resistant components, ensuring the system can withstand the harsh conditions of molybdenum oxide handling. The design also emphasizes energy efficiency, using motorized systems that adjust speed based on load to reduce energy consumption. By adhering to these design principles, the conveyor system delivers reliable performance and long-term operational reliability.
Applications Across Various Industries
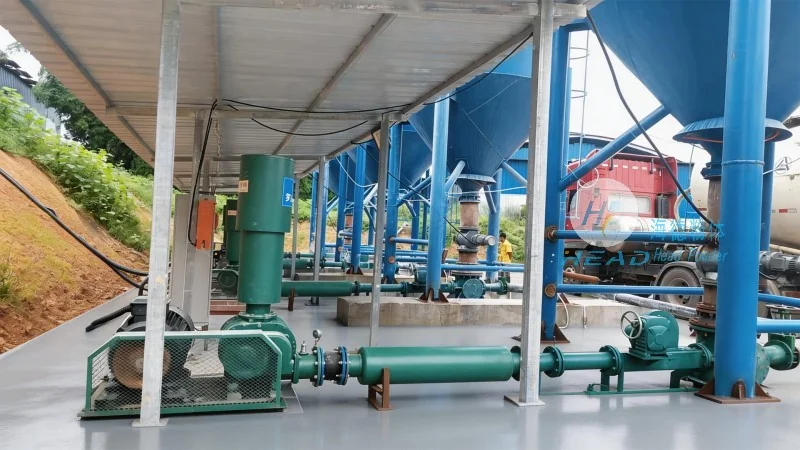
Molybdenum oxide material handling conveyors are widely utilized across multiple industries that rely on molybdenum oxide in their production processes. These industries include the chemical manufacturing sector, where molybdenum oxide is used in the production of molybdenum compounds and catalysts. The petroleum and refining industry also utilizes molybdenum oxide in the formulation of lubricants and additives. Additionally, the steel and metal processing industries employ molybdenum oxide as an alloying agent to enhance the properties of steel. The electronics industry benefits from molybdenum oxide in the production of electronic components and protective coatings. In each of these applications, the conveyor system plays a vital role in safely and efficiently transporting molybdenum oxide from storage to processing units. The design of the conveyor is adapted to the specific requirements of each industry, such as handling large volumes of material or operating in high-temperature environments. The consistent performance of the conveyor system contributes to the overall productivity and quality of the end products in these sectors.
Advantages of Implementing a Molybdenum Oxide Material Handling Conveyor
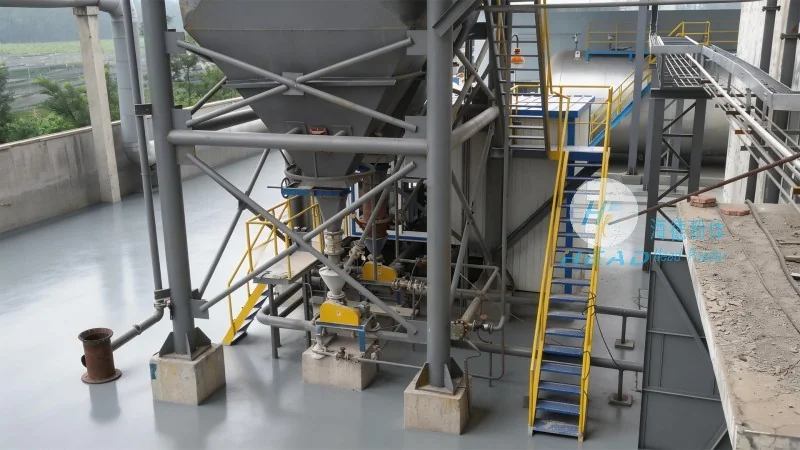
Adopting a Molybdenum Oxide Material Handling Conveyor offers significant advantages for industrial operations. One primary benefit is improved operational efficiency. By automating material transport, the conveyor reduces the need for manual labor, minimizing human error and increasing the speed of material flow. This leads to higher production throughput and reduced downtime. Another advantage is enhanced workplace safety. The enclosed design prevents dust and particles from escaping into the environment, protecting both workers and the surrounding ecosystem. The control systems also provide real-time monitoring, allowing operators to quickly identify and address any issues that may arise. Additionally, the durability of the conveyor system ensures long-term reliability, reducing maintenance costs and extending the lifespan of the equipment. The energy-efficient design helps lower operational costs, making the conveyor a cost-effective solution for industries handling molybdenum oxide. Overall, the use of a Molybdenum Oxide Material Handling Conveyor contributes to a more streamlined, sustainable, and productive industrial process.
Conclusion and Company Profile
In summary, a Molybdenum Oxide Material Handling Conveyor is a critical piece of equipment for industries dependent on molybdenum oxide. Its design principles focus on efficiency, safety, and durability, ensuring reliable material transport. The system is composed of specialized components that work together to handle the unique properties of molybdenum oxide. The applications of this conveyor span multiple industries, from chemical manufacturing to steel production, highlighting its versatility and importance. The advantages of using such a conveyor include improved efficiency, enhanced safety, and cost savings. Shandong HeadPowder Engineering Co., Ltd., located in Shandong, China, specializes in the design and manufacturing of these advanced conveyor systems, providing tailored solutions to meet the specific needs of their clients. The company's commitment to quality and innovation ensures that their Molybdenum Oxide Material Handling Conveyors deliver optimal performance and contribute to the success of industrial operations worldwide.




