When it comes to industrial material handling, especially for bulk materials like sodium bicarbonate, specialized conveyor systems are essential for efficient processing and transportation. This article delves into the concept of a sodium bicarbonate material handling conveyor, exploring its design principles and the key factors that make it an effective solution in various industrial applications.
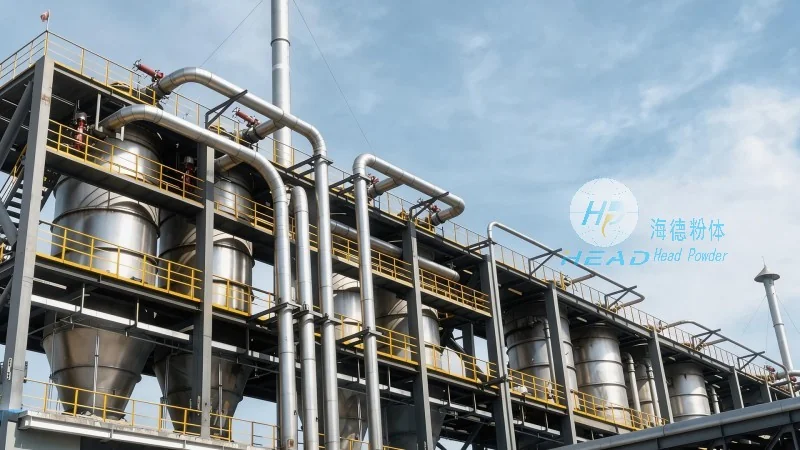
Introduction to Sodium Bicarbonate Material Handling Conveyors
A sodium bicarbonate material handling conveyor is a specialized piece of equipment designed to transport sodium bicarbonate, a common chemical compound used in food, pharmaceutical, and industrial processes. These conveyors are engineered to handle the unique properties of sodium bicarbonate, such as its granular or powder form, ensuring smooth and reliable movement from one point to another within a production facility. The system typically integrates components like feeders, belts, or screw conveyors, tailored to the specific characteristics of the material to minimize segregation, caking, or degradation during transport.
Understanding the Core Components and Functionality
The effectiveness of a sodium bicarbonate material handling conveyor relies on its core components, each playing a critical role in the overall operation. Key elements include the feeding mechanism, which evenly distributes the material onto the conveyor belt or screw, the conveyor itself (whether belt, chain, or screw type), and the control systems that regulate speed, direction, and material flow. For sodium bicarbonate, which can be prone to bridging or sticking, advanced feeding technologies like vibratory feeders or rotary valves are often incorporated to ensure consistent and uniform material delivery. The conveyor's design also considers factors like material flow rate, load capacity, and the need for gentle handling to preserve the product's quality and prevent contamination.
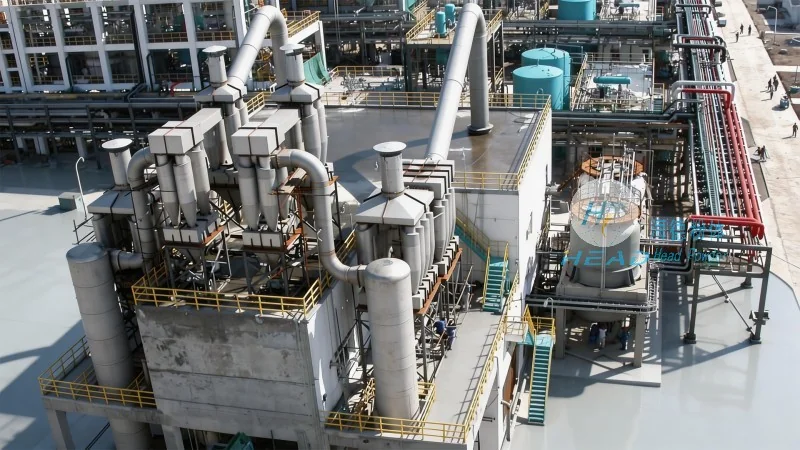
Design Principles Behind the Conveyor System
The design principles of a sodium bicarbonate material handling conveyor are centered on optimizing efficiency, durability, and material integrity. One primary principle is the minimization of material degradation, which is achieved through gentle handling and controlled speed. The conveyor's surface material, such as food-grade stainless steel or polyurethane, is chosen to prevent chemical reactions with sodium bicarbonate and to facilitate easy cleaning. Another key principle is the prevention of product segregation, where different particle sizes or densities are separated during transport. This is addressed through the use of inclined or horizontal conveyor designs, along with internal baffles or mixing elements that maintain a uniform mixture. Additionally, the system is designed for easy maintenance and cleaning, with removable components and access points that allow for thorough sanitation, which is crucial in industries like food and pharmaceuticals where hygiene standards are stringent.
Application Scenarios and Operational Efficiency
Sodium bicarbonate material handling conveyors are widely used in various industrial settings, from food processing plants to chemical manufacturing facilities. In food production, they are essential for transporting baking soda into mixing lines or packaging stations, ensuring consistent quality and preventing cross-contamination. In pharmaceutical applications, the conveyors are used to move sodium bicarbonate into processing lines, where it is used as an excipient or active ingredient in formulations. The operational efficiency of these systems is critical, as they help reduce labor costs, minimize material loss, and improve overall production throughput. By automating the material handling process, these conveyors enable manufacturers to scale their operations while maintaining high standards of product quality and safety.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
At the heart of high-quality sodium bicarbonate material handling solutions is Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer and supplier of industrial conveyor systems. With years of experience in the field, HeadPowder specializes in designing and producing customized conveyor solutions tailored to the specific needs of their clients. The company's commitment to innovation and quality has earned them a reputation for delivering reliable, efficient, and durable equipment that meets the stringent requirements of various industries. HeadPowder's team of engineers and technicians work closely with clients to understand their operational challenges and develop tailored solutions that enhance productivity and reduce downtime.
Address and Location
HeadPowder is headquartered in Shandong, China, with a dedicated facility that houses research and development, manufacturing, and quality control operations. The company's location in Shandong provides easy access to key markets and logistics networks, enabling them to deliver products efficiently to clients worldwide. The facility is equipped with state-of-the-art equipment and adheres to international quality standards, ensuring that every product leaves the factory meeting the highest specifications. HeadPowder's presence in Shandong underscores its commitment to excellence and its role as a trusted partner in the industrial material handling sector.




