Potash, a vital nutrient for modern agriculture, is often delivered in powdered form due to its fine particle size and high solubility. However, efficiently transporting these fine powders from storage to processing or application sites requires specialized equipment. This is where potash powder conveying systems come into play, designed to handle the unique challenges of moving such materials with precision and reliability. Understanding the components and design principles behind these systems is crucial for optimizing agricultural operations and ensuring the safe, efficient movement of potash.
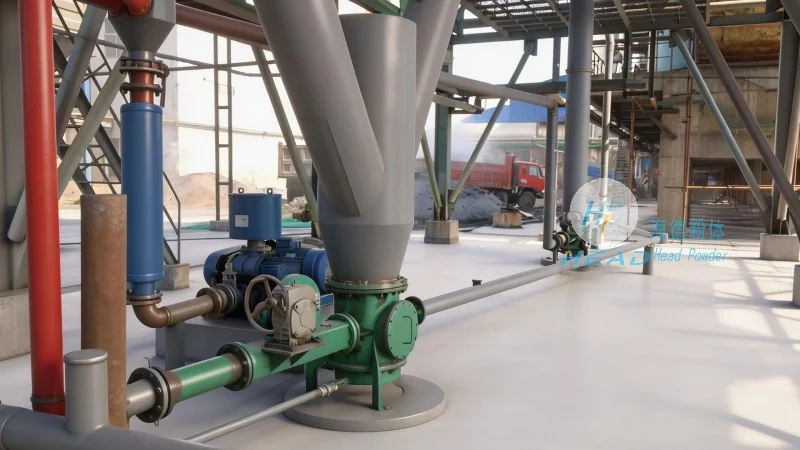
Key Components of a Potash Powder Conveying System
A typical potash powder conveying system consists of several interconnected components, each playing a critical role in the overall operation. The primary components include:
- Potash Material Hopper: A storage vessel designed to hold bulk potash powder. It often features a sloped bottom to facilitate material flow and may include a discharge valve or rotary valve to control the release of material into the conveying system.
- Feeder Device: This component regulates the flow rate of potash from the hopper. Common types include rotary feeders, vibratory feeders, or screw feeders, which ensure a consistent and controlled feed into the conveying line. For potash, a feeder that minimizes material degradation and maintains a stable flow rate is essential.
- Conveying Pipeline: The pipeline transports the potash powder through the system. It is typically made of materials resistant to corrosion and abrasion, such as stainless steel or special alloys, to withstand the chemical and physical stresses of potash particles.
- Conveying Equipment: The core of the system, this equipment can be either pneumatic (air-driven) or mechanical. Pneumatic systems use compressed air to move the powder, while mechanical systems rely on positive displacement or other mechanisms. For potash, pneumatic systems are often preferred due to their ability to handle fine powders and minimize dust generation.
- Control Valves and Regulators: These components manage the pressure, flow, and direction of the conveying medium (air or material). They ensure the system operates within safe and efficient parameters, preventing overpressure or underflow conditions.
- Dust Collection and Filtration: To maintain environmental safety and operational efficiency, dust collection systems are integrated. These may include cyclones, baghouses, or other filtration technologies to capture and remove airborne potash particles, reducing health hazards and preventing material loss.
Design Principles for Efficient Potash Powder Handling
The design of a potash powder conveying system is guided by several key principles to ensure optimal performance, safety, and longevity. These principles address the unique properties of potash powder, such as its fine particle size, high density, and potential for static electricity.
1. Material Compatibility: The system components must be compatible with potash's chemical and physical characteristics. For instance, stainless steel or corrosion-resistant alloys are chosen for pipelines and hoppers to prevent chemical reactions with the fertilizer. Additionally, materials that do not generate static electricity are preferred to avoid sparks, which could be hazardous in an environment with flammable air-powder mixtures.
2. Airflow and Pressure Management: Pneumatic conveying systems rely on precise airflow and pressure control. The design must consider the particle size distribution and density of the potash to determine the appropriate air velocity and pressure levels. Proper pressure management ensures that the powder is transported without clogging or excessive wear on components.
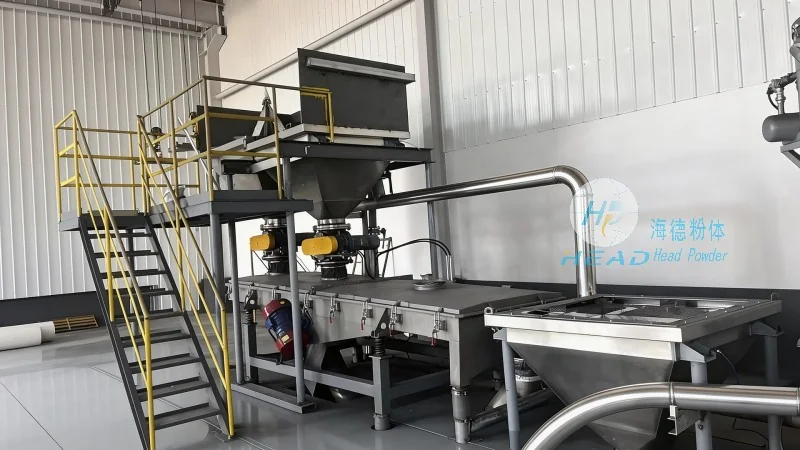
3. Flow Uniformity and Consistency: Consistent material flow is critical to prevent system inefficiencies or blockages. The feeder device and hopper design are optimized to maintain a steady flow rate, which is essential for downstream processing or application equipment. This uniformity also reduces the risk of overloading or underloading the conveying system.
4. Dust Control and Environmental Safety: Potash powders are fine and can easily become airborne, posing health risks and environmental concerns. The design incorporates dust collection and filtration systems to capture and contain particles. These systems are often integrated with the conveying pipeline and are designed to meet regulatory standards for air quality and occupational safety.
5. System Scalability and Customization: Potash operations vary in scale and application requirements. The conveying system design must be flexible and scalable to accommodate different production volumes and operational needs. Customization allows for the integration of specific features, such as variable speed drives or automated control systems, to enhance efficiency and adaptability.
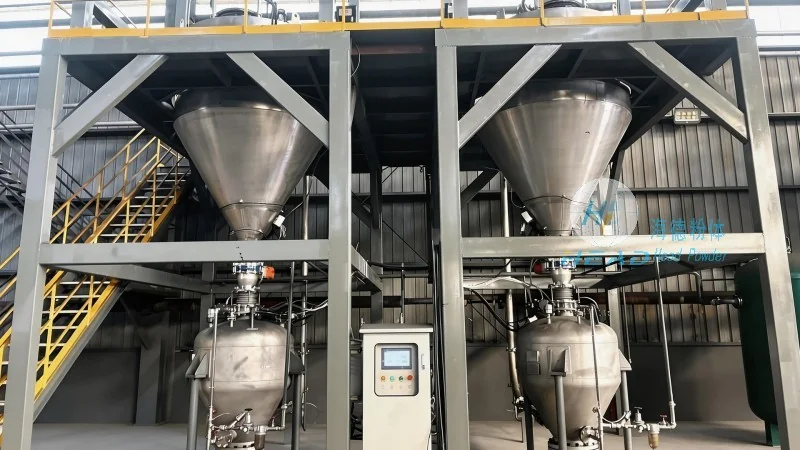
How Shandong HeadPowder Engineering Co., Ltd. Enhances Potash Powder Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of powder handling solutions, specializes in designing and manufacturing potash powder conveying systems tailored to the unique needs of agricultural and industrial clients. With years of experience in the field, the company understands the critical role of efficient potash handling in optimizing agricultural productivity and ensuring operational safety.
The company's approach to potash powder conveying systems focuses on integrating advanced engineering principles with practical application. By leveraging their expertise in material science and fluid dynamics, Shandong HeadPowder engineers develop systems that address the specific challenges of potash, such as its fine particle size and potential for static buildup.
Key features of their potash powder conveying solutions include:
- Advanced Feeder Technology: The company utilizes high-quality rotary or vibratory feeders that are specifically designed for potash. These feeders ensure consistent material flow, minimize degradation, and reduce the risk of blockages, even with varying potash compositions.
- Corrosion-Resistant Materials: All components, including pipelines and hoppers, are constructed from corrosion-resistant materials like stainless steel or specialized alloys. This ensures long-term durability and prevents contamination of the potash, which is crucial for maintaining product quality.
- Integrated Dust Control: Shandong HeadPowder integrates state-of-the-art dust collection systems into their designs. These systems are engineered to capture and filter fine potash particles, ensuring compliance with environmental regulations and protecting the health of workers.
- Customized System Design: Recognizing that each potash operation is unique, the company offers customized solutions. They work closely with clients to understand their specific requirements, such as production volume, material characteristics, and operational constraints, and tailor the conveying system accordingly.
- Reliability and Maintenance: The systems are designed for minimal maintenance and high reliability. Components are selected for durability, and the overall system is engineered to operate efficiently over extended periods, reducing downtime and operational costs.
By combining these design principles and features, Shandong HeadPowder Engineering Co., Ltd. provides potash powder conveying systems that enhance operational efficiency, ensure product quality, and promote environmental safety. Their expertise in powder handling technology makes them a trusted partner for agricultural and industrial clients seeking reliable and effective potash transportation solutions.




