Beer brewery pelletized waste powder conveying refers to the process of transporting the pelletized waste material from beer brewing operations. This material, often referred to as beer brewery pelletized waste, is a byproduct of the brewing process. The efficient handling of this waste is crucial for maintaining operational efficiency and ensuring compliance with environmental regulations. Understanding the mechanisms and design principles behind this type of material handling is essential for breweries seeking to optimize their waste management systems.
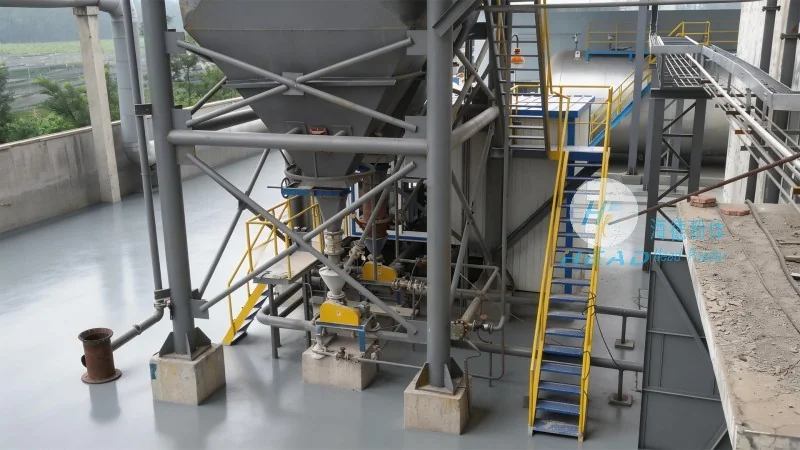
Understanding the Core Components of Beer Brewery Pelletized Waste Powder Conveying
At the heart of beer brewery pelletized waste powder conveying are several key components that work in tandem to ensure effective material transport. The primary components include the source of the waste material, which is typically the pelletized waste from the brewing process. This material is often in a dry, powdery form after being processed through drying and pelletizing steps. The conveying system then uses various mechanisms such as pneumatic conveying, mechanical screw conveyors, or belt conveyors to move the material from one location to another within the brewery or to off-site disposal facilities.
The Design Principles Behind Efficient Beer Brewery Pelletized Waste Powder Conveying Systems
Designing an effective beer brewery pelletized waste powder conveying system involves several critical principles that ensure reliability, efficiency, and minimal material loss. One of the fundamental principles is the selection of the appropriate conveying method based on the characteristics of the waste material. For instance, if the material is fine and dry, pneumatic conveying systems may be more suitable due to their ability to handle low-density powders without the need for mechanical contact. Conversely, if the material contains larger particles or has a higher moisture content, mechanical conveyors like screw or belt conveyors might be preferred to prevent blockages and ensure consistent flow.
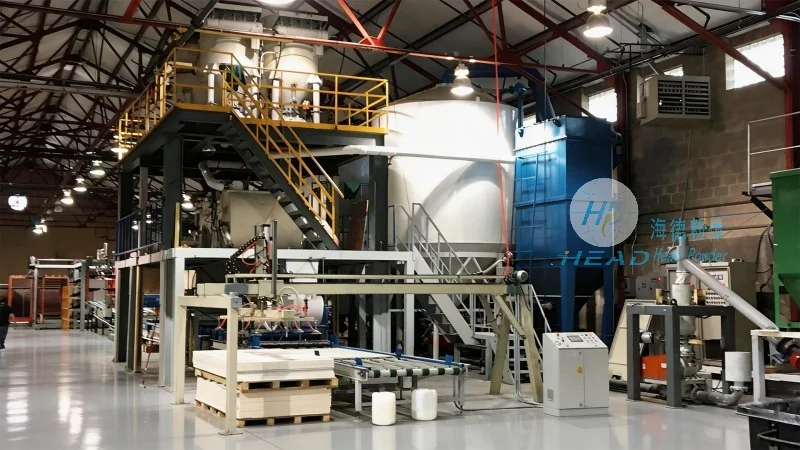
Key Factors Influencing the Performance of Beer Brewery Pelletized Waste Powder Conveying Systems
Several factors play a significant role in determining the performance of beer brewery pelletized waste powder conveying systems. The first is the particle size and density of the waste material. Smaller particles can lead to higher friction and potential for dust generation, which may require additional dust control measures. The second factor is the distance and elevation changes between the source and destination of the material. Longer distances or significant vertical lifts may necessitate more powerful conveying equipment or additional booster sections to maintain material flow. Third, the system's capacity requirements are critical, as the conveying rate must match the production volume of the brewery to avoid bottlenecks or overloading the system. Finally, the need for dust control and environmental compliance is a key consideration, as many breweries are subject to regulations regarding air quality and waste disposal.
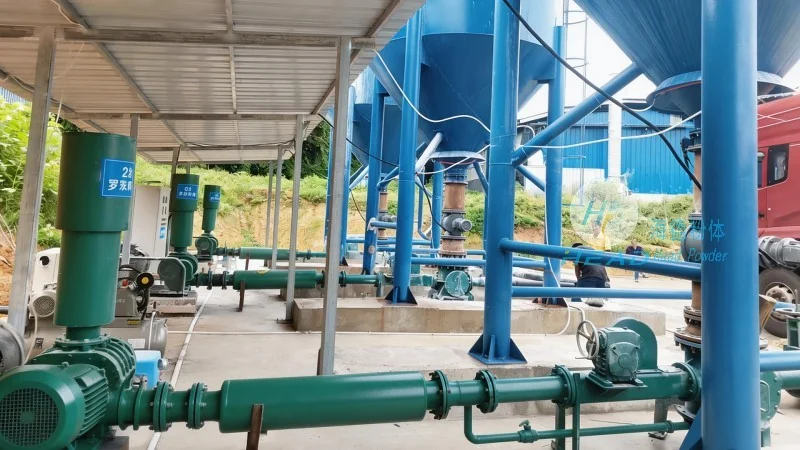
How Shandong HeadPowder Engineering Co., Ltd. Addresses Beer Brewery Pelletized Waste Powder Conveying Challenges
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for material handling, specializes in designing and implementing efficient beer brewery pelletized waste powder conveying systems. With a focus on tailored solutions that meet the specific needs of breweries, the company leverages its expertise in pneumatic and mechanical conveying technologies to deliver reliable and cost-effective systems. The company's approach involves a thorough analysis of the brewery's waste characteristics, production volume, and operational requirements to design a system that optimizes material transport while minimizing downtime and maintenance costs. By incorporating advanced materials and engineering principles, HeadPowder ensures that its conveying systems are durable, efficient, and compliant with industry standards and environmental regulations.
Conclusion: The Importance of Effective Beer Brewery Pelletized Waste Powder Conveying
Efficient beer brewery pelletized waste powder conveying is a critical aspect of modern brewing operations, impacting both operational efficiency and environmental responsibility. By understanding the design principles and key factors that influence system performance, breweries can select and implement the most appropriate conveying solutions. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing the technical expertise and engineering solutions needed to address the unique challenges of beer brewery waste handling. As breweries continue to prioritize sustainability and operational excellence, the importance of reliable and efficient powder conveying systems will only grow, making it essential for industry professionals to stay informed about the latest advancements in this field.




