For professionals in the brewing industry, understanding the technology behind efficient malt handling is crucial. Malt pneumatic conveying equipment represents a sophisticated solution for transporting malt, a key ingredient in beer production. This article delves into the structure and operational principles of such systems, highlighting how they enhance process efficiency and reliability.
Overview of Malt Pneumatic Conveying Systems
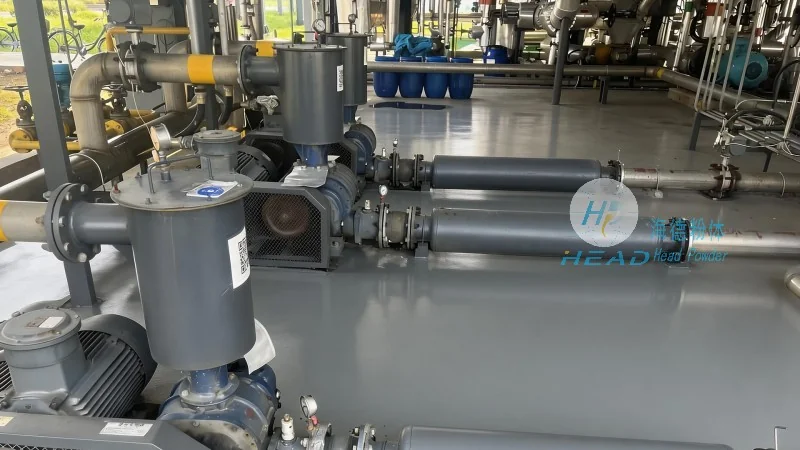
Malt pneumatic conveying equipment is designed to transport malt powder or granules through a closed system using compressed air or vacuum. Unlike traditional mechanical conveyors, these systems rely on air flow to move material, offering advantages like reduced contamination, minimal product degradation, and the ability to handle sensitive materials like malt without mechanical friction. The core components of a typical malt pneumatic conveying system include the feeding unit, conveying pipeline, air source, and separation or discharge equipment. Each component plays a critical role in ensuring smooth and effective material transport.
Key Structural Components and Their Functions
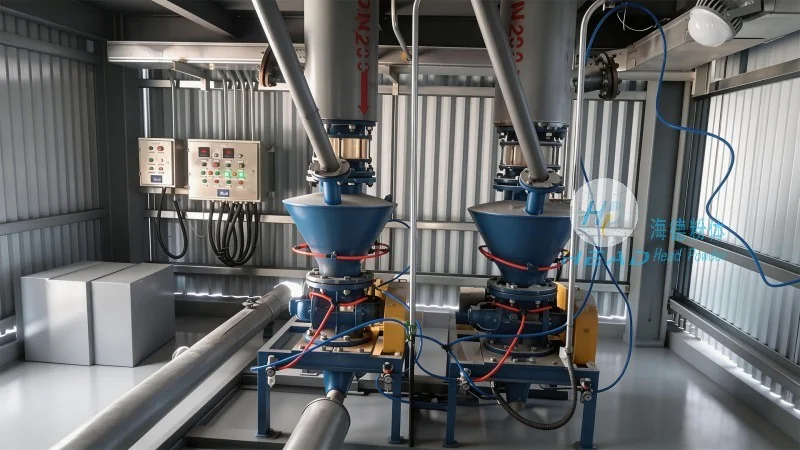
The feeding unit is responsible for introducing malt into the conveying system. This may involve a hopper with a rotary valve or a screw feeder, which controls the flow rate and prevents material buildup. The conveying pipeline, often made of stainless steel or other corrosion-resistant materials, is designed to withstand the pressure and temperature of the air-malt mixture. The air source, typically a blower or compressor, generates the necessary airflow to move the malt through the pipeline. The separation or discharge equipment, such as cyclones or filters, separates the malt from the air at the end of the conveying line, ensuring clean material collection.
Operational Principles: How Pneumatic Conveying Works
The fundamental principle of pneumatic conveying is the use of air to create a flow that lifts and transports the malt particles. In pressure systems, compressed air is introduced at the start of the pipeline, pushing the malt forward. In vacuum systems, a vacuum is created at the discharge end, drawing the malt through the pipeline. The velocity of the air and the size of the particles determine the type of system used—coarse particles may require higher air velocities for effective transport. The design of the system must consider factors like malt density, moisture content, and particle size to optimize performance and prevent blockages or degradation.
Benefits of Using Malt Pneumatic Conveying Equipment
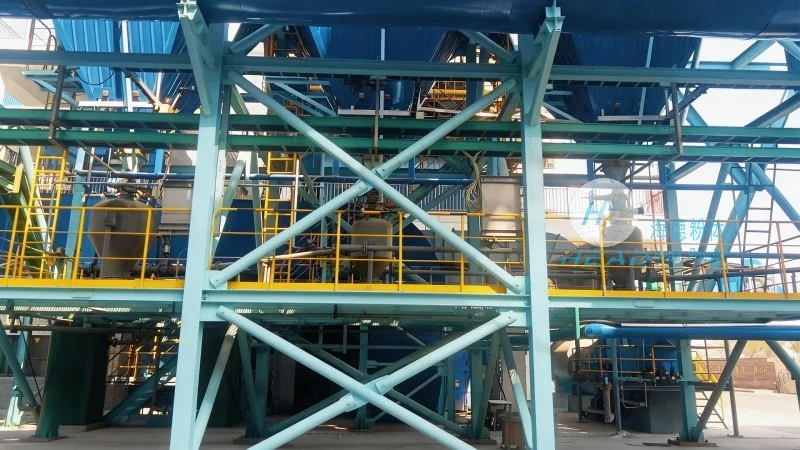
Implementing malt pneumatic conveying equipment offers several benefits for breweries. These systems reduce labor costs by automating the transport process, minimize product loss and contamination compared to manual handling, and improve overall process control. Additionally, the enclosed design prevents dust and odors from escaping, enhancing workplace safety and compliance with environmental regulations. For malt processors, the efficiency and reliability of pneumatic conveying systems contribute to consistent product quality and reduced downtime.
About HeadPowder: A Leading Manufacturer in Powder Handling Solutions
HeadPowder, a division of Shandong HeadPowder Engineering Co., Ltd., specializes in designing and manufacturing advanced pneumatic conveying equipment tailored to the needs of the brewing and food processing industries. With facilities located in Shandong, China, HeadPowder leverages years of experience to develop customized solutions that meet the unique requirements of malt handling. The company’s commitment to quality and innovation ensures that their equipment delivers reliable performance, long service life, and minimal maintenance. By partnering with HeadPowder, breweries can enhance their operational efficiency and maintain the highest standards of product quality in malt processing.




