HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and development of advanced negative pressure pneumatic conveying systems tailored for crystalline materials. This equipment is engineered to efficiently transport bulk crystalline substances with precision and reliability, addressing the unique challenges associated with handling such materials in industrial applications.
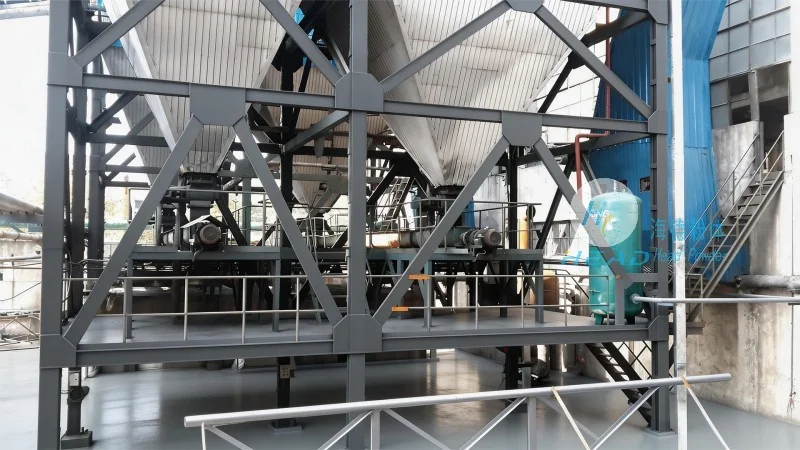
Key Features and Technical Advantages
The negative pressure pneumatic conveying equipment from HeadPowder is designed with several key features that enhance performance and operational efficiency. One of the primary advantages is the ability to maintain a consistent negative pressure environment, which prevents dust emissions and ensures a clean working environment. The system utilizes high-efficiency airlocks and rotary valves to control material flow, minimizing product degradation and ensuring product integrity throughout the conveying process. Additionally, the equipment is equipped with advanced control systems that allow for real-time monitoring and adjustment of conveying parameters, optimizing energy consumption and reducing operational costs.
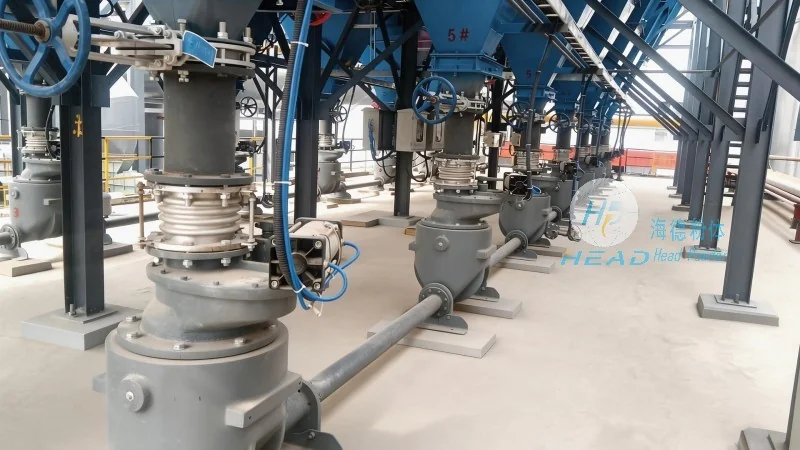
Application Scenarios and Material Compatibility
HeadPowder's negative pressure pneumatic conveying systems are versatile and suitable for a wide range of crystalline materials, including but not limited to pharmaceutical powders, food additives, chemical reagents, and industrial minerals. The system's design accommodates various particle sizes and moisture content, making it adaptable to different industrial processes. For instance, in pharmaceutical manufacturing, the equipment ensures that sensitive crystalline drugs are transported without contamination or degradation, meeting stringent quality standards. In the food industry, the system maintains hygiene and prevents cross-contamination, aligning with food safety regulations. The flexibility of the system also makes it suitable for chemical processing plants, where it efficiently handles reactive or corrosive crystalline materials while protecting equipment and personnel.
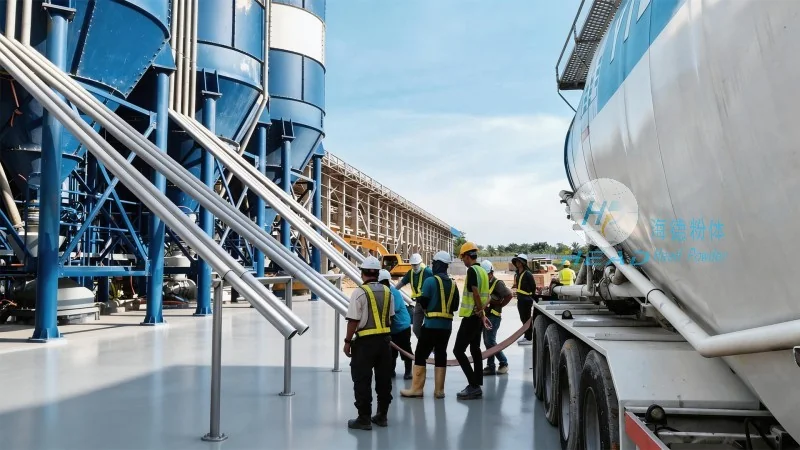
Engineering and Customization Capabilities
HeadPowder Engineering Co., Ltd. offers comprehensive engineering services to customize negative pressure pneumatic conveying solutions according to specific customer requirements. The company's team of experienced engineers works closely with clients to assess their operational needs, process parameters, and material characteristics to design a tailored system. This includes selecting appropriate air volumes, pressure differentials, and equipment components that ensure optimal performance. The engineering process also incorporates considerations for material handling efficiency, energy consumption, and maintenance requirements, resulting in a system that meets both functional and economic objectives. HeadPowder's commitment to quality and innovation ensures that each customized solution is built to withstand the demands of industrial environments and provide long-term reliability.
Operational Benefits and Efficiency
The implementation of HeadPowder's negative pressure pneumatic conveying equipment brings significant operational benefits to industrial facilities. By eliminating the need for traditional mechanical conveying methods, such as belt conveyors or screw conveyors, the system reduces equipment wear and maintenance costs. The negative pressure design also minimizes dust generation, improving workplace safety and compliance with environmental regulations. Furthermore, the system's ability to handle materials at high speeds and over long distances enhances overall production throughput, increasing operational efficiency. The advanced control systems allow for automated operation, reducing the need for manual intervention and minimizing human error. This leads to consistent product quality and reduced downtime, contributing to improved overall productivity.
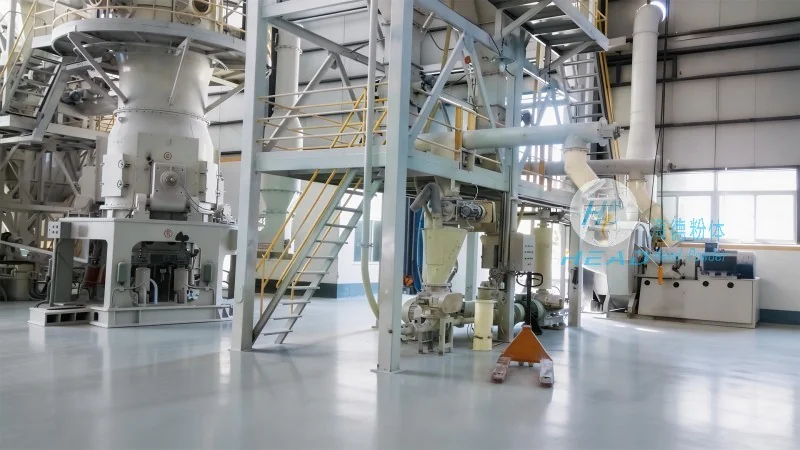
Quality Assurance and Compliance
HeadPowder Engineering Co., Ltd. adheres to strict quality standards in the design, manufacturing, and testing of its negative pressure pneumatic conveying equipment. The company follows international quality management systems, such as ISO 9001, to ensure that all products meet or exceed industry benchmarks. The equipment is rigorously tested under various operating conditions to verify performance, durability, and safety. This includes testing for material flow rates, pressure differentials, and air consumption to ensure that the system operates within specified parameters. Additionally, the company complies with relevant environmental regulations, ensuring that the equipment is designed to minimize environmental impact and meet sustainability goals. The quality assurance process also involves regular inspections and maintenance checks to ensure that the equipment remains in optimal condition throughout its service life.




