HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems for stone aggregate powders. The equipment is engineered to efficiently transport bulk materials like stone aggregates through an air-based system, ensuring reliable and low-maintenance operation in various industrial applications. This article delves into the operational process and underlying principles of such systems, highlighting their efficiency and practicality for material handling needs.
Key Components of the Pneumatic Conveying System
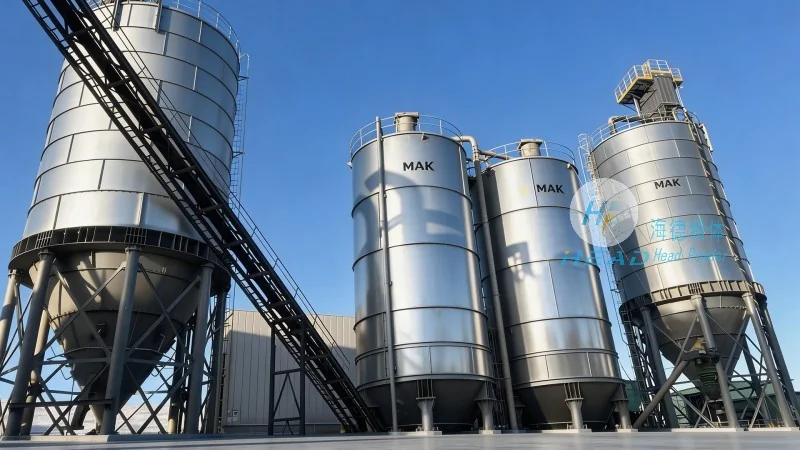
The pneumatic conveying equipment for stone aggregate powders typically consists of several critical components that work in tandem to facilitate material transport. These include a material hopper for storage, a blower or compressor to generate air pressure, a pipeline network for material and air flow, a control system for operation, and a discharge unit for material release. Each component plays a vital role in ensuring the smooth and efficient movement of the stone aggregate powder from the source to the destination. The material hopper is designed to hold the bulk stone aggregate, providing a consistent feed to the system. The blower or compressor generates the necessary air pressure, which is then introduced into the pipeline to create a flow that carries the powder particles. The pipeline network, often made of durable materials like stainless steel or high-density polyethylene, ensures the material is transported without blockages or degradation. The control system allows operators to monitor and adjust the air pressure, flow rate, and other parameters to optimize performance. Finally, the discharge unit, such as a rotary valve or a dust collector, manages the release of the stone aggregate powder at the receiving end, preventing dust and ensuring a clean operation.
Operation Process of the Pneumatic Conveying Equipment
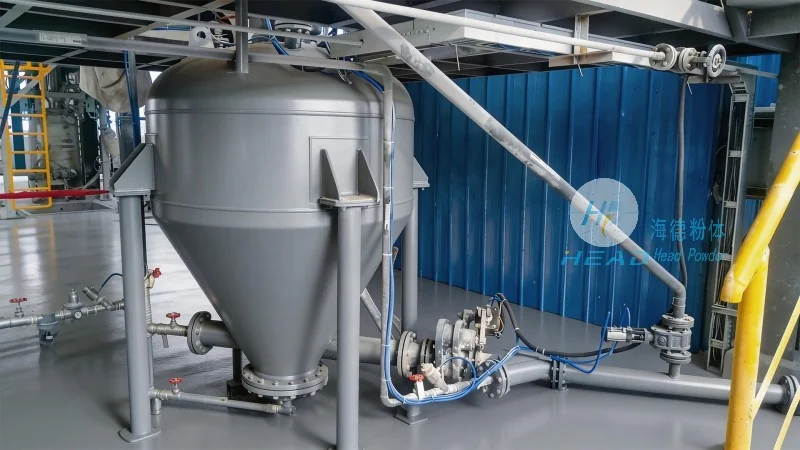
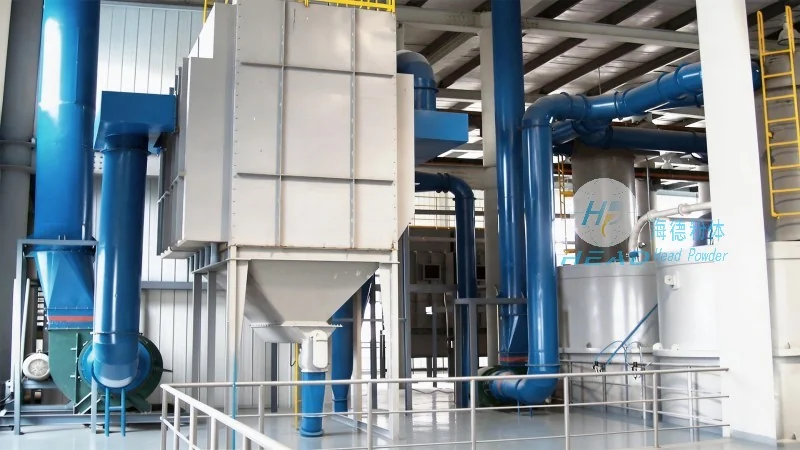
The operation of the stone aggregate powder pneumatic conveying system follows a systematic process that ensures efficient material transport. The process begins with the loading of the stone aggregate into the material hopper. The hopper is equipped with a feeding mechanism, such as a screw feeder or a rotary valve, which regulates the flow of material into the pipeline. Simultaneously, the blower or compressor starts operating, generating the required air pressure. The air is then introduced into the pipeline, creating a positive pressure environment that lifts the stone aggregate powder particles and propels them through the system. As the material travels through the pipeline, it is mixed with the air, forming a dense flow that moves towards the discharge point. The control system continuously monitors the pressure and flow rates, adjusting the blower speed or feed rate as needed to maintain optimal performance. At the receiving end, the discharge unit separates the stone aggregate powder from the air, typically using a cyclone separator or a bag filter. The purified air is then released back into the environment, while the stone aggregate powder is collected in a storage bin or directly to the processing equipment. This entire process is designed to be continuous and automated, minimizing manual intervention and maximizing throughput.
Working Principle of the Pneumatic Conveying System
The working principle of the stone aggregate powder pneumatic conveying equipment is based on the fundamental concept of fluidization and air transport. The system utilizes compressed air to create a flow that carries the solid particles of the stone aggregate. The key principle is that the air pressure in the pipeline is sufficient to overcome the gravitational force acting on the powder particles, allowing them to be lifted and transported. The velocity of the air flow is critical; it must be high enough to keep the particles suspended but not so high as to cause excessive wear on the pipeline or equipment components. The system operates under either positive pressure or negative pressure, depending on the application. Positive pressure systems, where the pipeline is pressurized above atmospheric pressure, are commonly used for long-distance or high-capacity transport. Negative pressure systems, where the pipeline is under vacuum, are often used for short-distance or dusty applications. The choice of system depends on factors such as the distance between the source and destination, the material characteristics, and the environmental requirements. The efficiency of the system is also influenced by the particle size and density of the stone aggregate. Smaller particles may require higher air velocities to maintain suspension, while larger particles may need higher air pressure to overcome their weight. The design of the equipment, including the hopper geometry, pipeline diameter, and blower capacity, is optimized to match the specific material characteristics and operational requirements, ensuring reliable and efficient performance.
Advantages of Using Pneumatic Conveying for Stone Aggregate Powders
Employing pneumatic conveying systems for stone aggregate powders offers several advantages over traditional methods like belt conveyors or bucket elevators. One of the primary benefits is the ability to transport materials in a closed system, which significantly reduces dust emissions and improves workplace safety. This is particularly important for stone aggregates, which can be abrasive and generate fine particles that are harmful to workers and the environment. The closed system also prevents contamination of the material, ensuring that the stone aggregate remains clean and free from external particles. Another advantage is the flexibility of the system, as it can be easily reconfigured to handle different material types or transport distances. The equipment can be adapted to various industrial settings, from construction sites to manufacturing plants, providing a versatile solution for material handling needs. Additionally, pneumatic conveying systems are generally more energy-efficient compared to other methods, as they use compressed air to transport materials without the need for mechanical components like belts or chains. This results in lower operational costs and reduced maintenance requirements. The system also offers high throughput capabilities, allowing for the efficient transport of large quantities of stone aggregate in a short period. This makes it ideal for applications where large volumes of material need to be moved quickly and reliably.
Applications and Industries Served
The stone aggregate powder pneumatic conveying equipment from HeadPowder is widely used in various industries that require the efficient handling of bulk materials. In the construction industry, the equipment is used to transport stone aggregates from storage silos to mixing plants or concrete batching stations. This ensures a consistent supply of materials, improving the quality and efficiency of concrete production. The equipment is also used in the mining industry to transport crushed stone or sand from processing facilities to storage areas or shipping points. In the chemical industry, it can be used to convey fine stone aggregates used as fillers or additives in various products. Additionally, the equipment is utilized in the food and pharmaceutical industries, where the closed system helps maintain hygiene and prevent contamination. The versatility of the system makes it suitable for a wide range of applications, from small-scale operations to large industrial plants. HeadPowder's equipment is designed to meet the specific needs of each industry, ensuring optimal performance and reliability in diverse environments.




