Efficient and reliable transportation of powdered materials like bentonite powder is a critical aspect of many industrial processes. Pneumatic conveying systems offer a solution by utilizing air flow to move these fine particles from one location to another. This method not only enhances operational efficiency but also reduces the risk of material contamination and dust exposure. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing advanced pneumatic conveying solutions tailored to the unique needs of bentonite powder handling.
Understanding Pneumatic Conveying Systems
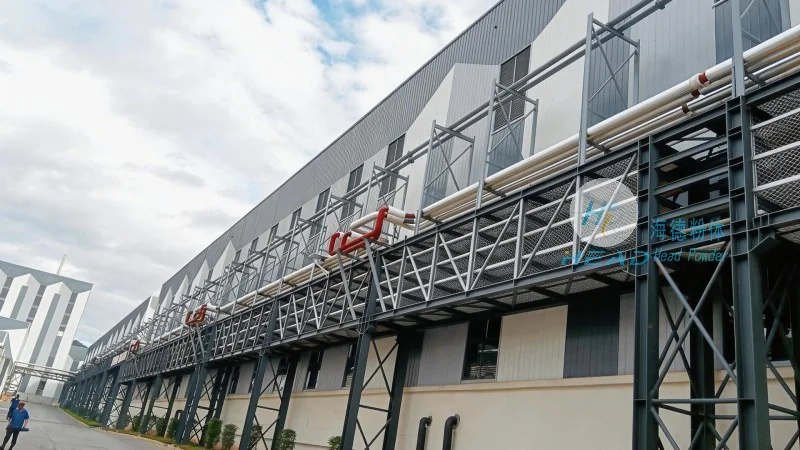
Pneumatic conveying systems operate by creating a pressure differential that propels the powder through a pipeline using compressed air. There are two primary types: dilute phase and dense phase. Dilute phase systems are suitable for high-volume, low-density materials and operate at relatively high velocities, while dense phase systems are ideal for sensitive or abrasive powders, operating at lower velocities to minimize particle degradation. For bentonite powder, which is often fine and can be prone to agglomeration, a well-designed dilute phase system with appropriate air-to-material ratios is typically recommended. The system components include a material feed hopper, a conveyor line, a receiver, and a dust collector. The feed hopper ensures a consistent material supply, while the conveyor line transports the powder through the pipeline. The receiver collects the material at the destination, and the dust collector captures any airborne particles to maintain air quality and comply with environmental regulations.
Key Factors in Designing an Efficient System
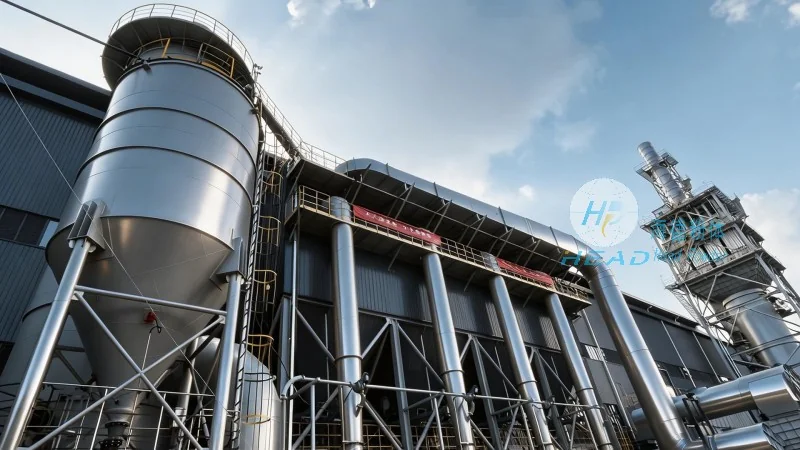
The success of a pneumatic conveying system for bentonite powder depends on several key factors. First, the air flow rate and pressure must be optimized to match the material's characteristics. Bentonite powder has a specific density and particle size distribution, which influence the required air velocity to prevent blockages and ensure smooth transport. Second, the pipeline design is crucial. The use of smooth, corrosion-resistant materials like stainless steel or PTFE-lined pipes minimizes friction and reduces the risk of material buildup. Additionally, the inclusion of bends and fittings with minimal pressure loss is essential to maintain system efficiency. Third, the system's control mechanisms play a vital role. Automated controls allow for real-time monitoring of pressure, flow, and material levels, enabling quick adjustments to maintain optimal performance. This is particularly important in industrial settings where production rates and material quality are critical.
Benefits of Pneumatic Conveying for Bentonite Powder
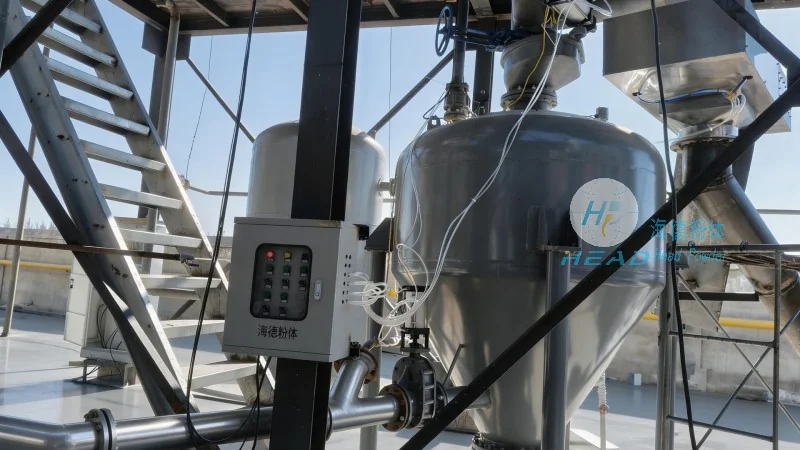
Implementing a pneumatic conveying system for bentonite powder offers numerous benefits. One of the most significant advantages is the reduction in manual handling, which minimizes the risk of product contamination and improves workplace safety. The enclosed system also prevents dust from spreading, enhancing air quality and compliance with occupational health standards. Furthermore, pneumatic conveying systems can be integrated with other processing equipment, such as mixing or blending units, to create a seamless production line. This integration increases overall operational efficiency and reduces downtime. Another benefit is the ability to transport bentonite powder over long distances without the need for intermediate storage or transfer points, which simplifies the logistics of material movement. The system's flexibility also allows for easy adjustments to accommodate changes in production volume or material type, making it a versatile solution for various industrial applications.
Case Study: Successful Implementation by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. has successfully implemented pneumatic conveying systems for bentonite powder in several industrial projects. For example, a customer in the paper industry required a system to transport bentonite powder from a storage silo to a blending unit. The company designed a dilute phase system with a 100 mm diameter pipeline and a 0.5 MPa air pressure system. The system was equipped with automated controls and a dust collector to ensure compliance with local environmental regulations. The result was a 30% increase in production efficiency and a significant reduction in labor costs associated with manual handling. Another case involved a customer in the pharmaceutical industry, where the system was used to transport bentonite powder to a coating line. The system was designed with a dense phase configuration to prevent particle degradation, and the enclosed design ensured product purity. The customer reported improved product quality and reduced waste due to the efficient transport process.
Conclusion and Recommendations
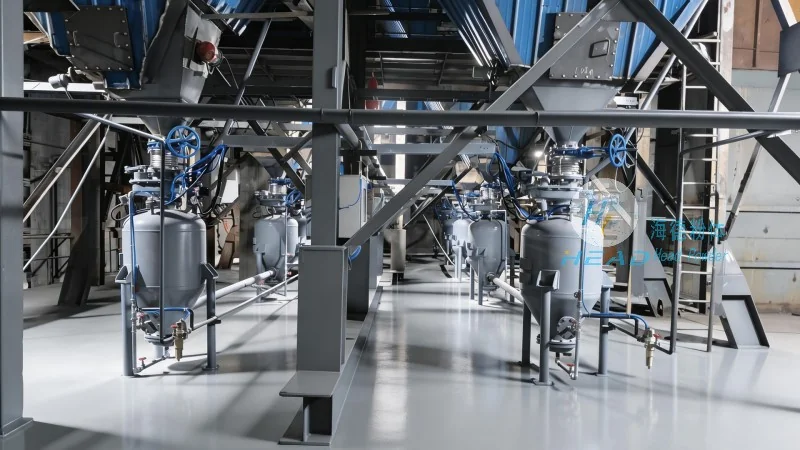
Pneumatic conveying is an effective and efficient method for transporting bentonite powder and other fine powdered materials. By understanding the key factors in system design, such as air flow rate, pipeline design, and control mechanisms, industries can achieve optimal performance and operational benefits. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions tailored to the specific needs of bentonite powder handling, ensuring reliable and cost-effective material transport. For businesses looking to enhance their production processes and improve material handling efficiency, pneumatic conveying systems offer a robust and versatile solution. By partnering with a specialized provider like Shandong HeadPowder Engineering Co., Ltd., companies can ensure the successful implementation of a system that meets their unique requirements and contributes to overall operational excellence.




