When it comes to transporting bulk materials like wheat bran, the choice between positive pressure and negative pressure pneumatic conveying systems is a critical decision for many industries. Both methods offer distinct advantages and are designed to address specific operational needs. This article provides a detailed comparison of positive pressure and negative pressure conveying systems, focusing on their applications, operational principles, and key differences in performance, efficiency, and cost-effectiveness. The analysis is tailored to the unique characteristics of wheat bran, a material that demands careful handling due to its fine particle size and potential for dust generation.
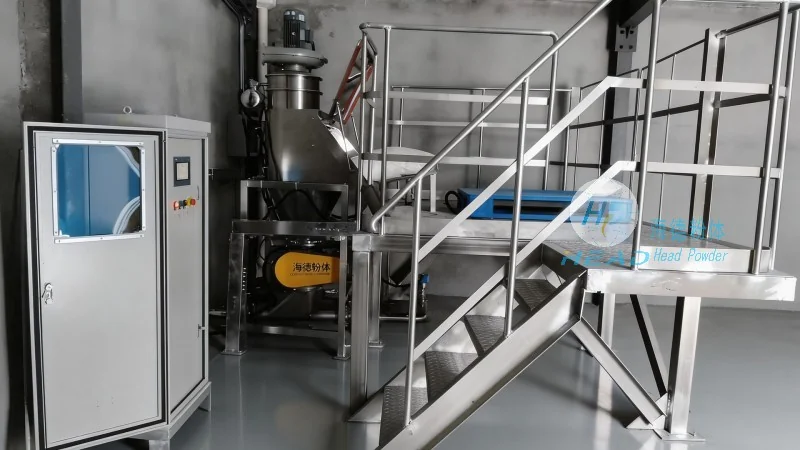
Understanding Pneumatic Conveying Systems
Pneumatic conveying is a method of transporting solid materials using a stream of air or gas. It is widely used in industries such as food processing, pharmaceuticals, and chemical manufacturing due to its ability to handle materials that are difficult to transport by traditional means like belts or trucks. The two primary types of pneumatic conveying systems are positive pressure and negative pressure, each with its own set of characteristics that make it suitable for different scenarios.
Positive Pressure Conveying Systems
Positive pressure conveying systems operate by blowing air or gas into the material to be transported. The system generates a higher pressure inside the conveying line compared to the ambient air pressure. This pressure difference forces the material to move through the pipeline. In the context of wheat bran, positive pressure systems are often preferred for their ability to handle abrasive and fine materials efficiently. The high-pressure air stream can effectively move wheat bran from a storage silo or hopper to a processing unit without the need for complex vacuum equipment.
A key advantage of positive pressure systems is their robustness and ability to handle high material loads. They are less susceptible to clogging and can maintain consistent flow rates even with varying material characteristics. However, they require more energy input to generate the necessary pressure, which can increase operational costs. Additionally, positive pressure systems may generate more noise and require proper ventilation to manage the air exhaust, which can be a concern in enclosed facilities.
Negative Pressure Conveying Systems
Negative pressure conveying systems, also known as vacuum systems, operate by creating a lower pressure inside the conveying line compared to the ambient air pressure. The system draws material into the pipeline using a vacuum pump. For wheat bran, negative pressure systems are often used when the material needs to be transported from a processing area back to a storage silo or when the material is sensitive to high air velocities that could cause dust dispersion.
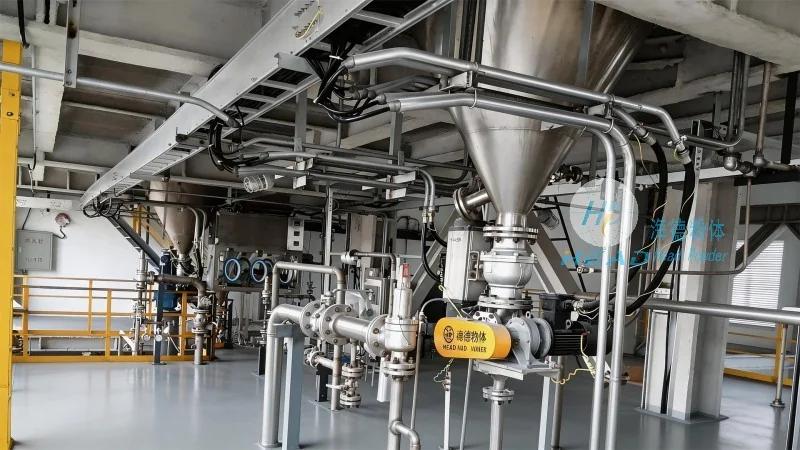
One of the main benefits of negative pressure systems is their ability to handle materials that are prone to dust generation. The lower air velocities and reduced pressure differentials minimize the risk of dust being released into the environment, making them suitable for applications where air quality and safety are paramount. However, negative pressure systems are more prone to clogging and can be less efficient with highly abrasive or sticky materials like some types of wheat bran. They also require more maintenance due to the higher wear on components from the constant vacuum operation.
Key Differences and Performance Comparison
When comparing positive and negative pressure conveying systems for wheat bran, several factors stand out. Positive pressure systems generally offer higher conveying capacities and are more energy-efficient for long-distance transport. They are better suited for handling large volumes of fine materials and can maintain consistent flow rates with minimal variation. Negative pressure systems, on the other hand, excel in applications where dust control and material recovery are critical. They are often used for short-distance transport or when the material needs to be returned to a storage area.
The choice between the two systems often depends on the specific requirements of the wheat bran processing facility. For example, a facility that processes large quantities of wheat bran and requires high throughput may opt for a positive pressure system due to its higher capacity and efficiency. Conversely, a facility that prioritizes environmental compliance and dust control may choose a negative pressure system to minimize air emissions and maintain a clean working environment.
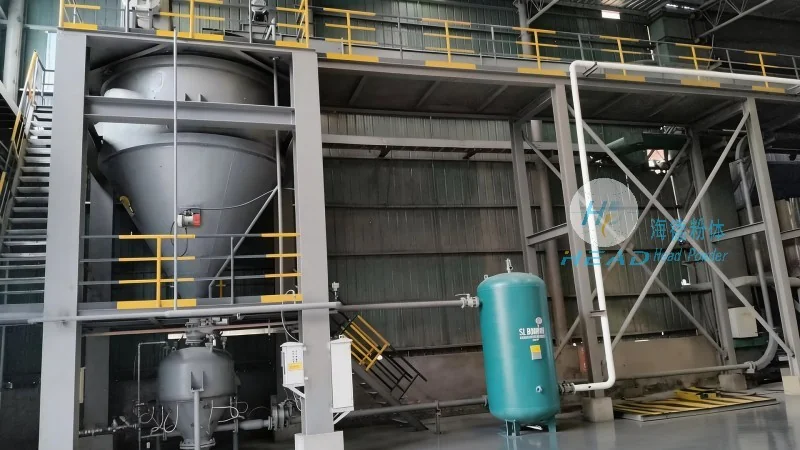
Operational Considerations and Maintenance
Both positive and negative pressure conveying systems require regular maintenance to ensure optimal performance. Positive pressure systems need to check for air leaks, maintain proper air filtration to prevent dust accumulation in the system, and inspect the conveying line for any signs of wear or clogging. Negative pressure systems, while more prone to clogging, require more frequent cleaning of the vacuum pump and filter systems to maintain suction efficiency.
The operational costs of both systems vary based on the energy consumption and maintenance requirements. Positive pressure systems typically have higher initial energy costs due to the need for high-pressure air compressors, but they may have lower maintenance costs as they are less complex. Negative pressure systems, while having lower initial energy costs, may incur higher maintenance expenses due to the wear on vacuum components and the need for more frequent cleaning.
Conclusion
In conclusion, the choice between positive pressure and negative pressure pneumatic conveying systems for wheat bran depends on the specific operational needs of the facility. Positive pressure systems offer higher capacity, efficiency, and robustness, making them ideal for high-volume transport. Negative pressure systems excel in dust control and material recovery, making them suitable for applications where environmental and safety considerations are paramount. By understanding the characteristics of each system and the specific requirements of wheat bran, processing facilities can select the most appropriate conveying method to optimize their operations and ensure efficient material handling.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing customized systems tailored to the unique needs of bulk material handling. With years of experience in the industry, HeadPowder offers advanced solutions that enhance operational efficiency, reduce costs, and improve safety in wheat bran processing applications. The company's expertise in both positive and negative pressure systems allows them to provide comprehensive advice and support to help clients choose the best conveying method for their specific requirements.




