The sulfate potash pneumatic conveying system is a critical piece of industrial equipment designed for the efficient and safe transportation of sulfate potash, a vital raw material in the fertilizer and chemical industries. This system utilizes air as the conveying medium to move bulk materials, offering advantages such as reduced labor costs, minimized material loss, and enhanced operational safety compared to traditional mechanical conveying methods. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in developing and supplying high-quality pneumatic conveying solutions tailored to the specific needs of clients in the agricultural and chemical sectors.
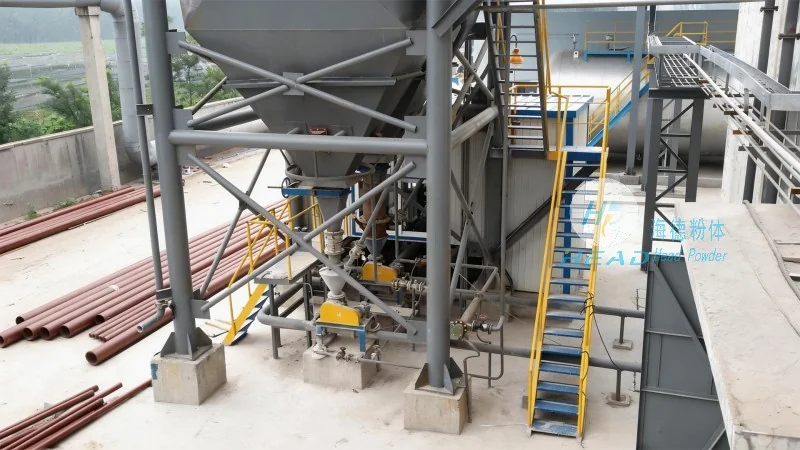
Key Components and Structure of the System
The sulfate potash pneumatic conveying system consists of several key components that work in concert to ensure reliable and efficient material transport. The primary components include a hopper for material storage, a rotary feeder to control the flow rate of the material, a pneumatic conveying pipeline, a filter system to remove dust and particles from the air, and a discharge unit for delivering the material to its final destination. The system is typically designed with a modular structure, allowing for easy installation, maintenance, and scalability to accommodate varying production capacities. The hopper is equipped with a level indicator to monitor the material inventory, while the rotary feeder ensures a consistent and controlled feed rate, preventing overloading or underfeeding of the conveying line. The pneumatic pipeline is constructed from high-quality materials, such as stainless steel or corrosion-resistant alloys, to withstand the chemical properties of sulfate potash and ensure long-term durability. The filter system is crucial for maintaining air quality and protecting downstream equipment from dust accumulation, while the discharge unit is designed to handle the material safely and efficiently, minimizing spillage and contamination.
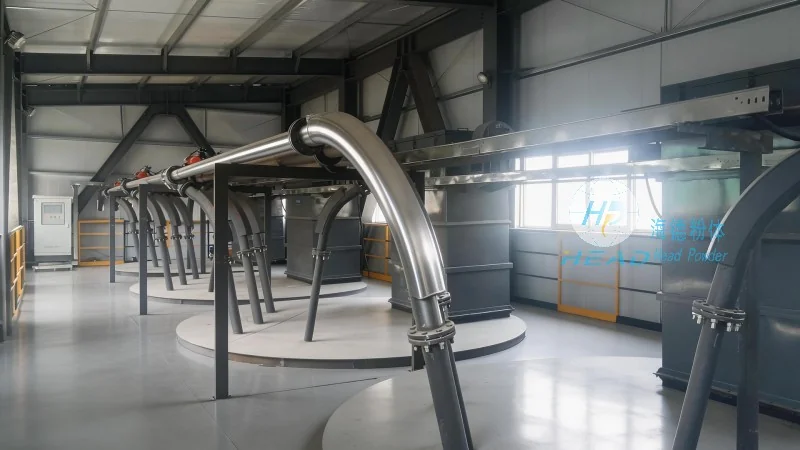
Working Principle of the Pneumatic Conveying Process
The operation of the sulfate potash pneumatic conveying system is based on the principle of pneumatic transport, where air is used to create a flow of material through the pipeline. The process begins with the material being fed from the hopper into the rotary feeder, which regulates the flow rate. The feeder then delivers the material into the conveying pipeline, where it is mixed with high-velocity air. The air, moving at a sufficient velocity, lifts and transports the material particles through the pipeline to the discharge point. The air and material mixture then passes through a filter system, where the air is cleaned and the material is separated from the air stream. The cleaned air is typically vented to the atmosphere, while the material is collected in the discharge unit and delivered to its final storage or processing location. The system operates under a pressure or vacuum condition, depending on the specific application and material characteristics. The pressure system uses compressed air to push the material through the pipeline, while the vacuum system uses a suction mechanism to draw the material from the source. The choice between pressure and vacuum depends on factors such as the distance to be covered, the material's density, and the system's overall efficiency. The system is equipped with control valves and sensors to monitor and adjust the air flow and material feed rate, ensuring optimal performance and preventing system overload or blockages.
Advantages and Applications of the System
The sulfate potash pneumatic conveying system offers several advantages that make it an ideal choice for industrial applications. One of the primary benefits is its ability to transport materials over long distances without the need for intermediate storage or transfer points, which reduces operational costs and improves overall efficiency. The system also minimizes material loss and contamination, as the material is contained within the pipeline and handled in a closed environment. This is particularly important for sensitive materials like sulfate potash, which can be affected by moisture or dust exposure. Additionally, the system provides enhanced safety features, as it eliminates the need for manual handling of bulk materials, reducing the risk of accidents and injuries. The system is also highly adaptable, with the ability to integrate with existing production lines and expand to meet increasing production demands. The applications of the sulfate potash pneumatic conveying system are widespread, including the transportation of raw materials in fertilizer plants, the delivery of finished products to storage facilities, and the transfer of materials between different processing stages. The system is also suitable for use in other industries, such as the chemical and food processing sectors, where bulk material handling is required.
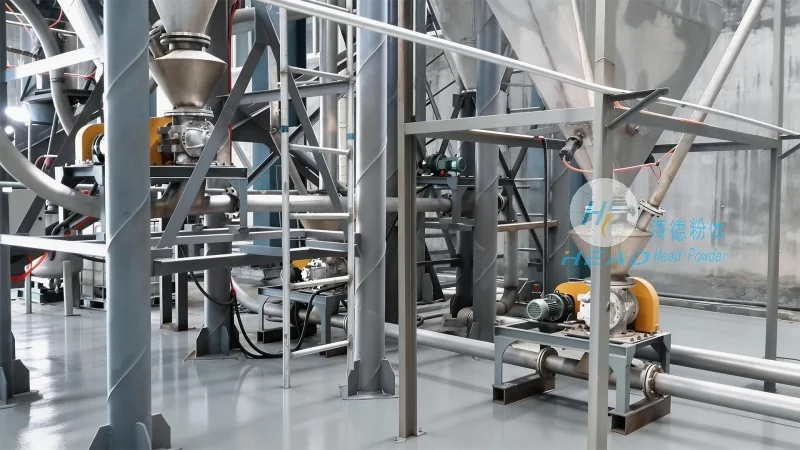
Company Information and Commitment
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of pneumatic conveying systems, with a strong commitment to quality, innovation, and customer satisfaction. The company is headquartered in Shandong, China, and has a team of experienced engineers and technicians dedicated to developing and producing high-performance conveying solutions. HeadPowder specializes in customizing systems to meet the specific requirements of clients, ensuring that each system is optimized for the material being transported and the operational conditions of the facility. The company adheres to strict quality control standards, using only the highest-quality materials and components in the manufacturing process. HeadPowder also provides comprehensive after-sales support, including installation, maintenance, and technical assistance, to ensure that clients receive the best possible service and support throughout the life of their system. With a focus on reliability, efficiency, and safety, HeadPowder is a trusted partner for businesses in the fertilizer and chemical industries, providing them with the tools they need to improve their operations and achieve their production goals.




