Automatic tonne bag feeding material pneumatic conveying equipment is a critical component in modern industrial material handling systems, designed to efficiently transfer bulk materials from storage containers to processing units. This equipment plays a vital role in enhancing production efficiency, reducing labor costs, and improving safety in various industries such as chemical, food, and pharmaceutical manufacturing. The seamless operation of this system relies on a combination of advanced mechanical and pneumatic technologies, ensuring reliable and consistent material flow.
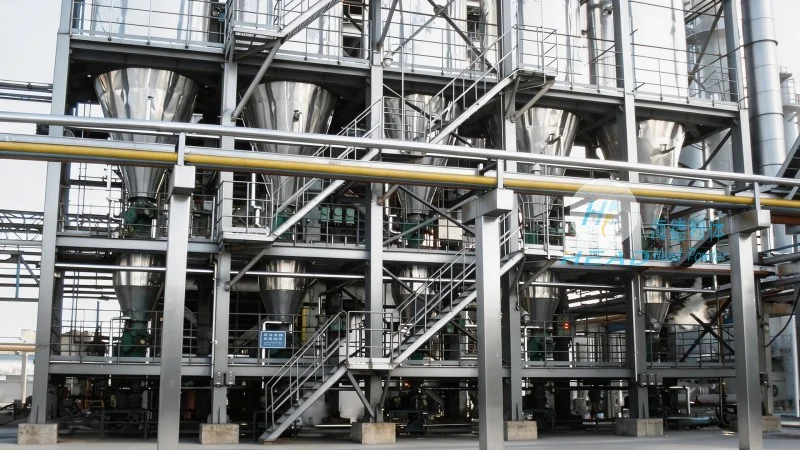
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the manufacturer of this advanced pneumatic conveying equipment, is a leading company in the field of material handling solutions. With a strong presence in China, specifically in Shandong province, HeadPowder specializes in designing, manufacturing, and supplying high-quality industrial equipment tailored to meet the diverse needs of global clients. The company's commitment to innovation and quality has established it as a trusted partner for businesses seeking efficient and reliable material handling solutions. HeadPowder's headquarters and operational base are located in Shandong, China, providing a robust foundation for delivering cutting-edge equipment and technical support.
Overview of the Automatic Tonne Bag Feeding System
The automatic tonne bag feeding material pneumatic conveying system is engineered to handle large volumes of bulk materials, typically stored in tonne bags or bulk containers. The system integrates several key components, including a hopper for material storage, a feeding mechanism to control the flow from the bag, a pneumatic conveying line to transport the material, and a receiving hopper or silo for final processing. Each component works in tandem to ensure a smooth and continuous material transfer process, minimizing downtime and maximizing productivity.
Step-by-Step Operation Process
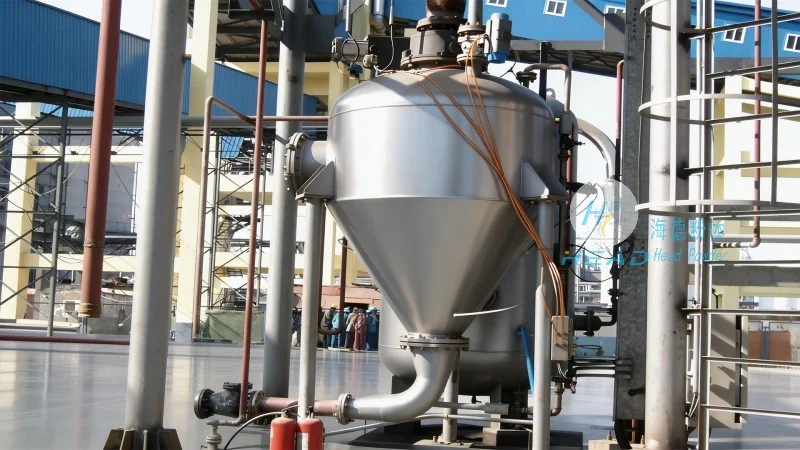
The operation of the automatic tonne bag feeding material pneumatic conveying equipment follows a systematic sequence of steps, each designed to optimize material handling efficiency. The process begins with the placement of a tonne bag into the feeding hopper, which is equipped with a discharge valve or a mechanical auger to control the material release. Once the bag is positioned correctly, the feeding mechanism activates, allowing the material to flow into the hopper at a controlled rate. Simultaneously, the pneumatic conveying system is activated, using compressed air to create a pressure differential that propels the material through the conveying line. The material travels through the pipeline, often passing through a filter or separator to remove any contaminants, before being discharged into the receiving hopper or processing unit. The entire process is automated, with sensors and control systems monitoring the flow rate, pressure, and material level to ensure consistent operation. This automation reduces the need for manual intervention, enhancing safety and reducing labor costs.
Working Principle of the Pneumatic Conveying System
The core of the automatic tonne bag feeding system is the pneumatic conveying mechanism, which operates on the principle of using compressed air to transport bulk materials. The system typically employs a positive displacement or pressure differential method to move the material. In the positive displacement method, a pump or blower creates a high-pressure air stream that forces the material through the pipeline. The material is suspended in the air stream, forming a dense phase or dilute phase flow, depending on the system design and material characteristics. The receiving hopper is positioned at a lower elevation than the feeding hopper, utilizing gravity to assist in the material discharge. The compressed air is then filtered and recycled back to the system, ensuring energy efficiency and minimal waste. The control system manages the air pressure, flow rate, and material feed rate, maintaining a stable and efficient conveying process. This principle allows for the safe and effective transport of various materials, including powders, granules, and fine particles, over long distances without the need for mechanical components like belts or buckets.
Key Features and Benefits
The automatic tonne bag feeding material pneumatic conveying equipment offers several advantages that make it an ideal choice for industrial applications. One of the primary benefits is its ability to handle large volumes of material with minimal labor, reducing operational costs and increasing productivity. The system is designed for high efficiency, with low maintenance requirements and long service life, thanks to the use of durable materials and advanced engineering. Additionally, the pneumatic conveying method eliminates the need for manual handling of bulk materials, enhancing workplace safety by reducing exposure to dust and potential hazards. The equipment is also highly flexible, capable of transporting various materials with different properties, and can be easily integrated into existing production lines. The automation features, including real-time monitoring and control, provide operators with precise control over the material flow, ensuring consistent quality and reducing the risk of material loss or contamination.
Applications and Industry Use Cases
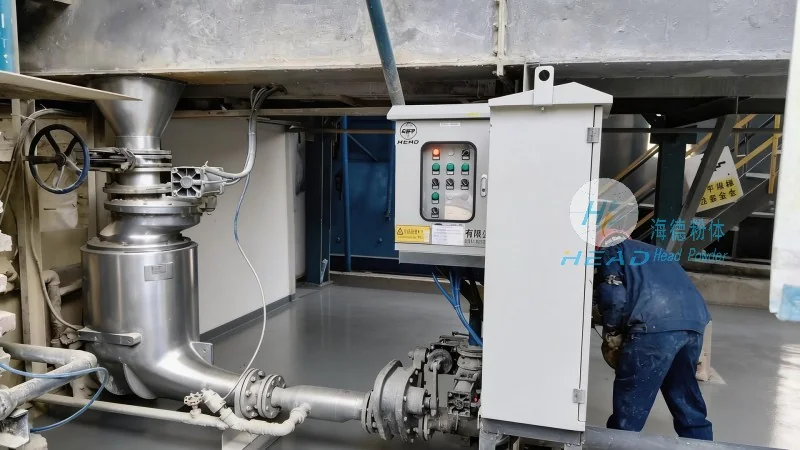
The automatic tonne bag feeding material pneumatic conveying equipment is widely used in various industries where bulk material handling is essential. In the chemical industry, it is used to transport raw materials such as powders and granules to reactors and processing units. In the food and pharmaceutical sectors, the system ensures hygienic and contamination-free material transfer, meeting stringent regulatory requirements. The equipment is also utilized in the mining and construction industries for handling raw materials like sand, gravel, and cement. Its ability to handle different material types and its flexibility make it suitable for a wide range of applications, from small-scale operations to large-scale industrial plants. The system's efficiency and reliability have made it a preferred choice for businesses seeking to optimize their material handling processes and improve overall operational performance.
Conclusion
Automatic tonne bag feeding material pneumatic conveying equipment, manufactured by Shandong HeadPowder Engineering Co., Ltd., represents a significant advancement in industrial material handling technology. By combining advanced automation, efficient pneumatic conveying, and robust engineering, this equipment offers a reliable and cost-effective solution for transferring bulk materials. The systematic operation process and clear working principles ensure consistent performance, while the key features and benefits enhance productivity, safety, and flexibility. As industries continue to seek more efficient and sustainable material handling solutions, this equipment remains a vital component in modern manufacturing processes, supporting the growth and success of businesses worldwide.




