HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced air-pneumatic conveying systems tailored for handling wheat bran and similar bulk materials. This article provides a detailed overview of the operational process and underlying principles of such equipment, emphasizing its efficiency and reliability in industrial applications.
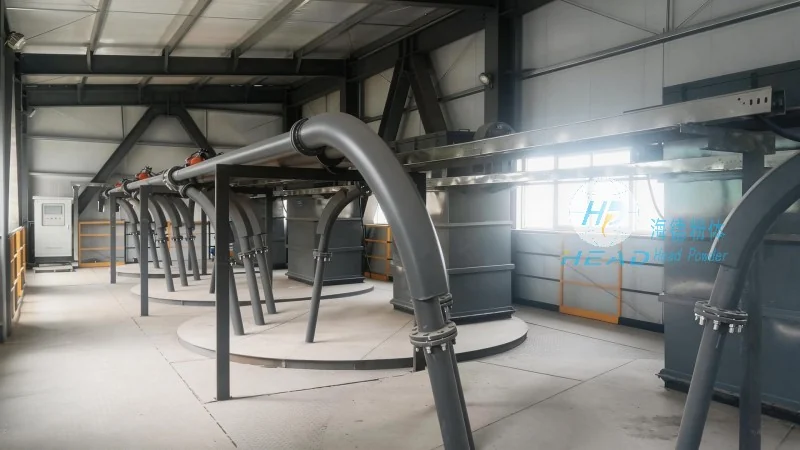
Introduction to Air-Pneumatic Conveying Systems for Wheat Bran
Wheat bran, a byproduct of the milling process, is often handled in large quantities and requires efficient transport solutions to maintain quality and minimize material loss. Air-pneumatic conveyors offer a versatile and effective method for moving these materials from one location to another within a processing facility. The system utilizes compressed air to create a flow of material through a pipeline, ensuring a clean and hygienic transfer process.
Key Components of the Air-Pneumatic Conveyor System
The air-pneumatic conveyor for wheat bran typically consists of several critical components that work in concert to achieve seamless material transport. These include a hopper for material storage, an air compressor to generate the necessary pressure, a pipeline network to guide the material flow, and a discharge unit at the receiving end. Each component plays a vital role in the overall operation, ensuring that the system operates smoothly and efficiently.
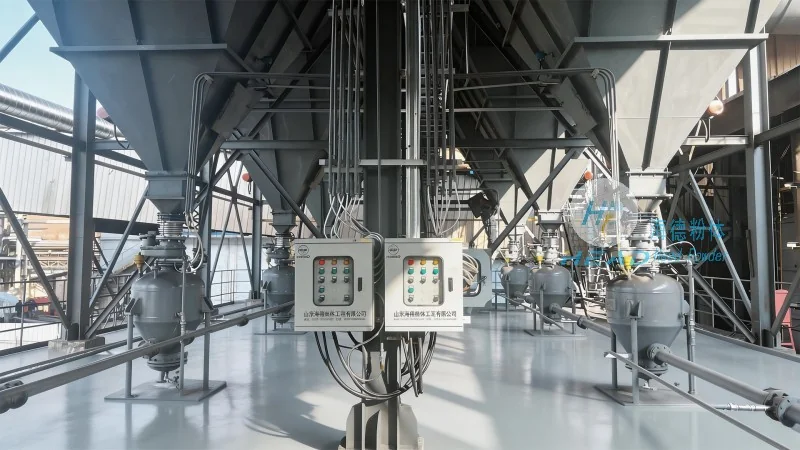
Operation Process of the Air-Pneumatic Conveyor
The operational process begins with the loading of wheat bran into the hopper. The material is then fed into the pipeline under the influence of compressed air, which propels the bran through the system. As the material travels through the pipeline, it is continuously mixed with air, maintaining a consistent flow rate. The system is designed to handle varying material loads and flow rates, adapting to the specific requirements of the processing line.
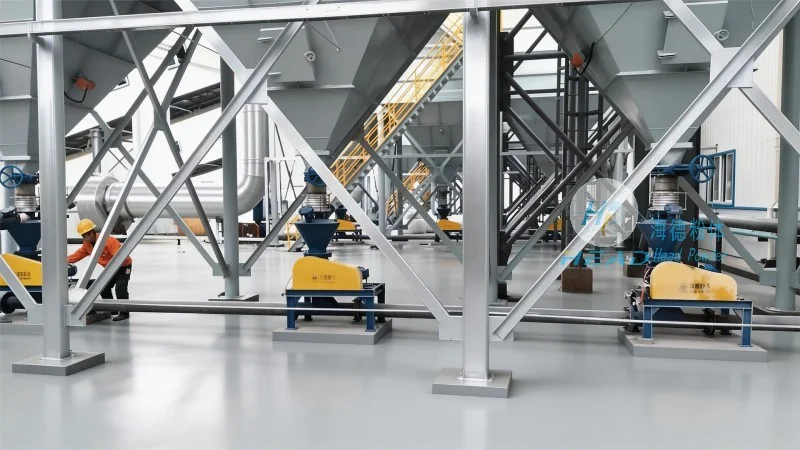
Working Principle of the Air-Pneumatic Conveyor
The core principle of the air-pneumatic conveyor is the use of differential pressure to move the material. Compressed air is introduced into the pipeline, creating a pressure difference between the inlet and outlet. This pressure difference generates a flow of air that entrains the wheat bran particles, carrying them along the pipeline. The system can operate in both positive and negative pressure modes, depending on the application and material characteristics. The design ensures that the material is transported without excessive pressure or velocity, minimizing wear and tear on the equipment and preserving the quality of the wheat bran.
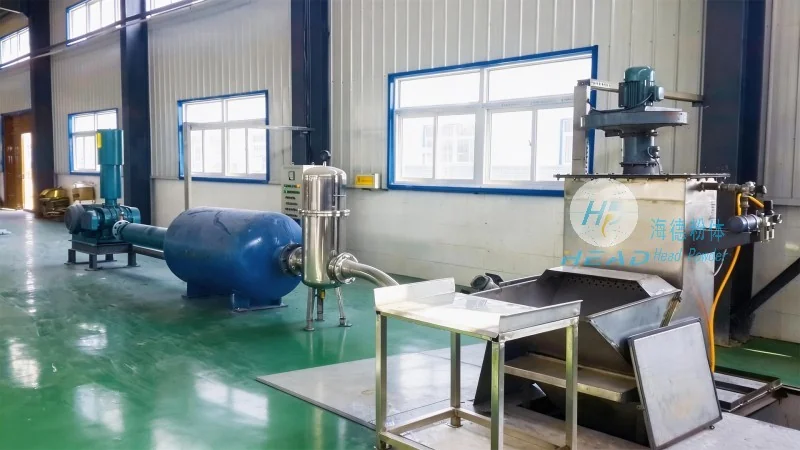
Advantages of Using Air-Pneumatic Conveyors for Wheat Bran
Implementing an air-pneumatic conveyor for wheat bran offers several advantages over traditional mechanical conveying methods. These include reduced material handling time, improved hygiene and cleanliness, and lower maintenance costs. The system is also highly flexible, allowing for easy integration into existing processing lines and the ability to transport materials over long distances without the need for intermediate storage or handling points.
Conclusion
HeadPowder's air-pneumatic conveying systems provide an efficient and reliable solution for the transport of wheat bran and similar bulk materials. By understanding the operational process and working principles, users can optimize their material handling processes, enhancing productivity and maintaining product quality. With a focus on innovation and quality, HeadPowder continues to deliver advanced solutions tailored to the needs of the food processing industry.




