Small bag quantitative weighing material conveying lines are advanced industrial equipment designed to handle the precise weighing and transportation of materials in bulk packaging. These systems are integral to modern manufacturing and processing industries, ensuring efficiency, accuracy, and reliability in material handling operations. The following sections will explore the fundamental principles behind these systems and highlight key working scene characteristics that make them indispensable in various industrial applications.
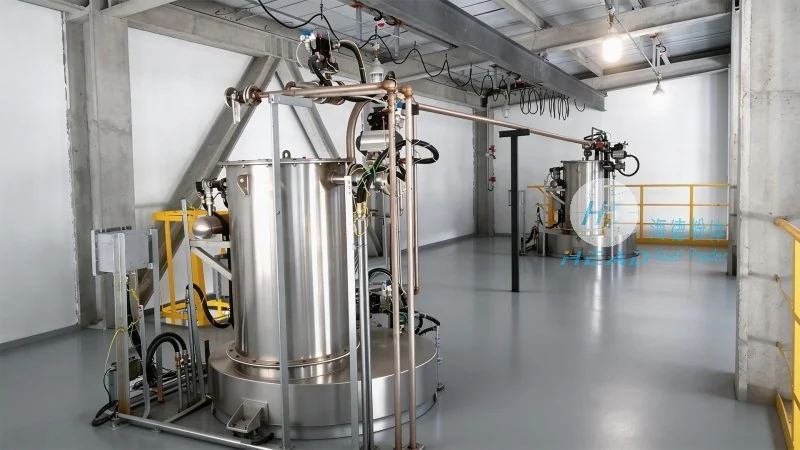
Company Introduction and Background
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of high-quality material handling solutions. With a strong commitment to innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for businesses seeking reliable and efficient conveying systems. The company’s headquarters is located in Shandong, China, where state-of-the-art facilities and a dedicated team of engineers work tirelessly to deliver cutting-edge solutions tailored to diverse industrial needs.
Principle of Small Bag Quantitative Weighing Material Conveying Lines
The core principle of small bag quantitative weighing material conveying lines revolves around the integration of weighing technology with automated material handling. These systems typically consist of several key components, including a conveyor belt, a weighing scale, a control system, and a packaging unit. The process begins with raw materials being loaded onto the conveyor belt, which transports the material to the weighing station. At the weighing station, the system uses precision load cells to measure the weight of the material in small bags, ensuring that each bag meets the specified weight criteria. The control system then processes the weight data and triggers the next steps in the packaging process, such as filling, sealing, and labeling. This integrated approach minimizes human intervention, reduces errors, and enhances overall operational efficiency.
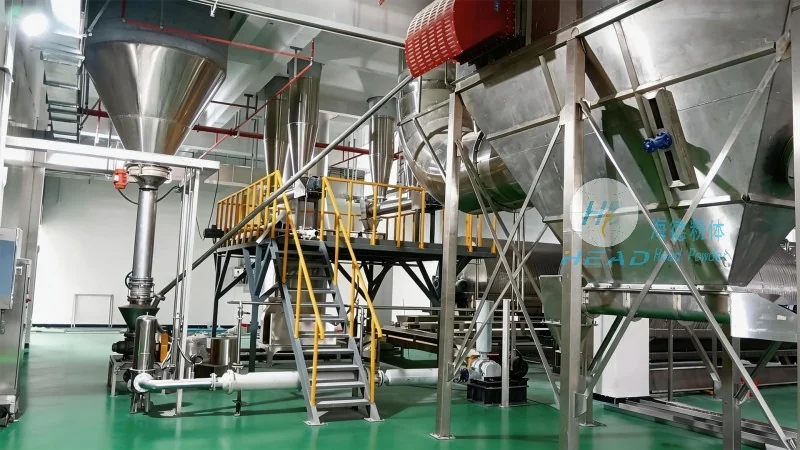
Working Scene Characteristics of Small Bag Quantitative Weighing Material Conveying Lines
The working scene characteristics of small bag quantitative weighing material conveying lines are tailored to meet the demands of various industrial environments. These systems are commonly used in sectors such as food processing, chemical manufacturing, pharmaceuticals, and agriculture, where consistent quality and precise dosing are critical. The flexibility of these lines allows them to handle a wide range of materials, from powders and granules to liquids and bulk solids. In food processing, for example, the systems ensure that each bag of ingredients is accurately weighed and packaged, maintaining compliance with food safety regulations and quality standards. In the chemical industry, the precision of the weighing process is essential to prevent over or under-dosing, which can impact product performance and safety. The pharmaceutical sector benefits from the ability to handle sensitive materials with minimal contamination, thanks to the sealed and controlled environment of the conveying line. Additionally, the systems are designed to operate in high-volume production environments, supporting continuous and uninterrupted operations, which is crucial for meeting market demands and optimizing production schedules.
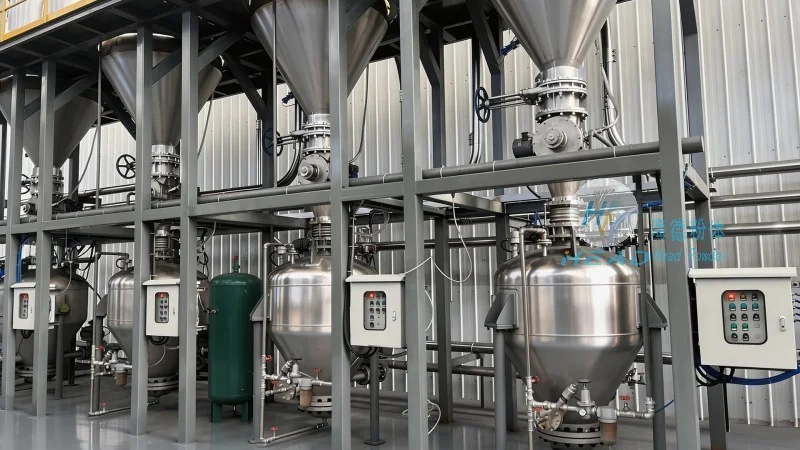
Key Advantages and Applications
Small bag quantitative weighing material conveying lines offer several advantages that make them a preferred choice for industrial applications. The primary advantage is the high level of accuracy and consistency in weighing, which reduces waste and improves product quality. The automated nature of these systems minimizes labor costs and eliminates human errors, leading to increased productivity and operational efficiency. Another key advantage is the flexibility to handle different bag sizes and material types, allowing for customization to meet specific customer requirements. These systems are also designed for easy integration with existing production lines, enabling seamless operation and minimal downtime during setup or maintenance. In terms of applications, the systems are widely used in the packaging of agricultural products, such as fertilizers and seeds, where precise dosing is essential for optimal plant growth. They are also employed in the pharmaceutical industry for the packaging of medications, ensuring that each dose is accurately measured and delivered to patients. Furthermore, the systems are suitable for the packaging of chemical products, where safety and compliance with regulatory standards are paramount.
Conclusion and Future Outlook
Small bag quantitative weighing material conveying lines represent a significant advancement in material handling technology, combining precision weighing with automated transportation to enhance operational efficiency and product quality. As industries continue to demand higher standards of accuracy and reliability, these systems will play an increasingly important role in meeting production requirements. HeadPowder, with its expertise and commitment to innovation, remains at the forefront of developing and supplying advanced material handling solutions that cater to the evolving needs of modern industries. By leveraging the principles and characteristics outlined above, businesses can benefit from improved productivity, reduced costs, and enhanced product quality, ultimately gaining a competitive edge in their respective markets.




