Gray warehouse material conveying lines are a critical component in modern industrial logistics, engineered to efficiently transport bulk materials within storage facilities. These systems are designed to handle diverse materials, including powders, granules, and bulk solids, ensuring smooth and reliable material flow. The design and functionality of these conveying lines are tailored to meet the specific requirements of various industrial applications, making them a key asset for optimizing warehouse operations and enhancing overall productivity.
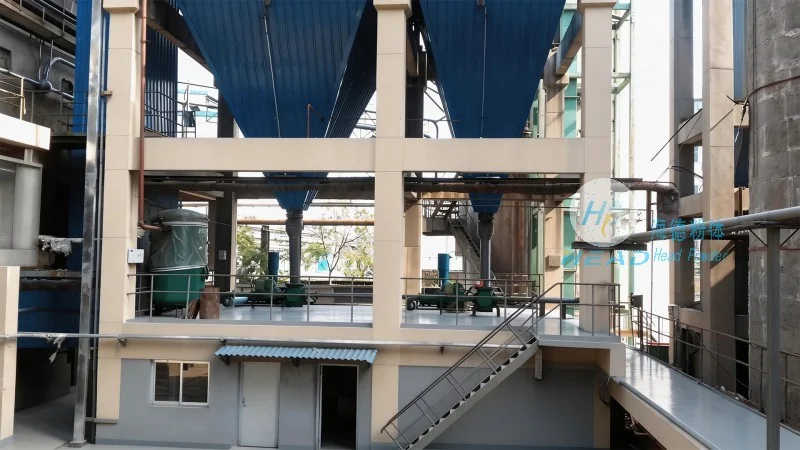
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, as the manufacturer, specializes in the design, development, and installation of advanced material handling solutions. With a strong operational base in Shandong, China, the company leverages its expertise to deliver high-quality conveying systems that enhance operational efficiency and safety. The company's commitment to innovation and customer-centric service has established it as a trusted partner in the material handling industry, providing tailored solutions for diverse industrial needs.
Principle of Material Conveying
The core principle of gray warehouse material conveying lines revolves around the efficient movement of materials from storage to processing or packaging areas. These systems typically utilize mechanical components such as conveyor belts, screw conveyors, or pneumatic transport to ensure consistent and controlled material flow. The gray color of the warehouse often indicates specialized storage for materials requiring controlled environmental conditions, such as moisture-sensitive or temperature-sensitive products. The conveying lines are integrated with the warehouse infrastructure to facilitate seamless material transfer, reducing manual handling and minimizing the risk of material loss or contamination.
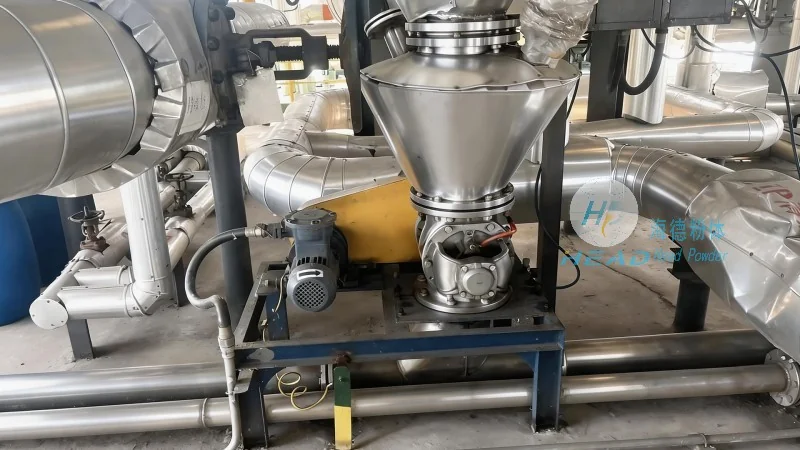
Working Scene Characteristics
The working scene characteristics of gray warehouse material conveying lines are tailored to the specific needs of industrial environments. These systems are commonly used in sectors like pharmaceuticals, food processing, chemical manufacturing, and bulk material storage. The design allows for flexibility in accommodating different material types and sizes, ensuring that the conveying process is optimized for each application. For example, in pharmaceutical facilities, the conveying lines are designed to maintain sterile conditions and prevent cross-contamination, while in food processing plants, they are constructed to meet sanitary standards and ensure product safety. The operational characteristics include high reliability, low maintenance requirements, and the ability to handle large volumes of material, making them suitable for continuous production lines.
Key Features and Advantages
Gray warehouse material conveying lines offer several key features that contribute to their effectiveness in industrial settings. These include adjustable speed control, enabling operators to manage the flow rate based on production demands. The systems are also equipped with safety features, such as emergency stop buttons and overload protection, to ensure operational safety. Additionally, the modular design allows for easy integration with existing warehouse infrastructure and supports future expansion as business needs evolve. The use of durable materials, such as stainless steel or corrosion-resistant components, ensures long-term performance and reduces the need for frequent replacements. Overall, these features make gray warehouse material conveying lines a cost-effective and reliable solution for material handling in various industrial applications.
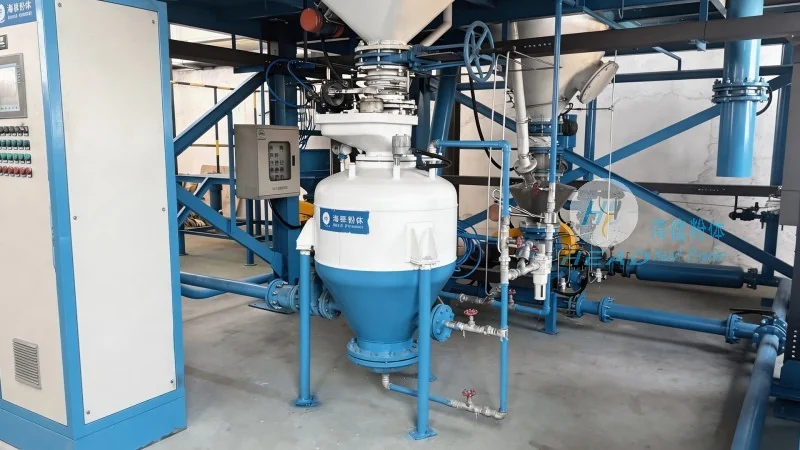
Application Examples
Real-world applications of gray warehouse material conveying lines demonstrate their versatility and effectiveness. In a pharmaceutical manufacturing plant, the conveying lines are used to transport raw materials from storage silos to production lines, ensuring a continuous supply of ingredients. In a food processing facility, the system efficiently moves bulk grains or powders from storage bins to packaging machines, maintaining product quality and reducing downtime. In chemical plants, the conveying lines handle hazardous materials, such as powders or granules, with safety measures in place to prevent accidents. These examples highlight how the systems adapt to different operational requirements while maintaining efficiency and safety standards.
Conclusion
Gray warehouse material conveying lines are a vital part of modern industrial logistics, providing efficient and reliable material handling solutions. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., these systems are designed to meet the specific needs of various industries, ensuring optimal performance and operational efficiency. The principles and characteristics of these conveying lines make them an essential asset for any facility that requires consistent and controlled material flow. As industrial demands continue to evolve, the development of advanced material handling systems will remain crucial in maintaining competitiveness and productivity.




