HeadPowder, a leading provider of industrial powder handling solutions, specializes in the design and manufacturing of advanced sintering dust ash powder conveying machines. These systems are engineered to efficiently transport fine powders generated during sintering processes, such as those found in steel and non-ferrous metal production facilities. The company, based in Shandong, China, leverages over a decade of experience in powder technology to deliver robust and reliable equipment tailored to the unique demands of modern industrial applications.
Principle of Sintering Dust Ash Powder Conveying Machines
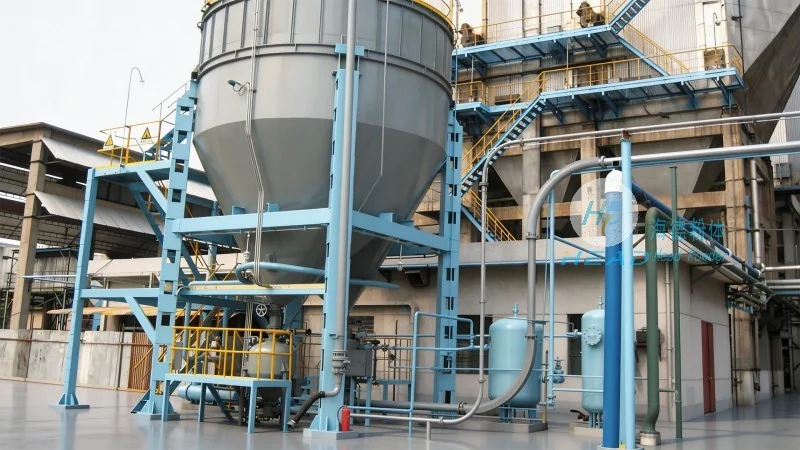
The core principle of sintering dust ash powder conveying machines revolves around the use of positive pressure or negative pressure systems to move fine particulate materials. Positive pressure systems, often utilizing air blowers or fans, create an airflow that propels the dust ash through a network of pipes and ducts. This method is particularly effective for conveying materials that are light in weight and have a high dust content. Negative pressure systems, on the other hand, operate by creating a vacuum that draws the dust ash into the conveying line, which is advantageous for applications requiring minimal air leakage and odor control. Both systems are designed to maintain consistent flow rates and particle size distribution, ensuring that the transported material remains intact and free from agglomeration.
Working Scene Characteristics
The working scene characteristics of sintering dust ash powder conveying machines are closely tied to the industrial environments in which they are deployed. These machines are typically found in large-scale sintering plants, where they play a critical role in managing the byproducts of the sintering process. The primary working scene includes the collection of dust ash from sintering furnaces, its transport to storage silos or treatment facilities, and the subsequent handling for recycling or disposal. The equipment must operate in harsh conditions, including high temperatures, abrasive particles, and varying humidity levels, which demands robust construction materials like stainless steel and high-grade alloys. Additionally, the systems are designed to integrate seamlessly with existing industrial infrastructure, minimizing downtime and maintenance requirements. The working scene also emphasizes safety and environmental compliance, as the dust ash often contains hazardous components that require careful handling to prevent pollution and ensure worker safety.
Key Features and Technical Advantages
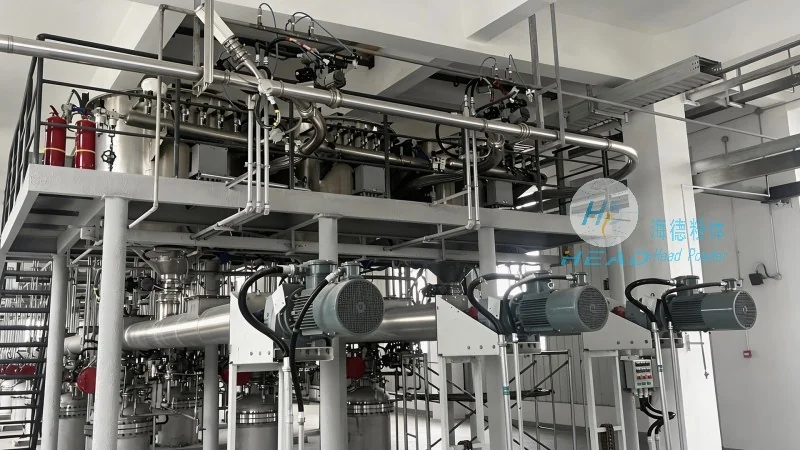
HeadPowder's sintering dust ash powder conveying machines are equipped with several key features that enhance their performance and reliability. These include adjustable airflow control systems that allow operators to fine-tune the conveying rate based on material properties and system requirements. The machines also feature advanced filtration and separation components, such as cyclone separators and bag filters, which help to maintain air quality and protect downstream equipment from particle buildup. Another critical feature is the integration of monitoring and control systems, which provide real-time data on flow rates, pressure differentials, and system performance. This enables proactive maintenance and reduces the risk of unexpected failures. The equipment is also designed for easy maintenance, with accessible components and modular designs that allow for quick replacement of worn parts. These technical advantages contribute to higher efficiency, lower operational costs, and extended equipment lifespan.
Application Scenarios and Industry Impact
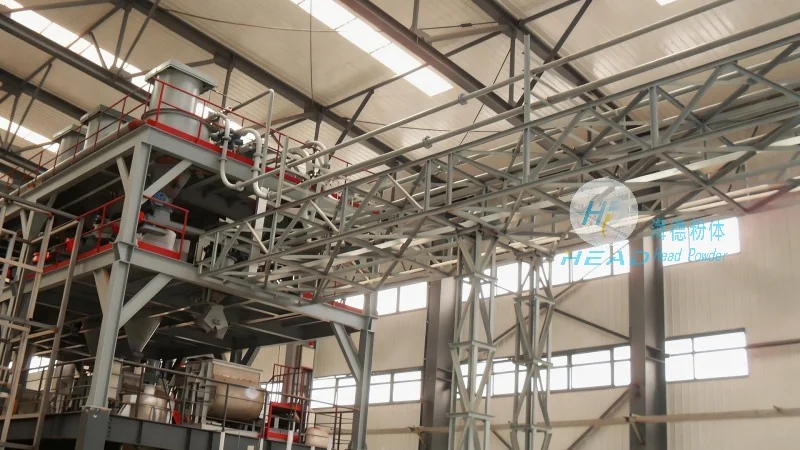
The application scenarios for sintering dust ash powder conveying machines span across multiple industries, with a strong focus on the metallurgical and cement sectors. In steel mills, these systems are essential for managing the large volumes of dust ash produced during the sintering of iron ore, which is a precursor to blast furnace operations. The efficient transport of this material reduces the need for manual handling, which improves safety and productivity. In cement plants, the machines help to handle the fine powders generated during the clinker production process, which are then used in the final cement mix. The consistent quality of the conveyed material ensures that the cement produced meets strict industry standards. Beyond these primary applications, the technology is also adapted for use in other industries that generate fine particulate waste, such as non-ferrous metal smelting and chemical processing. The impact of these machines extends beyond mere material transport; they contribute to overall process optimization by reducing waste, improving material recovery rates, and enhancing environmental sustainability. By efficiently handling sintering dust ash, these systems help industrial facilities achieve higher operational efficiency and comply with increasingly stringent environmental regulations.
Conclusion and Future Directions
HeadPowder's sintering dust ash powder conveying machines represent a significant advancement in industrial powder handling technology. By combining robust engineering with advanced control systems, these machines provide reliable and efficient solutions for the transportation of fine sintering dust ash. The working scene characteristics, which include harsh operating conditions and stringent safety requirements, are addressed through the use of high-quality materials and modular designs. The company's commitment to innovation and customer-centric solutions ensures that their equipment continues to meet the evolving needs of modern industrial applications. As industries strive for greater efficiency and sustainability, the role of advanced powder conveying systems like these will only become more critical. HeadPowder remains at the forefront of this technology, offering tailored solutions that enhance productivity, reduce costs, and promote environmental responsibility.




