Positive pressure blowing type powder conveying systems represent a critical technology in the field of material handling, particularly for the efficient and safe transportation of bulk powders. These systems utilize compressed air to create a positive pressure environment, ensuring that powders are conveyed from a source to a destination without exposure to external contaminants or atmospheric pressure fluctuations. The design and operation of such systems are tailored to meet the diverse demands of various industrial applications, making them indispensable in sectors ranging from chemical processing to food and pharmaceutical manufacturing.
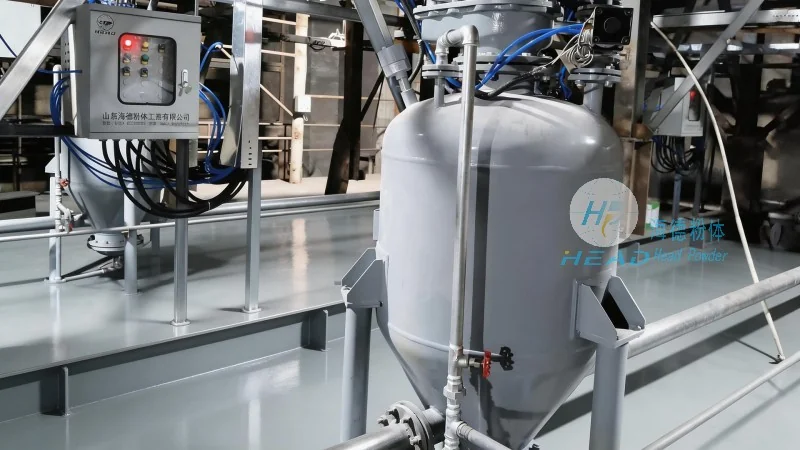
Introduction to Positive Pressure Blowing Type Powder Conveying Systems
At the core of positive pressure blowing type powder conveying systems is the principle of utilizing compressed air as the driving force to transport powders. Unlike negative pressure or vacuum systems, which rely on creating a vacuum to draw materials, positive pressure systems actively push powders through a sealed pipeline using high-pressure air. This approach offers several advantages, including enhanced material containment, reduced risk of dust emissions, and improved control over the conveying process. The system typically consists of a blower, a hopper or feeder to introduce the powder, a pipeline network, and a receiver or discharge point. The compressed air is introduced at the inlet of the pipeline, creating a pressure differential that propels the powder forward. The air and powder mixture is then separated at the discharge point, with the air typically being filtered and recycled or vented safely.
Working Scene Characteristics and Applications
The working scene characteristics of positive pressure blowing type powder conveying systems are highly adaptable to different industrial environments and material properties. For instance, in chemical plants, these systems are commonly used to transport reactive powders or those requiring strict contamination control, such as pharmaceutical intermediates or fine chemicals. The sealed pipeline design prevents cross-contamination and maintains the integrity of the material, which is crucial for compliance with regulatory standards. In the food industry, positive pressure systems are employed to convey ingredients like flour, sugar, or spices, ensuring that the product remains free from external contaminants and maintains its quality throughout the conveying process. The gentle handling of the powder by the air flow minimizes particle degradation, preserving the texture and flavor of the food products.
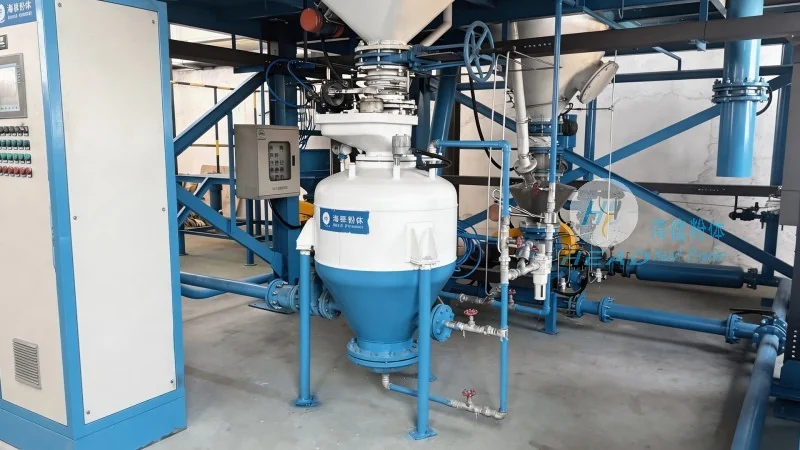
Advantages in Pharmaceutical and Food Processing
In the pharmaceutical sector, the use of positive pressure blowing type powder conveying systems is governed by stringent hygiene and safety regulations. The systems are designed with materials that are easy to clean and sanitize, such as stainless steel, and feature sealed connections to prevent microbial contamination. The positive pressure environment also helps maintain a controlled atmosphere, reducing the risk of microbial growth on the conveyed powders. This is particularly important for active pharmaceutical ingredients (APIs) and finished dosage forms. The efficiency of these systems in pharmaceutical manufacturing is evident in their ability to handle small batches of high-value powders with minimal loss and maximum precision. The ability to control the flow rate and pressure allows for precise dosing, which is critical in drug formulation processes.
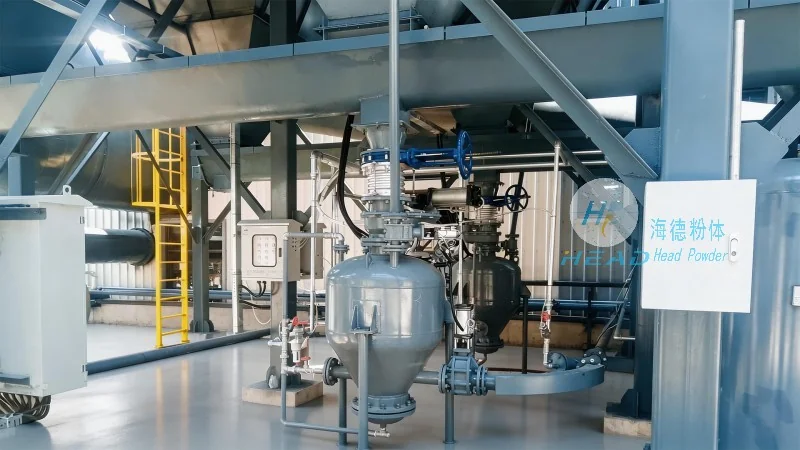
Industrial Applications and Performance Metrics
Beyond pharmaceuticals and food processing, positive pressure blowing type powder conveying systems find applications in a wide range of industries, including mining, cement production, and agricultural processing. In mining operations, these systems are used to transport ore or tailings over long distances, leveraging the high-pressure air to overcome resistance and maintain a consistent flow rate. The robust design of the equipment, including durable pipelines and high-capacity blowers, ensures reliable operation even in harsh environmental conditions. Performance metrics such as conveying capacity, pressure drop, and energy efficiency are key considerations when selecting a positive pressure system for industrial use. The capacity of these systems can range from a few kilograms per hour to several tons per hour, depending on the specific requirements of the application. The pressure drop across the pipeline is a critical factor, as it indicates the energy required to move the powder and can affect the overall efficiency of the system.
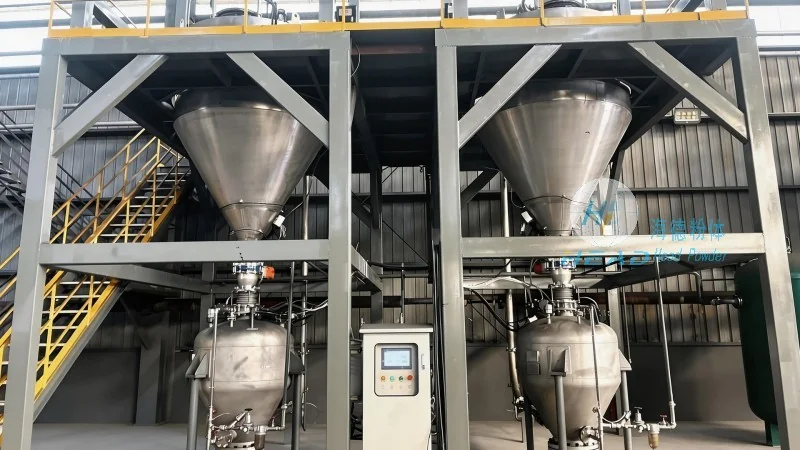
HeadPowder: A Leading Provider of Powder Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent manufacturer and supplier of positive pressure blowing type powder conveying systems. With its headquarters located in Shandong, China, HeadPowder has established itself as a trusted partner for industries seeking reliable and efficient material handling solutions. The company specializes in designing and manufacturing customized powder conveying systems that meet the unique needs of its clients. HeadPowder's products are engineered with precision, incorporating advanced technology to ensure optimal performance and durability. The company's commitment to quality is reflected in its adherence to international standards and rigorous testing protocols. HeadPowder's team of engineers and technicians work closely with clients to understand their specific requirements, from material properties to operational constraints, and develop tailored solutions that enhance productivity and safety. The company's extensive experience in the field allows it to address a wide range of challenges, from handling abrasive powders to managing high-volume conveying tasks.
Customization and Adaptability of Positive Pressure Systems
One of the key advantages of positive pressure blowing type powder conveying systems is their adaptability to various material types and operational conditions. HeadPowder offers a range of customization options to suit different applications. For example, the system can be configured with different types of hoppers and feeders to handle powders with varying flow characteristics, such as cohesive or free-flowing materials. The pipeline design can be adjusted to accommodate different diameters and lengths, ensuring that the system can be integrated into existing facilities or new installations. The blower selection is also customizable, with options for different pressure ratings and air volumes to match the conveying requirements. This flexibility allows HeadPowder to provide solutions that are tailored to the specific needs of each client, whether it's a small-scale operation or a large industrial plant. The adaptability of the systems also extends to the control systems, which can be integrated with existing automation platforms to provide real-time monitoring and control of the conveying process.




