Calcined ash, a byproduct from industrial processes such as coal combustion, requires efficient and reliable handling systems to ensure safe and effective transport. The calcined ash powder conveying equipment developed by Shandong HeadPowder Engineering Co., Ltd. addresses these needs through advanced engineering solutions tailored for high-performance material transport. This equipment is designed to handle the unique challenges posed by calcined ash, including its fine particle size, potential moisture content, and abrasive nature, ensuring optimal performance in various industrial applications.
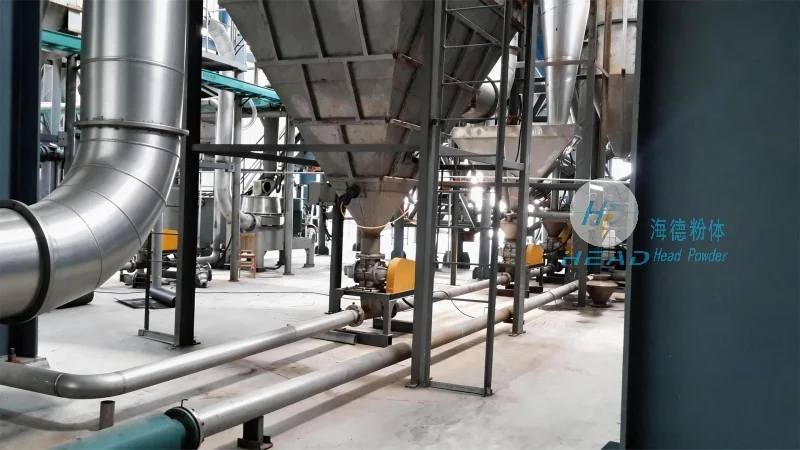
Working Principle of the Powder Conveying System
The core of the calcined ash powder conveying equipment is a sophisticated system that typically combines pneumatic and mechanical conveying technologies to achieve efficient material transport. The system operates by drawing the calcined ash powder into a conveying line using air pressure or mechanical means. The primary components include a hopper for material storage, a feeder to control the flow rate, a conveying line with appropriate ductwork, and a receiver for the discharged material. The air flow is managed by a blower or fan, which creates the necessary pressure differential to move the powder through the system. The design ensures that the powder is transported without clogging or degradation, maintaining the integrity of the material throughout the process.
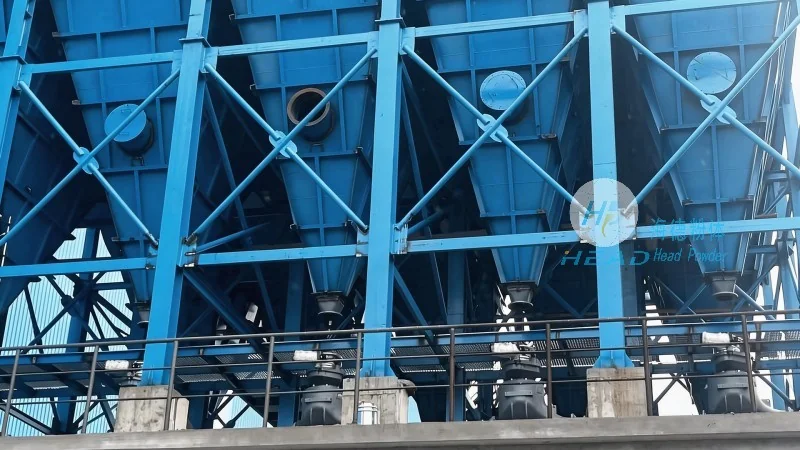
Key Features and Technical Specifications
Shandong HeadPowder Engineering Co., Ltd. has integrated several key features into the calcined ash powder conveying equipment to enhance its performance and reliability. These features include a robust construction using corrosion-resistant materials to withstand the abrasive nature of calcined ash, adjustable flow control mechanisms to match varying production demands, and advanced filtration systems to minimize dust emissions. The equipment is also equipped with safety sensors and alarms to prevent over-pressurization or blockages, ensuring operational safety. Technical specifications typically include a conveying capacity ranging from 5 to 50 tons per hour, depending on the system configuration, and a maximum conveying distance of up to 200 meters. The system operates at low noise levels and with minimal maintenance requirements, making it suitable for continuous industrial use.
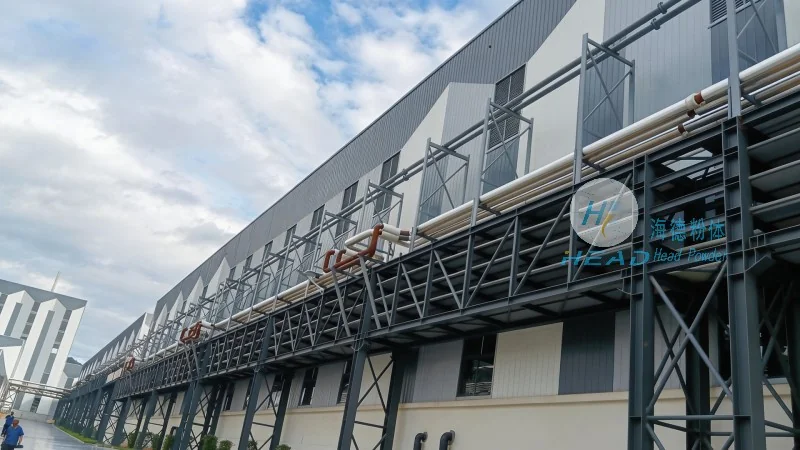
Typical Working Scenarios and Applications
The calcined ash powder conveying equipment is widely used in various industrial settings where calcined ash needs to be transported from one location to another. Common applications include power plants, where the equipment is used to transfer calcined ash from the bottom ash handling system to storage silos or disposal sites. It is also utilized in waste treatment facilities for the transport of calcined ash from incineration processes to landfills or recycling facilities. Additionally, the equipment is employed in cement and concrete production plants, where calcined ash is used as a supplementary cementitious material. In these scenarios, the equipment ensures that the calcined ash is handled efficiently, reducing labor costs and improving overall operational efficiency.
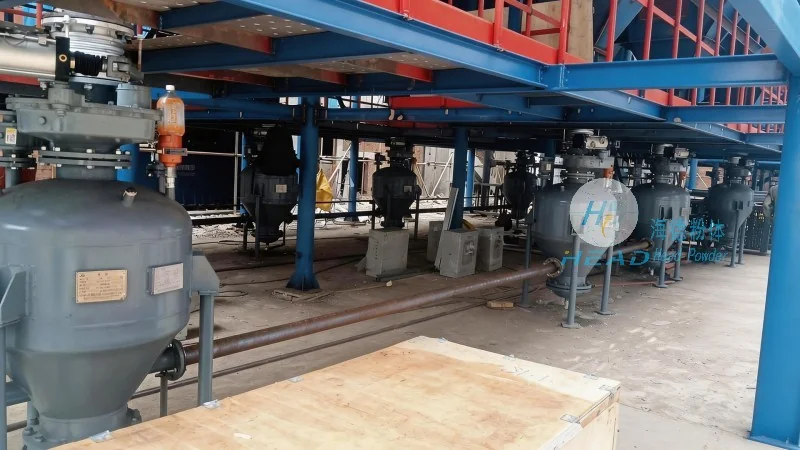
Company Information and Contact
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of industrial conveying equipment, is based in Shandong, China. The company specializes in designing and manufacturing high-quality powder handling systems tailored to the specific needs of various industries. With a focus on innovation and customer satisfaction, HeadPowder provides comprehensive solutions for material transport, including calcined ash powder conveying equipment. The company's products are known for their durability, efficiency, and compliance with international safety and environmental standards. For more information about the calcined ash powder conveying equipment or other industrial conveying solutions, please contact Shandong HeadPowder Engineering Co., Ltd.




