When it comes to handling purified ash in industrial processes, selecting the right conveying method is crucial for efficiency, safety, and cost-effectiveness. The choice of ash conveying system directly impacts the overall performance of waste management and material transport operations. In this article, we explore common purification ash conveying methods and highlight the advantages and features of HeadPowder's ash pneumatic conveying system, a leading solution from Shandong HeadPowder Engineering Co., Ltd., based in China.
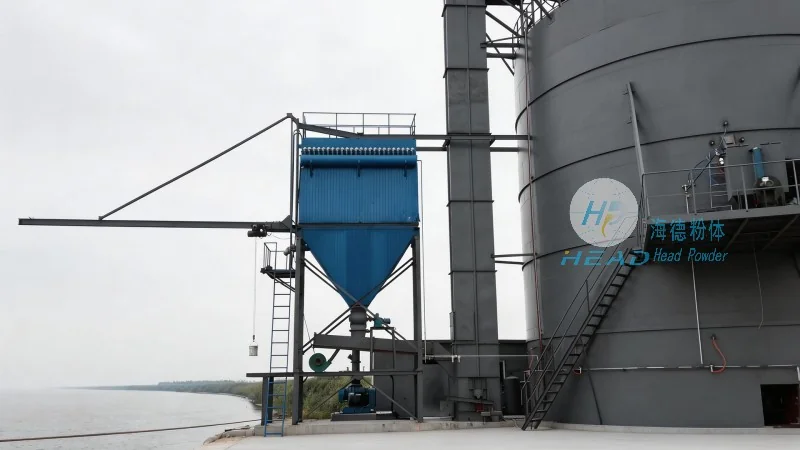
Understanding Common Purification Ash Conveying Methods
Industrial facilities dealing with ash from purification processes have several options for transporting this material. Traditional methods include mechanical conveyors like belt conveyors, screw conveyors, and bucket elevators. These systems rely on mechanical components to move ash from one location to another. While effective for certain applications, they often face challenges such as material buildup, wear and tear, and the need for regular maintenance. Additionally, mechanical conveyors may not be suitable for handling fine or dusty ash particles, which can lead to clogging and reduced efficiency.
Another common method is hydraulic conveying, which uses water to transport ash through pipelines. This approach is particularly useful for wet ash or slurry applications. However, hydraulic systems require significant water management and can be less efficient for dry ash, as water may need to be separated and reclaimed, adding complexity to the process. Furthermore, hydraulic conveying may not be ideal for environments where water usage is restricted or where the ash needs to be kept dry for downstream processing.
Introducing HeadPowder's Ash Pneumatic Conveying System
HeadPowder, a renowned name in the field of industrial material handling, offers a superior solution with its ash pneumatic conveying system. This system utilizes compressed air or other gases to transport purified ash through a network of pipes. The technology is designed to handle a wide range of ash characteristics, including fine powders, granules, and even sticky or abrasive materials, making it versatile for various industrial applications.
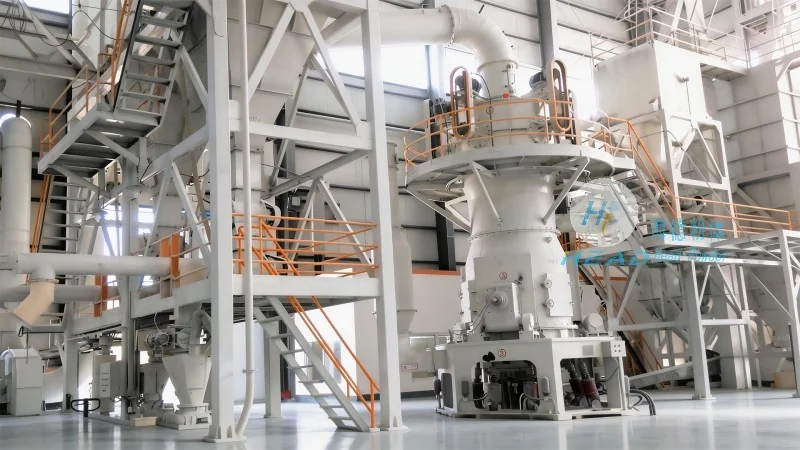
The core advantage of HeadPowder's pneumatic conveying system lies in its ability to provide a clean, dust-free, and efficient transport solution. Unlike mechanical or hydraulic methods, pneumatic systems eliminate the need for moving parts in contact with the ash, reducing wear and maintenance costs. This results in lower operational expenses and extended equipment lifespan. Moreover, the system ensures minimal environmental impact by containing dust and preventing emissions, aligning with modern industrial standards for sustainability.
Key Features and Advantages of HeadPowder's Ash Pneumatic Conveying
HeadPowder's ash pneumatic conveying system is equipped with several key features that set it apart from conventional methods. One of the primary benefits is its flexibility in system design. The system can be customized to fit the specific layout and requirements of a facility, whether it involves short or long-distance transport, vertical or horizontal movement, or integration with existing infrastructure. This adaptability makes it suitable for a wide range of industrial settings, from power plants and waste treatment facilities to manufacturing plants dealing with ash byproducts.
Another significant advantage is the system's high efficiency and reliability. By using compressed air, the conveying process is rapid and consistent, ensuring that ash is transported in a timely manner without delays. The system also offers excellent control over the flow rate and pressure, allowing operators to adjust the conveying parameters as needed to optimize performance. This level of control helps in maintaining the quality of the ash and preventing issues such as clogging or material degradation during transport.
Furthermore, HeadPowder's pneumatic conveying system is designed with safety and user-friendliness in mind. The system operates with minimal noise and vibration, creating a more comfortable working environment for personnel. It also includes advanced monitoring and control features, such as pressure sensors and flow meters, which provide real-time data on the system's performance. This allows for proactive maintenance and quick troubleshooting, reducing downtime and enhancing overall operational efficiency.
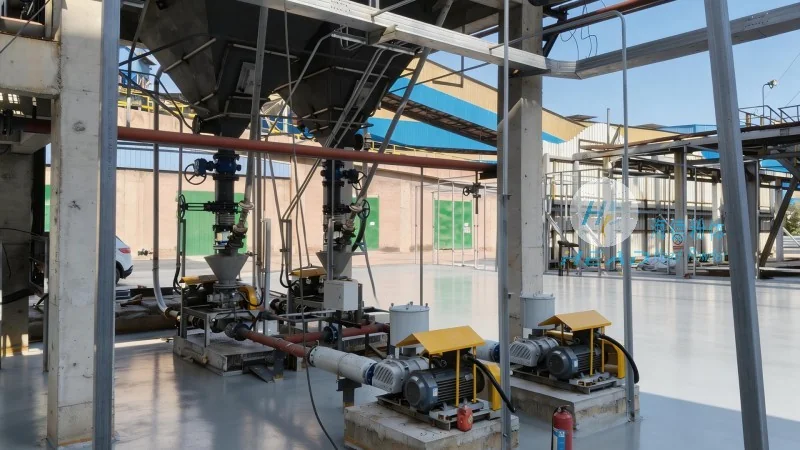
Applications and Benefits in Real-World Scenarios
The effectiveness of HeadPowder's ash pneumatic conveying system is evident in various real-world applications. For instance, in power plants, the system efficiently transports fly ash from the boiler to storage silos or for reuse in cement production. The clean and dust-free operation ensures that the ash is handled without contamination, meeting stringent environmental regulations. In waste treatment facilities, the system aids in the transport of ash from incineration processes, contributing to the overall waste management efficiency.
In manufacturing industries, where ash is a byproduct of certain processes, the system provides a reliable method for transporting the material to disposal or recycling facilities. The ability to handle fine particles without clogging makes it ideal for applications where the ash has a high moisture content or is prone to agglomeration. This ensures that the material is moved smoothly and consistently, preventing bottlenecks in the production line.
Conclusion and Contact Information
When considering purification ash conveying methods, it is clear that traditional mechanical or hydraulic systems may not always offer the best solution for modern industrial needs. HeadPowder's ash pneumatic conveying system, with its advanced features, efficiency, and reliability, stands out as a superior choice. By leveraging compressed air technology, this system provides a clean, low-maintenance, and cost-effective method for transporting purified ash. For businesses seeking to enhance their material handling capabilities and comply with environmental standards, HeadPowder's solutions from Shandong HeadPowder Engineering Co., Ltd., based in China, offer a robust and reliable option.




