Grain pneumatic conveying systems are essential equipment in modern grain handling and processing industries. These systems utilize air to transport bulk materials like grains, seeds, and powders over long distances with high efficiency and minimal product damage. The operation process and working principle of such systems are crucial for understanding their effectiveness and proper maintenance.
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, as a professional manufacturer based in Shandong, China, specializes in the design, production, and installation of advanced grain pneumatic conveying systems. With years of experience in the industry, the company has developed a range of solutions tailored to meet the diverse needs of agricultural and food processing sectors. The company’s commitment to quality and innovation ensures that its products deliver reliable performance and long-term durability.
Operation Process of Grain Pneumatic Conveying Systems
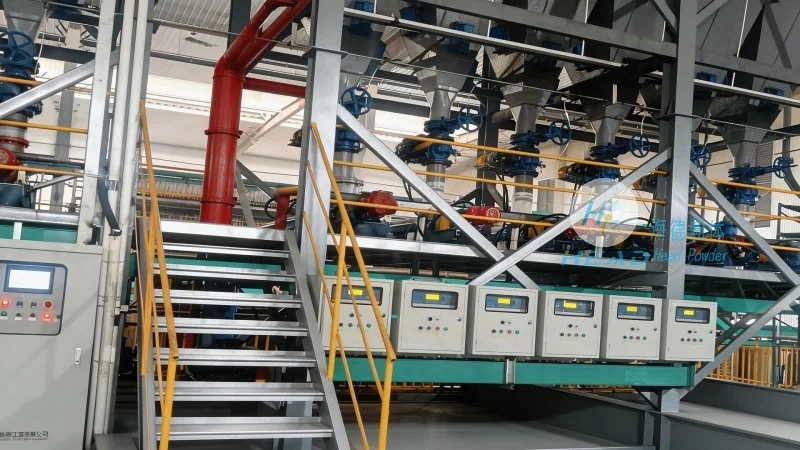
The operation process of a grain pneumatic conveying system typically involves several key steps. First, the grain is loaded into the hopper or storage silo. Then, an air compressor or blower generates high-pressure air, which is introduced into the conveying line. The air, along with the grain particles, is then propelled through the pipeline to the destination point, such as a processing plant or storage facility. The system may include components like cyclones, filters, and dust collectors to separate the air from the grain and ensure clean operation. The entire process is controlled by a system of valves, sensors, and a control panel, allowing for precise regulation of the conveying rate and air pressure.
Working Principle of Pneumatic Conveying Systems
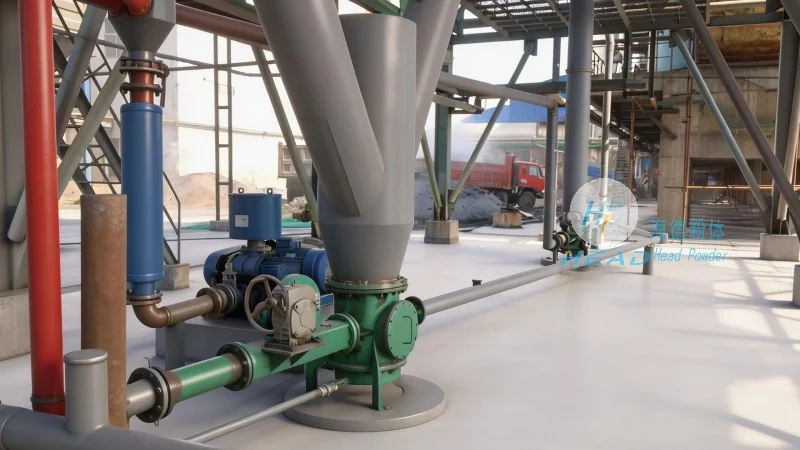
The working principle of grain pneumatic conveying systems is based on the principle of fluidization and pneumatic transport. When air is introduced into the conveying line at a sufficient velocity, it creates a fluidized state where the grain particles are suspended and carried along by the air stream. This method allows for continuous, non-stop material transport without the need for mechanical components like belts or buckets, which can cause wear and tear and product contamination. The system’s design, including the type of air flow (positive or negative pressure), the pipeline layout, and the size of the components, is critical to achieving optimal performance and minimizing energy consumption.
Key Features and Benefits
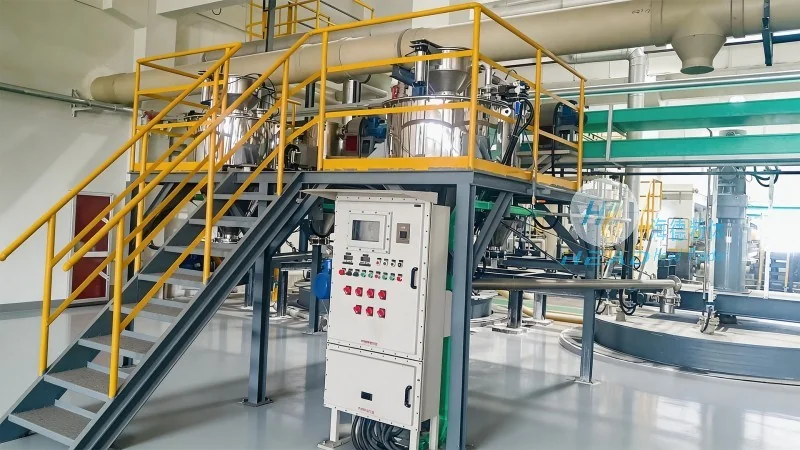
Grain pneumatic conveying systems offered by HeadPowder are designed with several key features that enhance their performance and reliability. These include high conveying capacities, low maintenance requirements, and the ability to handle a wide range of grain types and sizes. The systems are also equipped with advanced control systems that allow for real-time monitoring and adjustment of the conveying process. Additionally, the use of air as the conveying medium reduces the risk of product contamination and damage, making it ideal for food-grade applications. The company’s expertise in system design ensures that each installation is tailored to the specific requirements of the client, ensuring efficient and cost-effective operation.
Conclusion
Grain pneumatic conveying systems are a vital component of modern grain handling operations, offering efficient, reliable, and hygienic transport solutions. HeadPowder, with its professional team and advanced technology, provides high-quality systems that meet the needs of various industries. By understanding the operation process and working principle of these systems, users can ensure optimal performance and longevity of their equipment, contributing to increased productivity and reduced operational costs.




