HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for efficient tonne bag unloading operations. This article delves into the fundamental principles of such equipment and highlights key working scene characteristics that make it indispensable in various industrial applications.
Understanding the Core Principle of Tonne Bag Unloading Pneumatic Conveying Equipment
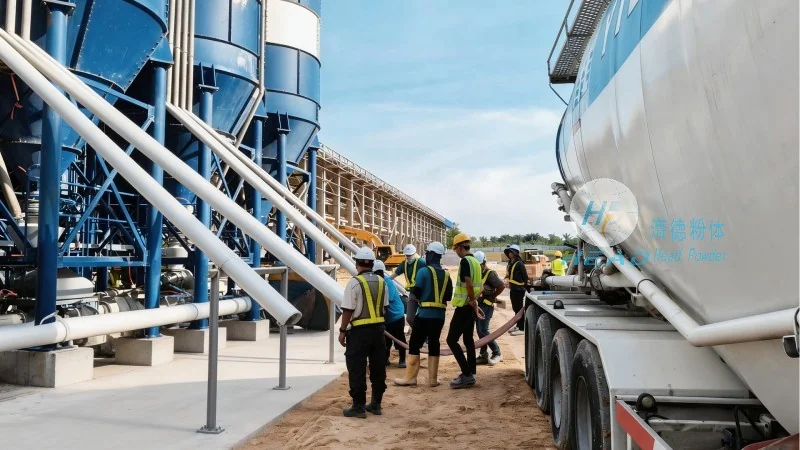
The primary function of tonne bag unloading pneumatic conveying equipment is to automate the process of transferring bulk materials from large bags (typically 1 tonne capacity) into processing or storage systems. The system operates on the principle of air flow, where compressed air or a combination of air and vacuum is used to create a pressure differential that moves the material through a pipeline. This method eliminates the need for manual handling, reducing labor costs and enhancing workplace safety. The equipment typically consists of several key components, including a bag opening mechanism, a hopper for collecting the material, a rotary valve or feeder to control the flow, and a conveying line that transports the material to the destination. The bag opening mechanism, often a pneumatic or mechanical device, safely opens the top of the bag, allowing the material to fall into the hopper. From there, the feeder regulates the discharge rate, ensuring a consistent flow into the conveying line. The conveying line, usually made of stainless steel or other corrosion-resistant materials, is designed to handle the specific characteristics of the material, such as particle size, moisture content, and abrasiveness. The air flow, generated by a blower or fan, creates a negative pressure in the line, drawing the material along with it. This process is known as suction conveying, which is particularly effective for materials that are dusty or have a tendency to create dust during handling.
Key Working Scene Characteristics and Applications
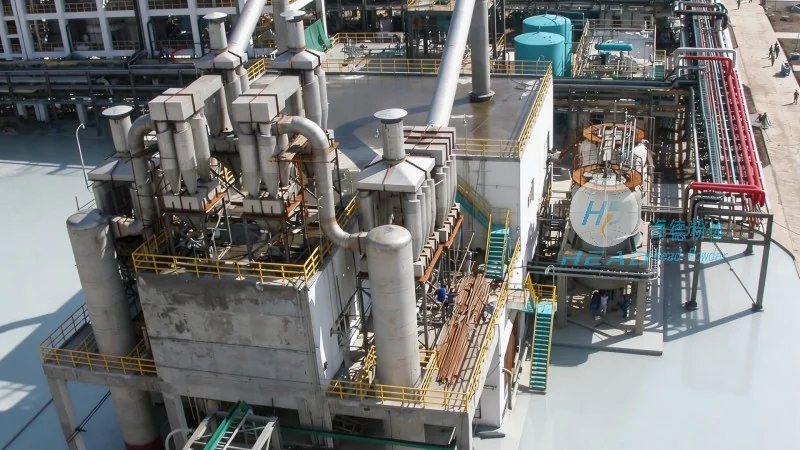
The working scene characteristics of tonne bag unloading pneumatic conveying equipment are tailored to meet the demands of diverse industrial environments. One of the most significant advantages is its ability to handle large volumes of material efficiently, making it ideal for applications in chemical, food, pharmaceutical, and mining industries. In chemical plants, for instance, the equipment is used to transfer raw materials like powders and granules into reactors or storage tanks, ensuring a continuous and controlled supply. The food industry benefits from the hygienic design of the equipment, which minimizes contamination risks and complies with strict regulatory standards. The pharmaceutical sector relies on the precision and cleanliness of the system to maintain product integrity and safety. In mining operations, the equipment is used to transport ore or other minerals from storage bags to processing machinery, improving operational efficiency and reducing downtime. Another key characteristic is the flexibility of the system, which can be adapted to different bag sizes and material types. This adaptability allows users to integrate the equipment into existing workflows without major modifications. The equipment also offers high reliability and low maintenance requirements, as the components are designed to withstand the rigors of continuous operation. This makes it a cost-effective solution for long-term material handling needs. Additionally, the system's ability to handle abrasive materials without significant wear and tear on the components is a crucial factor in its widespread adoption. The working scenes often involve integration with other processing equipment, such as mixers, crushers, or storage silos, creating a seamless material flow from unloading to processing. The equipment's ability to maintain a consistent flow rate is essential for maintaining the efficiency of downstream processes, preventing bottlenecks and ensuring optimal performance.
Technical Advantages and Performance Metrics
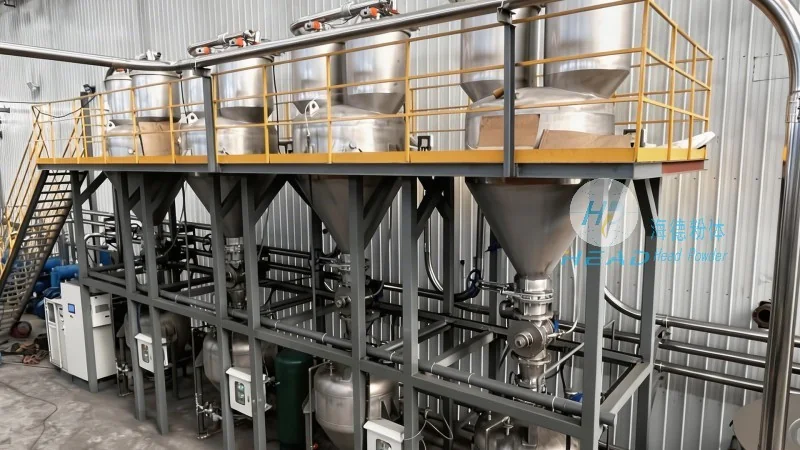
HeadPowder's tonne bag unloading pneumatic conveying equipment is engineered with several technical advantages that enhance its performance and reliability. The system is designed to handle a wide range of material properties, including varying particle sizes, moisture content, and bulk density. This versatility is achieved through adjustable parameters such as air pressure, flow rate, and hopper design, which can be customized to suit specific material characteristics. The equipment also features advanced control systems that allow for real-time monitoring and adjustment of the conveying process. This includes sensors to detect material levels, air pressure, and flow rates, providing operators with immediate feedback and enabling proactive maintenance. The control systems can be integrated with other plant systems, such as inventory management or process control, enhancing overall operational efficiency. The equipment's energy efficiency is another notable advantage, as it minimizes energy consumption compared to traditional mechanical conveying methods. This is achieved through optimized air flow design and efficient blower systems that operate at lower speeds and pressures when necessary. The system's durability is ensured by using high-quality materials and robust construction, which reduces the need for frequent repairs and replacements. The equipment is also designed for easy maintenance, with accessible components that can be serviced quickly, minimizing downtime. Performance metrics such as conveying capacity, which can range from several tons per hour to over 100 tons per hour depending on the system configuration, and the distance the material can be conveyed, which can be several hundred meters, are key indicators of the system's effectiveness. The system's ability to maintain a consistent flow rate and minimize material degradation is critical for maintaining product quality and reducing waste. Additionally, the equipment's compliance with international safety and environmental standards ensures that it meets the regulatory requirements of various industries, providing users with peace of mind.
Conclusion and Industry Impact
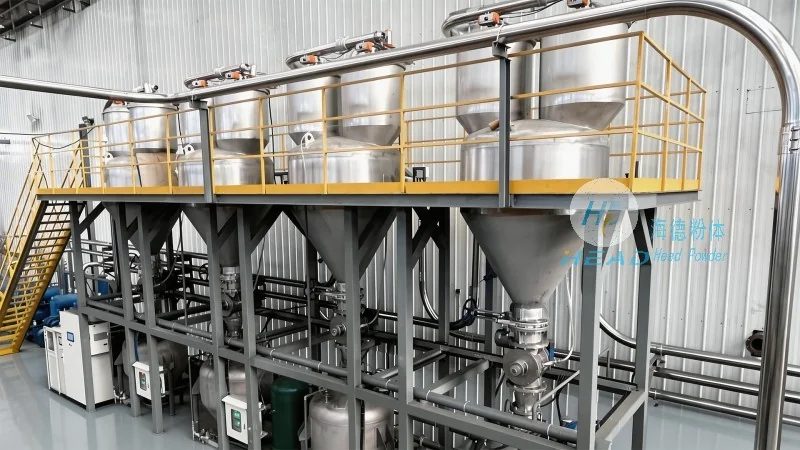
HeadPowder's tonne bag unloading pneumatic conveying equipment represents a significant advancement in material handling technology, offering efficient, safe, and cost-effective solutions for various industrial applications. The equipment's core principle of using air flow to transfer material from large bags into processing systems, combined with its adaptability and reliability, makes it a preferred choice for industries that require high-volume, continuous material handling. The working scene characteristics, including its ability to handle diverse materials, integrate with existing systems, and maintain operational efficiency, have contributed to its widespread adoption in sectors such as chemical, food, pharmaceutical, and mining. The technical advantages, including advanced control systems, energy efficiency, and durability, further enhance its performance and make it a long-term investment for industrial operations. As industries continue to demand more efficient and sustainable material handling solutions, the tonne bag unloading pneumatic conveying equipment from HeadPowder remains a vital component in modern manufacturing and processing. The company's commitment to innovation and quality ensures that its products continue to meet the evolving needs of the industry, providing reliable and effective solutions for years to come.




