For industrial applications involving the handling of precipitated barium sulfate, efficient and reliable material transport is crucial. The air-driven conveying system developed by Shandong HeadPowder Engineering Co., Ltd. offers a sophisticated solution tailored to meet these demands. This system is designed to handle the unique properties of precipitated barium sulfate, ensuring safe and effective material movement within processing facilities.
Company Overview
HeadPowder, as the company's brand, represents Shandong HeadPowder Engineering Co., Ltd., a leading provider of specialized engineering solutions in material handling. With a focus on innovation and precision, HeadPowder has established itself as a trusted partner in the industry, delivering high-quality equipment and systems that enhance operational efficiency and safety. The company is headquartered in Shandong, China, where it leverages its expertise to develop cutting-edge technologies for various industrial sectors.
Working Principle of the Air-Driven Conveying System
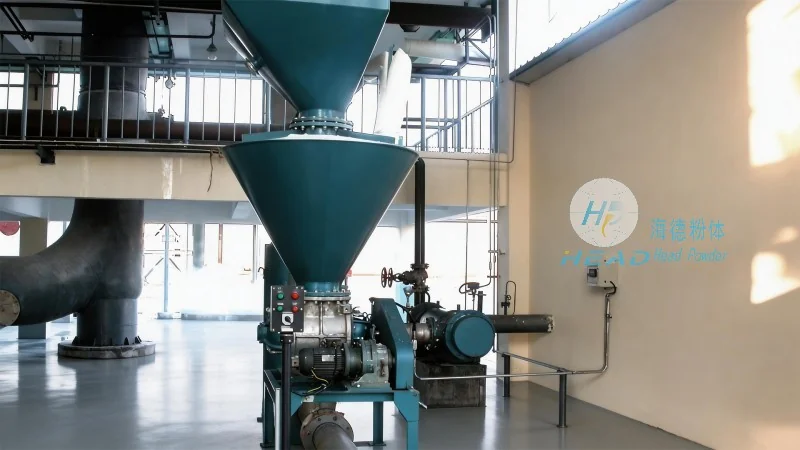
The air-driven conveying system for precipitated barium sulfate operates on the principle of pneumatic transport, utilizing compressed air to move material through a network of pipes. The system typically consists of a material loading hopper, an air compressor, and a series of conveying lines. When material is introduced into the hopper, it is drawn into the conveying line by the airflow generated by the compressor. The compressed air creates a low-pressure zone that pulls the material along the pipe, ensuring consistent and controlled transport. This method eliminates the need for mechanical components like belts or chains, reducing maintenance requirements and minimizing the risk of material contamination.
Key Features and Advantages
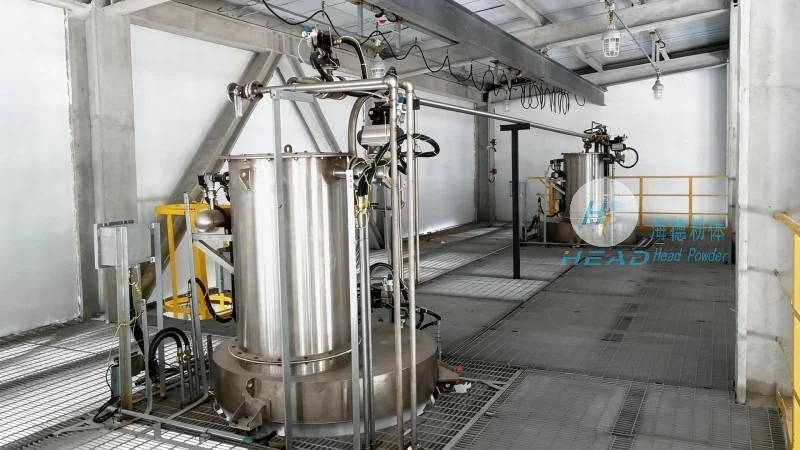
The air-driven conveying system for precipitated barium sulfate material offers several distinct features that set it apart from traditional conveying methods. Firstly, it provides a dust-free and enclosed transport environment, which is essential for handling fine powders like precipitated barium sulfate. This not only improves workplace safety by reducing airborne dust but also maintains the purity of the material, preventing contamination from external sources. Secondly, the system is highly flexible in terms of layout and can be adapted to various plant configurations, allowing for easy integration into existing processing lines. The modular design enables scalability, making it suitable for both small-scale and large-scale production facilities. Additionally, the system operates with minimal noise and vibration, contributing to a quieter and more stable working environment. Another significant advantage is its energy efficiency, as the pneumatic system can achieve high material throughput with lower energy consumption compared to other conveying methods. The system also ensures consistent material flow rates, which is critical for maintaining process stability and product quality.
Application and Performance
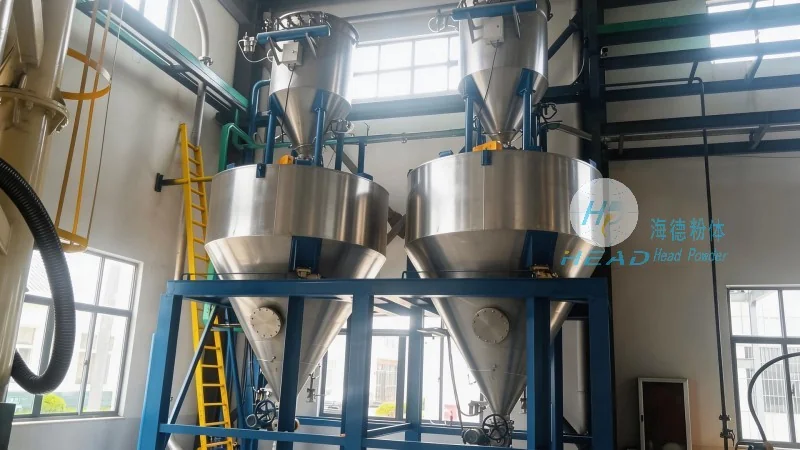
The air-driven conveying system is widely used in the chemical and pharmaceutical industries for the transport of precipitated barium sulfate, which is commonly used as a filler in coatings, plastics, and other industrial applications. The system's ability to handle fine powders without clogging or blockages makes it ideal for applications where material consistency is paramount. Performance-wise, the system can achieve high conveying capacities, with some models capable of transporting up to several tons of material per hour. The system's reliability is further enhanced by its self-cleaning capabilities, as the airflow helps to prevent material buildup in the pipes, reducing the need for frequent maintenance. Overall, the system provides a cost-effective and efficient solution for material handling, contributing to improved productivity and reduced operational costs for industrial facilities.
Conclusion
In conclusion, the air-driven conveying system for precipitated barium sulfate material developed by Shandong HeadPowder Engineering Co., Ltd. represents a significant advancement in material handling technology. By combining the principles of pneumatic transport with innovative design, the system offers a reliable, efficient, and safe solution for industrial applications. With its ability to handle fine powders, maintain material purity, and adapt to various plant layouts, the system is well-suited for a wide range of industrial sectors. HeadPowder's commitment to quality and innovation ensures that customers receive a product that meets their specific needs and contributes to the overall success of their operations.




