Pharmaceutical granule material handling equipment is a critical component in the pharmaceutical manufacturing workflow, responsible for the efficient and safe transport of granules from one processing stage to another. These systems are engineered to handle various types of pharmaceutical granules, including active pharmaceutical ingredients (APIs) and excipients, with precision and reliability. The proper operation of such equipment is essential for maintaining product quality, consistency, and compliance with regulatory standards, ensuring that pharmaceutical products meet the highest safety and efficacy requirements.
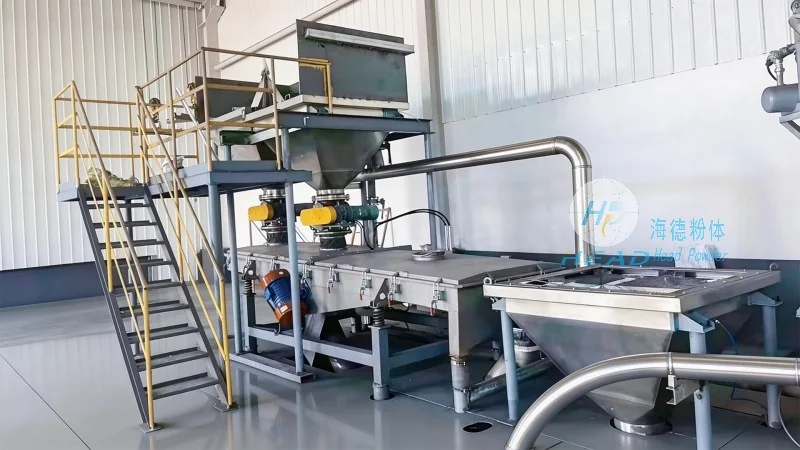
Working Principle of Pharmaceutical Granule Material Handling Equipment
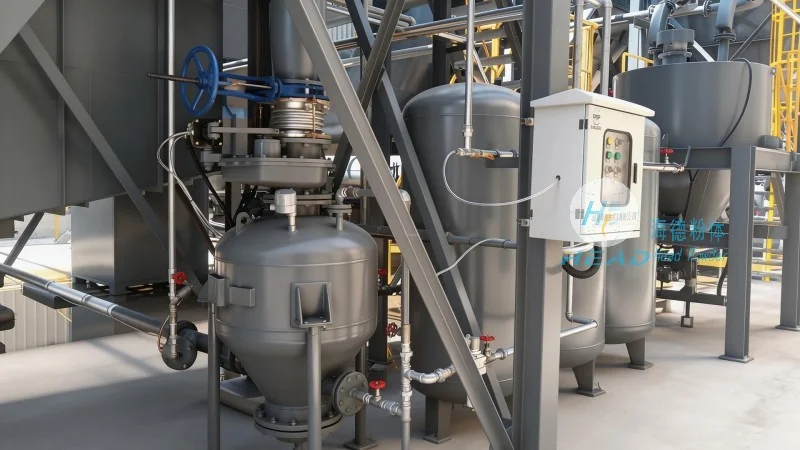
The working principle of pharmaceutical granule material handling equipment typically involves the integration of mechanical, pneumatic, or hybrid systems to move granules through pipelines, hoppers, and other containers. The core objective is to transport granules without degradation, contamination, or loss of quality. These systems often utilize gravity, air pressure, or mechanical forces to achieve material flow. For example, pneumatic conveying systems use compressed air to transport granules through a network of pipes, which is particularly effective for handling fine or dusty granules as it minimizes particle breakage and ensures a consistent flow. Mechanical screw or belt conveyors are used for bulkier granules, requiring less air pressure and suitable for larger production scales. The choice of technology depends on granule characteristics like size, density, moisture content, and the specific operational needs of the manufacturing process.
Modern pharmaceutical granule handling equipment incorporates advanced control mechanisms, including programmable logic controllers (PLCs) and sensors, to monitor and adjust material flow in real-time. This allows for precise control over speed and volume, preventing overloading or underloading of downstream equipment. The systems also feature material flow sensors and alarms to detect blockages or irregularities, ensuring operational safety and efficiency. Additionally, many units include cleaning and sanitization features, such as CIP (Clean-in-Place) systems, to maintain hygiene and prevent cross-contamination, which is paramount in pharmaceutical manufacturing.
Key Features of Pharmaceutical Granule Material Handling Equipment
Pharmaceutical granule material handling equipment is distinguished by several key features that enhance performance and usability. One of the most critical features is the use of stainless steel construction, which is non-reactive, easy to clean, and resistant to corrosion, ensuring product purity and compliance with regulatory standards. The equipment often operates within closed systems to minimize exposure to the environment and prevent contamination, with integrated dust collection and filtration systems to capture any airborne particles and protect both the product and operators.
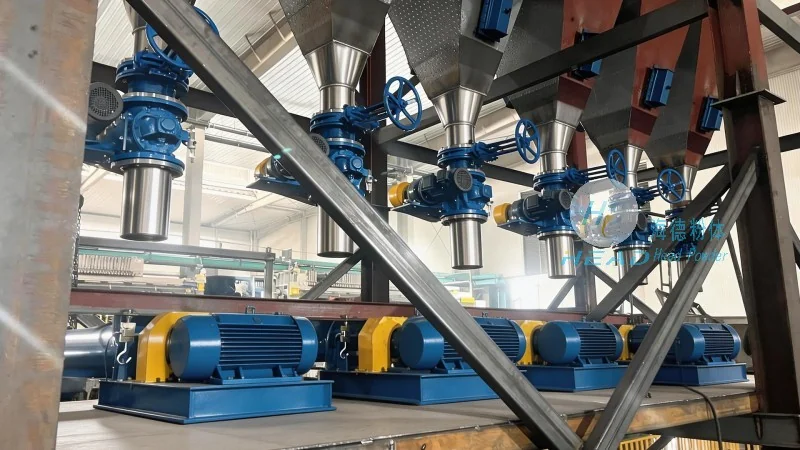
Another important feature is the emphasis on precision and control. Advanced control systems enable operators to adjust parameters such as flow rate, pressure, and speed with high accuracy, ensuring consistent material handling across different production batches. The equipment also includes safety features like emergency stop buttons and interlocks to prevent accidents and protect personnel. Reliability and efficiency are further enhanced through robust construction and durable components, designed to withstand the demands of continuous operation in a pharmaceutical manufacturing environment. Many systems also incorporate self-cleaning mechanisms and easy maintenance features, reducing downtime and maintenance efforts.
Customization and adaptability are also key aspects. Pharmaceutical manufacturers often require equipment tailored to their specific production needs, and modern granule handling systems offer modular designs that can be configured to handle different granule types and production volumes. This flexibility allows companies to scale their operations as needed without significant equipment changes. Additionally, the integration of data logging and reporting capabilities helps in process optimization and compliance with quality management systems (QMS), providing valuable insights into material handling performance.
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of pharmaceutical granule material handling equipment based in Shandong, China. The company has established a strong reputation in the pharmaceutical industry for providing high-quality, reliable equipment that meets the stringent requirements of modern manufacturing processes. HeadPowder specializes in the design, development, and supply of equipment tailored to the unique needs of pharmaceutical manufacturers, ensuring that their products enhance operational efficiency while maintaining product quality and safety.
HeadPowder’s commitment to innovation and customer satisfaction drives its continuous investment in research and development. The company’s engineering team works closely with clients to understand their specific challenges and provide customized solutions that address their unique material handling requirements. This collaborative approach ensures that the equipment delivered is not only efficient but also aligned with the client’s production goals and regulatory obligations.
HeadPowder’s manufacturing facilities are equipped with state-of-the-art technology and adhere to strict quality management standards, ensuring that every product meets the highest industry benchmarks. The company maintains a comprehensive quality control system, from raw material inspection to final product testing, to guarantee reliability and performance. Additionally, HeadPowder provides ongoing support and maintenance services to its clients, ensuring that the equipment operates at peak efficiency throughout its lifecycle. By choosing HeadPowder, pharmaceutical manufacturers can rely on a trusted partner that understands the critical role of material handling in their production processes, helping them achieve their production targets while upholding the highest standards of product quality and safety.




